 English
 中文简体
 русский
 Français
 Español
 عربى
 CONTACT US


Carbon Molecular Sieve for High-Efficiency PSA Nitrogen Generation
2026-10-07
Content
- 1 Introduction
- 2 What Is Carbon Molecular Sieve?
- 3 Principal Advantages of the CMS Product Range
- 4 CMS-240, CMS-260, CMS-280, and CMS-330 Performance Comparison
- 5 Advanced Manufacturing and Material-Control Strengths
- 6 Factory Testing and Quality Assurance
- 7 Required Air Pretreatment
- 8 Operating Conditions for Reliable Performance
- 9 Application Selection by Industry
- 10 Advantages Over Less Specialized Adsorbents
- 11 Installation, Storage, and Handling Recommendations
- 12 Maintenance and Service-Life Considerations
- 13 Choosing the Appropriate CMS Grade
- 14 Company Capabilities and Customer Support
- 15 Q&A
- 15.1 What is carbon molecular sieve used for?
- 15.2 What is the difference between CMS-240, CMS-260, CMS-280, and CMS-330?
- 15.3 Can CMS produce 99.999% nitrogen?
- 15.4 Why does nitrogen output decrease as purity increases?
- 15.5 What feed-air quality does CMS require?
- 15.6 What adsorption pressure is recommended?
- 15.7 How does temperature affect CMS performance?
- 15.8 How long does carbon molecular sieve last?
- 15.9 Why is factory testing in a nitrogen generator important?
- 15.10 How should customers select a CMS supplier?
- 16 Conclusion
- 17 References
- 18 Product: Carbon Molecular Sieve (CMS)
Introduction
Carbon molecular sieve, commonly abbreviated as CMS, is the core adsorbent used in many pressure swing adsorption nitrogen generators. Its primary function is to separate oxygen from nitrogen in compressed air by exploiting differences in molecular diffusion and adsorption behavior. When properly designed and operated, a CMS-filled adsorption tower allows oxygen, moisture, carbon dioxide, and other faster-diffusing components to be preferentially retained, while nitrogen passes through as the product gas.
The performance of a nitrogen generator depends on far more than the name of the adsorbent. Pore-size distribution, mechanical strength, adsorption selectivity, working capacity, regeneration behavior, particle uniformity, dust generation, filling density, pretreatment quality, pressure, temperature, cycle timing, and equipment design all influence the final result. A high-quality carbon molecular sieve must therefore provide a balanced combination of separation efficiency, durability, stable production, and cost control.
CMS-240, CMS-260, CMS-280, and CMS-330 are carbon molecular sieve grades developed for PSA nitrogen-generation applications. The grades are designed to cover a wide range of nitrogen purity and production requirements, from general industrial blanketing and fire prevention to applications requiring very high nitrogen purity. According to the supplied performance data, the grades can produce nitrogen purities from 99% to 99.999%, with different gas-production rates and air-to-nitrogen ratios.
Anhui Zhuoxu New Material Technology Co., Ltd. supplies these CMS products as a manufacturer and industrial materials company. Its production capabilities are supported by an integrated porous-carbon materials chain, continuous manufacturing equipment, product testing through nitrogen generators, cooperation with research institutions, and ISO 9001 quality-management certification. These capabilities are intended to provide customers with consistent material quality rather than simply a low-cost carbon adsorbent.
This article explains how carbon molecular sieves work, compares the CMS-240, CMS-260, CMS-280, and CMS-330 grades, reviews their manufacturing advantages, and discusses the operating conditions required to obtain reliable performance in a PSA nitrogen generator.
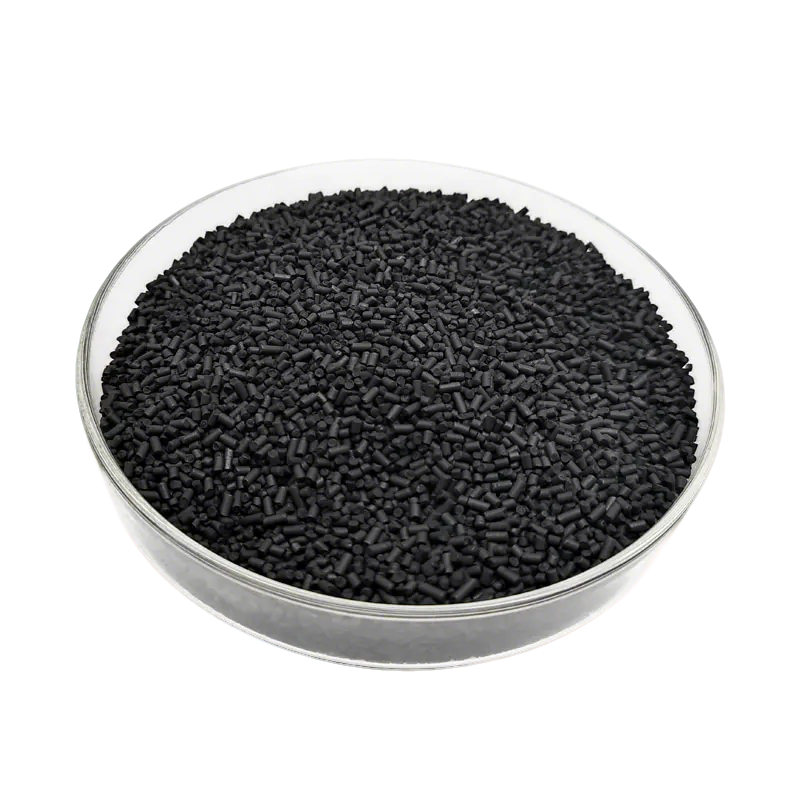
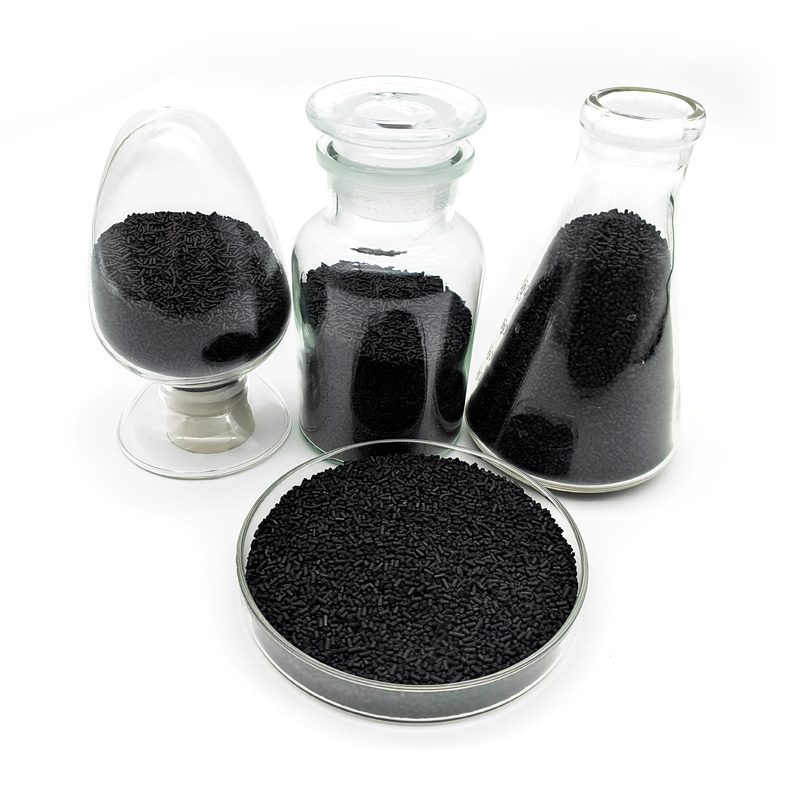
Carbon Molecular Sieve (CMS)
What Is Carbon Molecular Sieve?
Carbon molecular sieve is a porous carbon adsorbent engineered to separate gas molecules according to their adsorption affinity and diffusion rate. Although the material is carbon-based, it is not simply ordinary activated carbon. Its micropore structure is carefully controlled so that gases with similar molecular sizes can be separated under practical pressure and temperature conditions.
In air separation, the most important distinction is between oxygen and nitrogen. Oxygen molecules diffuse into the effective micropores of CMS more readily than nitrogen molecules. Under pressurized conditions, oxygen is therefore adsorbed preferentially. Nitrogen, which has a lower adsorption preference and a slower diffusion rate into the critical pores, can pass through the adsorption bed and be collected as product gas.
The pore-size range identified for the supplied carbon molecular sieve products is approximately 0.28 to 0.38 nanometers. This range is especially important for oxygen-nitrogen separation. If the pores are too large, nitrogen adsorption may increase and the separation selectivity may decline. If the pores are too small, oxygen diffusion may become excessively slow, reducing productivity. The objective is not simply to maximize surface area, but to create an appropriate pore structure for the intended PSA cycle.
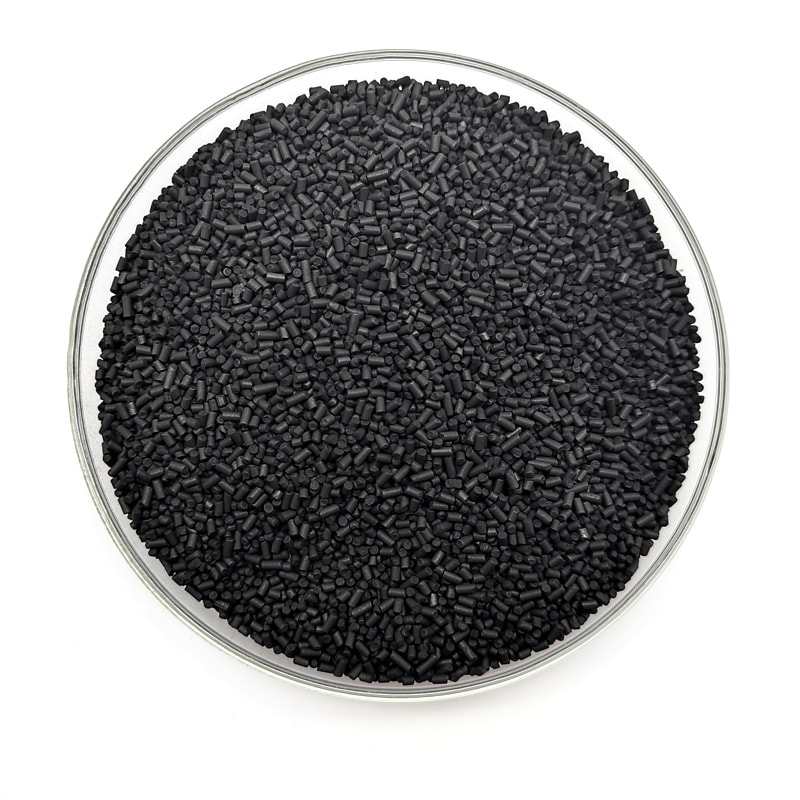
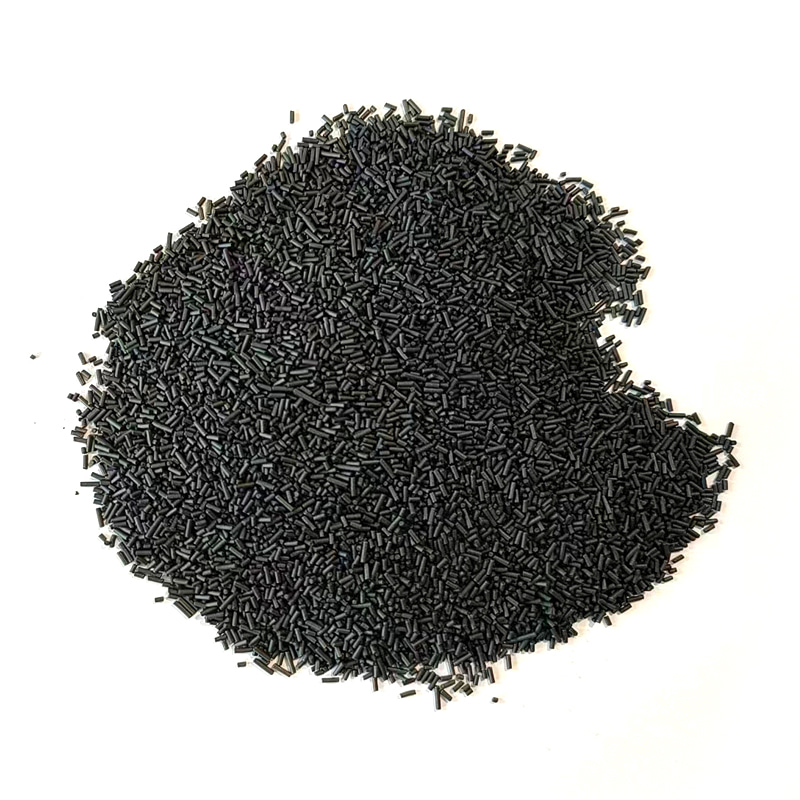
Carbon molecular sieve is generally supplied in granular or pelletized form. The particles must have enough mechanical strength to withstand filling, transportation, repeated pressurization, depressurization, and pressure equalization. Excessive particle breakage produces fines. Fines can increase pressure drop, interfere with valve operation, block filters, and reduce effective mass transfer in the adsorption bed.
For this reason, the best CMS product is one that combines selective microporosity with suitable particle strength and dimensional stability. A material with high adsorption capacity but poor mechanical stability may not deliver the best total operating result. Similarly, a very strong material with an unsuitable pore structure may fail to achieve the required nitrogen purity or capacity.
Selective Adsorption and Molecular Diffusion
The operating principle of CMS is based on a combination of adsorption equilibrium and molecular kinetics. Adsorption equilibrium describes how much of a gas component can be held by the carbon surface at a given pressure and temperature. Molecular kinetics describe how quickly that component can enter and move through the pore network.
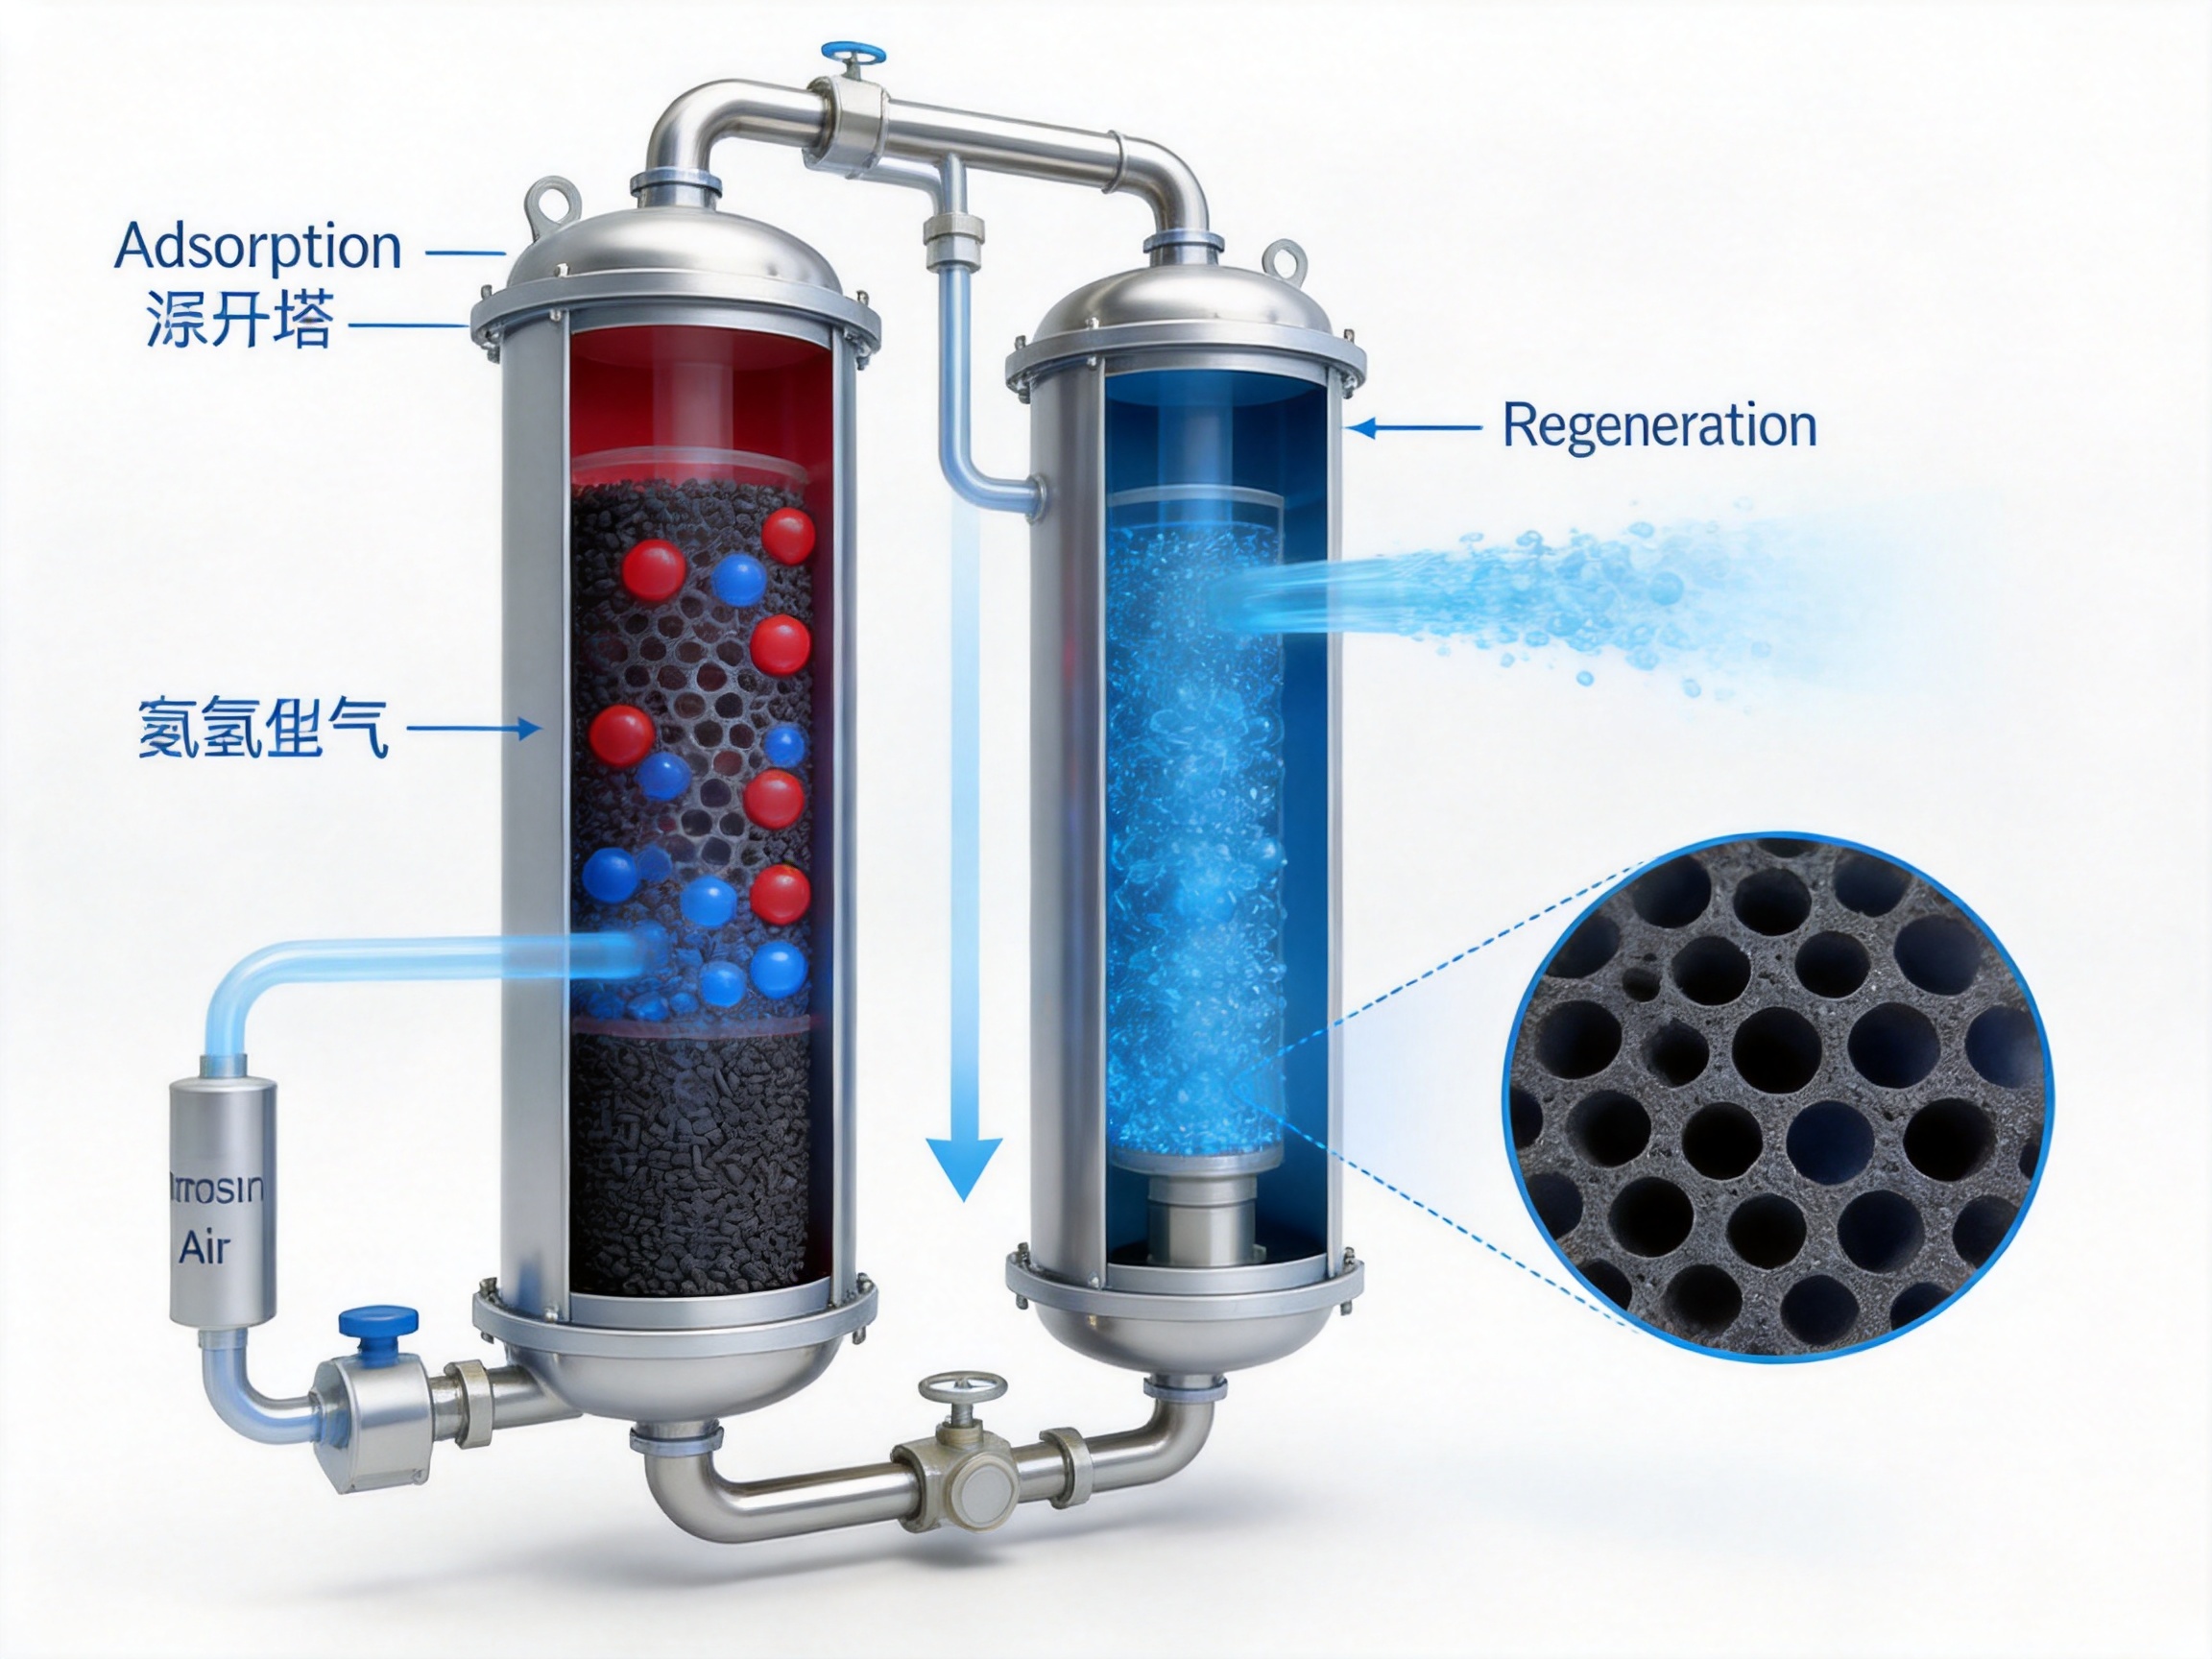
During the adsorption step, compressed air enters a CMS tower. Oxygen and other rapidly adsorbed components move into the micropores and are retained. Nitrogen travels through the bed and leaves as the product stream. During regeneration, the pressure is reduced and the retained gases are released. A portion of the nitrogen product may be used as purge gas to improve desorption and prepare the bed for the next adsorption step.
The actual separation is dynamic. The adsorbent is not expected to retain oxygen indefinitely. Instead, the PSA cycle repeatedly loads and regenerates the CMS. The adsorption time must be long enough to achieve the desired nitrogen recovery but short enough to avoid breakthrough of oxygen into the product stream.
Cycle design is therefore closely connected with CMS quality. A material with favorable mass-transfer kinetics can support shorter cycles and higher productivity. A material with stable pore structure can maintain performance through many adsorption-regeneration cycles. A material with low dust formation can help preserve bed permeability and equipment reliability.
Principal Advantages of the CMS Product Range
Efficient Oxygen-Nitrogen Separation
The primary advantage of the CMS range is its suitability for selective oxygen-nitrogen separation. The controlled micropores allow oxygen to diffuse more rapidly than nitrogen, making the material appropriate for PSA nitrogen generators. This enables nitrogen production without cryogenic air separation or membrane modules.
For many industrial users, PSA technology offers an effective balance between investment, operating cost, flexibility, and production speed. Nitrogen can be generated at the point of use, reducing reliance on delivered cylinders or liquid nitrogen. The required purity can also be adjusted according to the process instead of producing a fixed, unnecessarily high purity.
Strong Adsorption Capacity
Carbon molecular sieves can retain meaningful quantities of gas even when the concentration of a component is relatively low. This characteristic supports efficient removal of oxygen from air during the adsorption stage. The supplied product information also indicates that the CMS retains substantial adsorption capacity at elevated temperatures compared with many other adsorbent options under similar conditions.
In practical terms, strong working capacity can help reduce the amount of adsorbent required for a specified nitrogen output, or it can allow an existing generator to produce more nitrogen when the equipment and cycle are appropriately matched. Actual results depend on pressure, temperature, pretreatment, cycle configuration, product purity, and the design of the nitrogen generator.
Flexible Nitrogen Purity and Production
A PSA nitrogen generator does not necessarily need to operate at its maximum purity. Nitrogen production generally increases when the required purity is reduced, while the air consumption ratio may also improve. Conversely, producing very high-purity nitrogen normally requires more adsorbent, a longer or more carefully controlled cycle, greater air consumption, or reduced product flow.
The CMS grades are intended to support this operating flexibility. A user may select a target purity ranging from approximately 99% to 99.999%, depending on the application. The correct selection should be based on actual process requirements rather than automatically choosing the highest purity. Producing nitrogen at a higher purity than necessary can increase energy consumption and reduce overall system efficiency.
Cost-Effective PSA Operation
Compared with cryogenic nitrogen production, PSA systems can be installed at a smaller scale and started or stopped more easily. Compared with delivered nitrogen, an on-site system can reduce logistics requirements and provide a continuous supply. Carbon molecular sieve is central to this economic model because its performance directly affects air consumption, electricity use, product flow, and replacement intervals.
A cost-effective CMS product is not defined only by its purchase price per kilogram. The more important calculation includes nitrogen output, nitrogen purity, air-to-nitrogen ratio, power consumption, expected service life, dust generation, maintenance requirements, and the cost of replacing or refilling the adsorbent bed.
The supplied CMS data show that different product grades provide different combinations of purity, production rate, and air consumption. This allows the customer to choose a material according to the total operating cost of the nitrogen generator rather than selecting an adsorbent based on price alone.
Broad Industrial Application
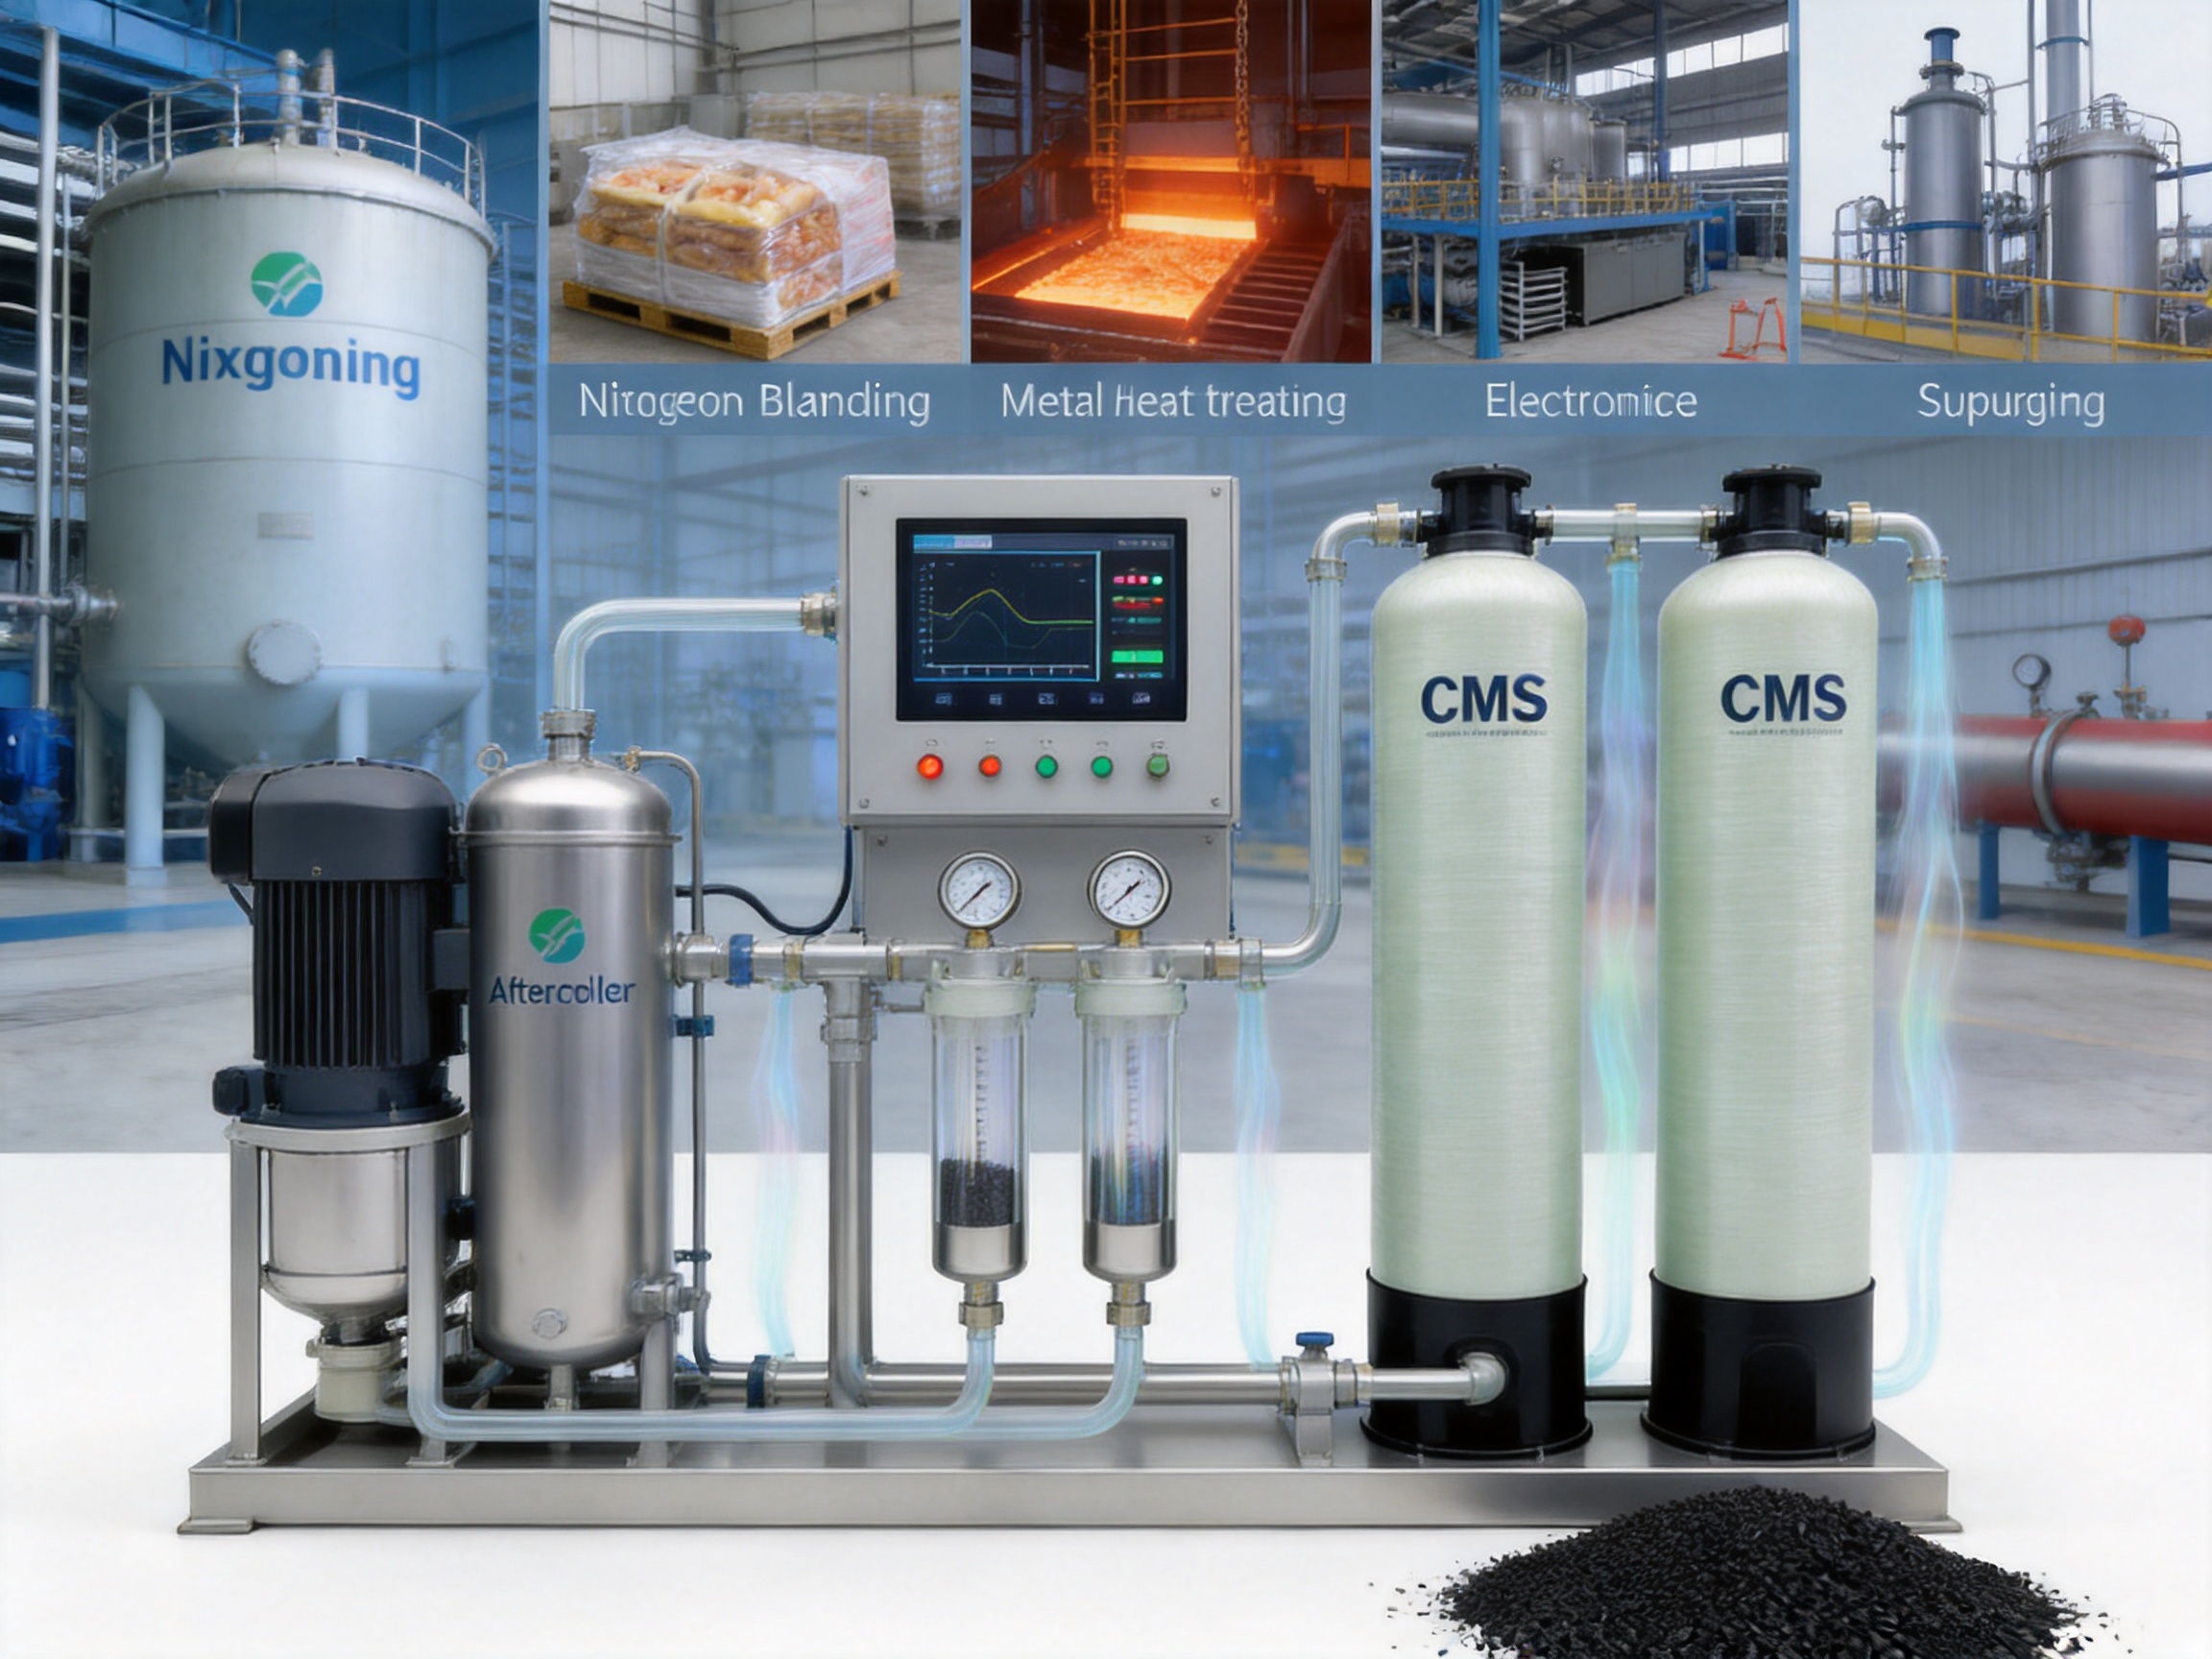
CMS-based nitrogen generation is used in chemical processing, oil and gas, electronics, food packaging, coal mining, pharmaceuticals, cable production, metal heat treatment, transportation, and storage. Nitrogen may be used for inerting, purging, blanketing, oxidation prevention, fire and explosion risk reduction, product preservation, or process control.
In the food industry, nitrogen can help displace oxygen in packaging and storage environments. In metal heat treatment, nitrogen can provide a controlled atmosphere that reduces unwanted oxidation. In chemical and petrochemical operations, nitrogen can be used for tank blanketing, pipeline purging, and equipment maintenance. In electronics manufacturing, higher-purity nitrogen can support controlled production environments.
The material grade and generator design must always be selected for the specific application. Food, pharmaceutical, and electronics users may have additional requirements concerning oil carryover, moisture, particulate contamination, gas purity verification, and system validation.
CMS-240, CMS-260, CMS-280, and CMS-330 Performance Comparison
The four grades are positioned for different production and purity targets. The figures below are the supplied reference values at an adsorption pressure of approximately 0.75–0.80 MPa. The nitrogen production-rate unit is reproduced as cubic meters per hour per tonne of CMS, based on the supplied specification format. Because actual output depends on generator design and operating conditions, users should confirm the final basis with the manufacturer before equipment selection.
| CMS Grade | Adsorption Pressure | Nitrogen Purity | Reported Nitrogen Production Rate | Air-to-Nitrogen Ratio |
|---|---|---|---|---|
| CMS-240 | 0.75–0.80 MPa | 99.999% | 70 | 6.5 |
| CMS-240 | 0.75–0.80 MPa | 99.99% | 110 | 4.6 |
| CMS-240 | 0.75–0.80 MPa | 99.9% | 165 | 3.6 |
| CMS-240 | 0.75–0.80 MPa | 99.5% | 240 | 2.6 |
| CMS-240 | 0.75–0.80 MPa | 99% | 290 | 2.3 |
| CMS-260 | 0.75–0.80 MPa | 99.999% | 80 | 6.4 |
| CMS-260 | 0.75–0.80 MPa | 99.99% | 120 | 4.5 |
| CMS-260 | 0.75–0.80 MPa | 99.9% | 175 | 3.5 |
| CMS-260 | 0.75–0.80 MPa | 99.5% | 260 | 2.5 |
| CMS-260 | 0.75–0.80 MPa | 99% | 305 | 2.2 |
| CMS-280 | 0.75–0.80 MPa | 99.999% | 90 | 6.2 |
| CMS-280 | 0.75–0.80 MPa | 99.99% | 135 | 4.2 |
| CMS-280 | 0.75–0.80 MPa | 99.9% | 195 | 3.3 |
| CMS-280 | 0.75–0.80 MPa | 99.5% | 280 | 2.3 |
| CMS-280 | 0.75–0.80 MPa | 99% | 335 | 1.9 |
| CMS-330 | 0.75–0.80 MPa | 99.999% | 100 | 6.2 |
| CMS-330 | 0.75–0.80 MPa | 99.99% | 170 | 4.0 |
| CMS-330 | 0.75–0.80 MPa | 99.9% | 250 | 3.3 |
| CMS-330 | 0.75–0.80 MPa | 99.5% | 330 | 2.3 |
| CMS-330 | 0.75–0.80 MPa | 99% | 360 | 1.9 |
How to Interpret the Data
The table demonstrates a common PSA relationship: as nitrogen purity increases, the available nitrogen production rate generally decreases and the air-to-nitrogen ratio increases. For example, CMS-330 is listed at 360 units for 99% nitrogen, but at 100 units for 99.999% nitrogen. This does not mean that the higher-purity operating point is less useful. It means that achieving a very low residual oxygen concentration requires a greater separation duty.
CMS-240 is suitable for systems where a moderate production requirement and a range of purity options are needed. CMS-260 provides a higher reported production rate than CMS-240 at each listed purity level. CMS-280 provides a further increase in the supplied reference values and is presented as one of the company’s principal high-quality grades. CMS-330 shows the highest reported rates across the listed purity levels and is intended for demanding production requirements when the generator is properly designed for the material.
Performance comparisons should not be made solely from a single number. A higher nominal flow rate may require a different bed volume, cycle time, feed-air quality, or pressure profile. The correct comparison is the total amount of usable nitrogen produced per unit of compressed-air energy while meeting the required purity and stability targets.
Advanced Manufacturing and Material-Control Strengths
Integrated Porous-Carbon Supply Chain
An important strength of the manufacturer is its connection with a broader porous-carbon materials operation. The supplied company information states that the production base has an annual capacity of approximately 4,000 tons of porous carbon materials and 30,000 cubic meters of floral foam. A second-phase porous-carbon project with a planned capacity of approximately 3,000 tons is scheduled to begin operation in 2026 and is intended to support applications including silicon-carbon anode materials and PSA pressure swing adsorption.
An integrated materials chain can provide greater control over raw-material quality, production scheduling, formulation development, and cost. It can also reduce dependence on multiple intermediaries. In carbon molecular sieve manufacturing, raw-material consistency is particularly important because changes in precursor composition can influence carbonization behavior, pore development, surface chemistry, mechanical strength, and final adsorption performance.
Controlled Raw-Material Selection
The supplied material describes the use of dedicated raw materials and cooperation with upstream suppliers to maintain stable and uniform input quality. This approach is valuable because CMS production is sensitive to variations in precursor chemistry and processing conditions.
Consistent raw materials help reduce batch-to-batch differences. They can support more predictable carbonization, activation, pore adjustment, shaping, and heat treatment. For customers operating multiple nitrogen generators, consistency is important because a change in adsorbent behavior can alter oxygen breakthrough time, product purity, pressure drop, and compressor loading.
Specialized Carbon-Based Formulation
The product information refers to a proprietary carbon molecular sieve base material and a specialized material formulation developed for carbon molecular sieve production. The purpose of such a formulation is to improve the conversion efficiency of carbon material into finished adsorbent while supporting the required pore structure and physical strength.
The company also describes its broader Resin-Based Porous Carbon, or RHC, technology. This technology uses polymer resin as a precursor and forms a stable hard-carbon structure through high-temperature carbonization. Although different product applications may require different formulations and processing conditions, resin-based precursor technology can provide a controllable route for engineering carbon structure and pore characteristics.
For CMS, the key advantage of a controlled precursor route is the ability to adjust the material toward the intended gas-separation duty. The production objective is not to create a general-purpose activated carbon. It is to create a carbon adsorbent with a pore system and particle structure appropriate for PSA nitrogen generation.
Continuous Production Equipment
The company reports the use of continuous production equipment. Continuous processing can reduce direct labor requirements and limit variation caused by frequent manual intervention. It may also improve temperature control, material residence-time consistency, process repeatability, and production efficiency.
Automation and continuous handling are especially useful for a product that must maintain consistent particle properties. Manual operations can introduce variation in mixing, forming, drying, loading, unloading, and heat treatment. Reducing these influences can support more uniform finished material and help lower the amount of off-specification product.
Continuous equipment is not a substitute for process control. It must be supported by appropriate monitoring, calibration, sampling, and quality checks. When these elements are combined, continuous production can become an important advantage over small-scale or highly manual manufacturing operations.
Location and Environmental Conditions
The company indicates that its production location has relatively low atmospheric humidity compared with more humid regions. Moisture control is relevant to carbon molecular sieve manufacturing and storage. Excessive humidity can affect drying requirements, packaging, handling, and the water content of the finished adsorbent.
Moisture is also important during customer operation. CMS should be protected from water vapor because water can occupy adsorption sites, alter gas-transfer behavior, increase the load on the regeneration step, and reduce separation performance. The dry production environment is therefore one part of a broader moisture-management strategy that must continue through packaging, transport, storage, and nitrogen-generator filling.
Research and Development Cooperation
The manufacturer reports cooperation with Jinan Shengquan Group and China University of Mining and Technology in research and development related to carbon molecular sieves and carbon materials. Cooperation with industrial and academic partners can support material characterization, process optimization, scale-up, and application testing.
Research for CMS should include more than static adsorption measurements. Important areas include pore-size distribution, oxygen and nitrogen adsorption kinetics, dynamic breakthrough behavior, pellet strength, abrasion resistance, bulk density, pressure drop, thermal stability, regeneration response, and long-term cycling in an actual PSA generator.
The company states that it owns 21 core patents and holds ISO 9001 certification. Patents may support proprietary process and formulation development, while ISO 9001 provides a structured framework for document control, process management, corrective action, and continual improvement. Neither factor alone guarantees performance, but together they indicate an organized approach to product development and quality management.
Factory Testing and Quality Assurance
Testing in an Actual Nitrogen Generator
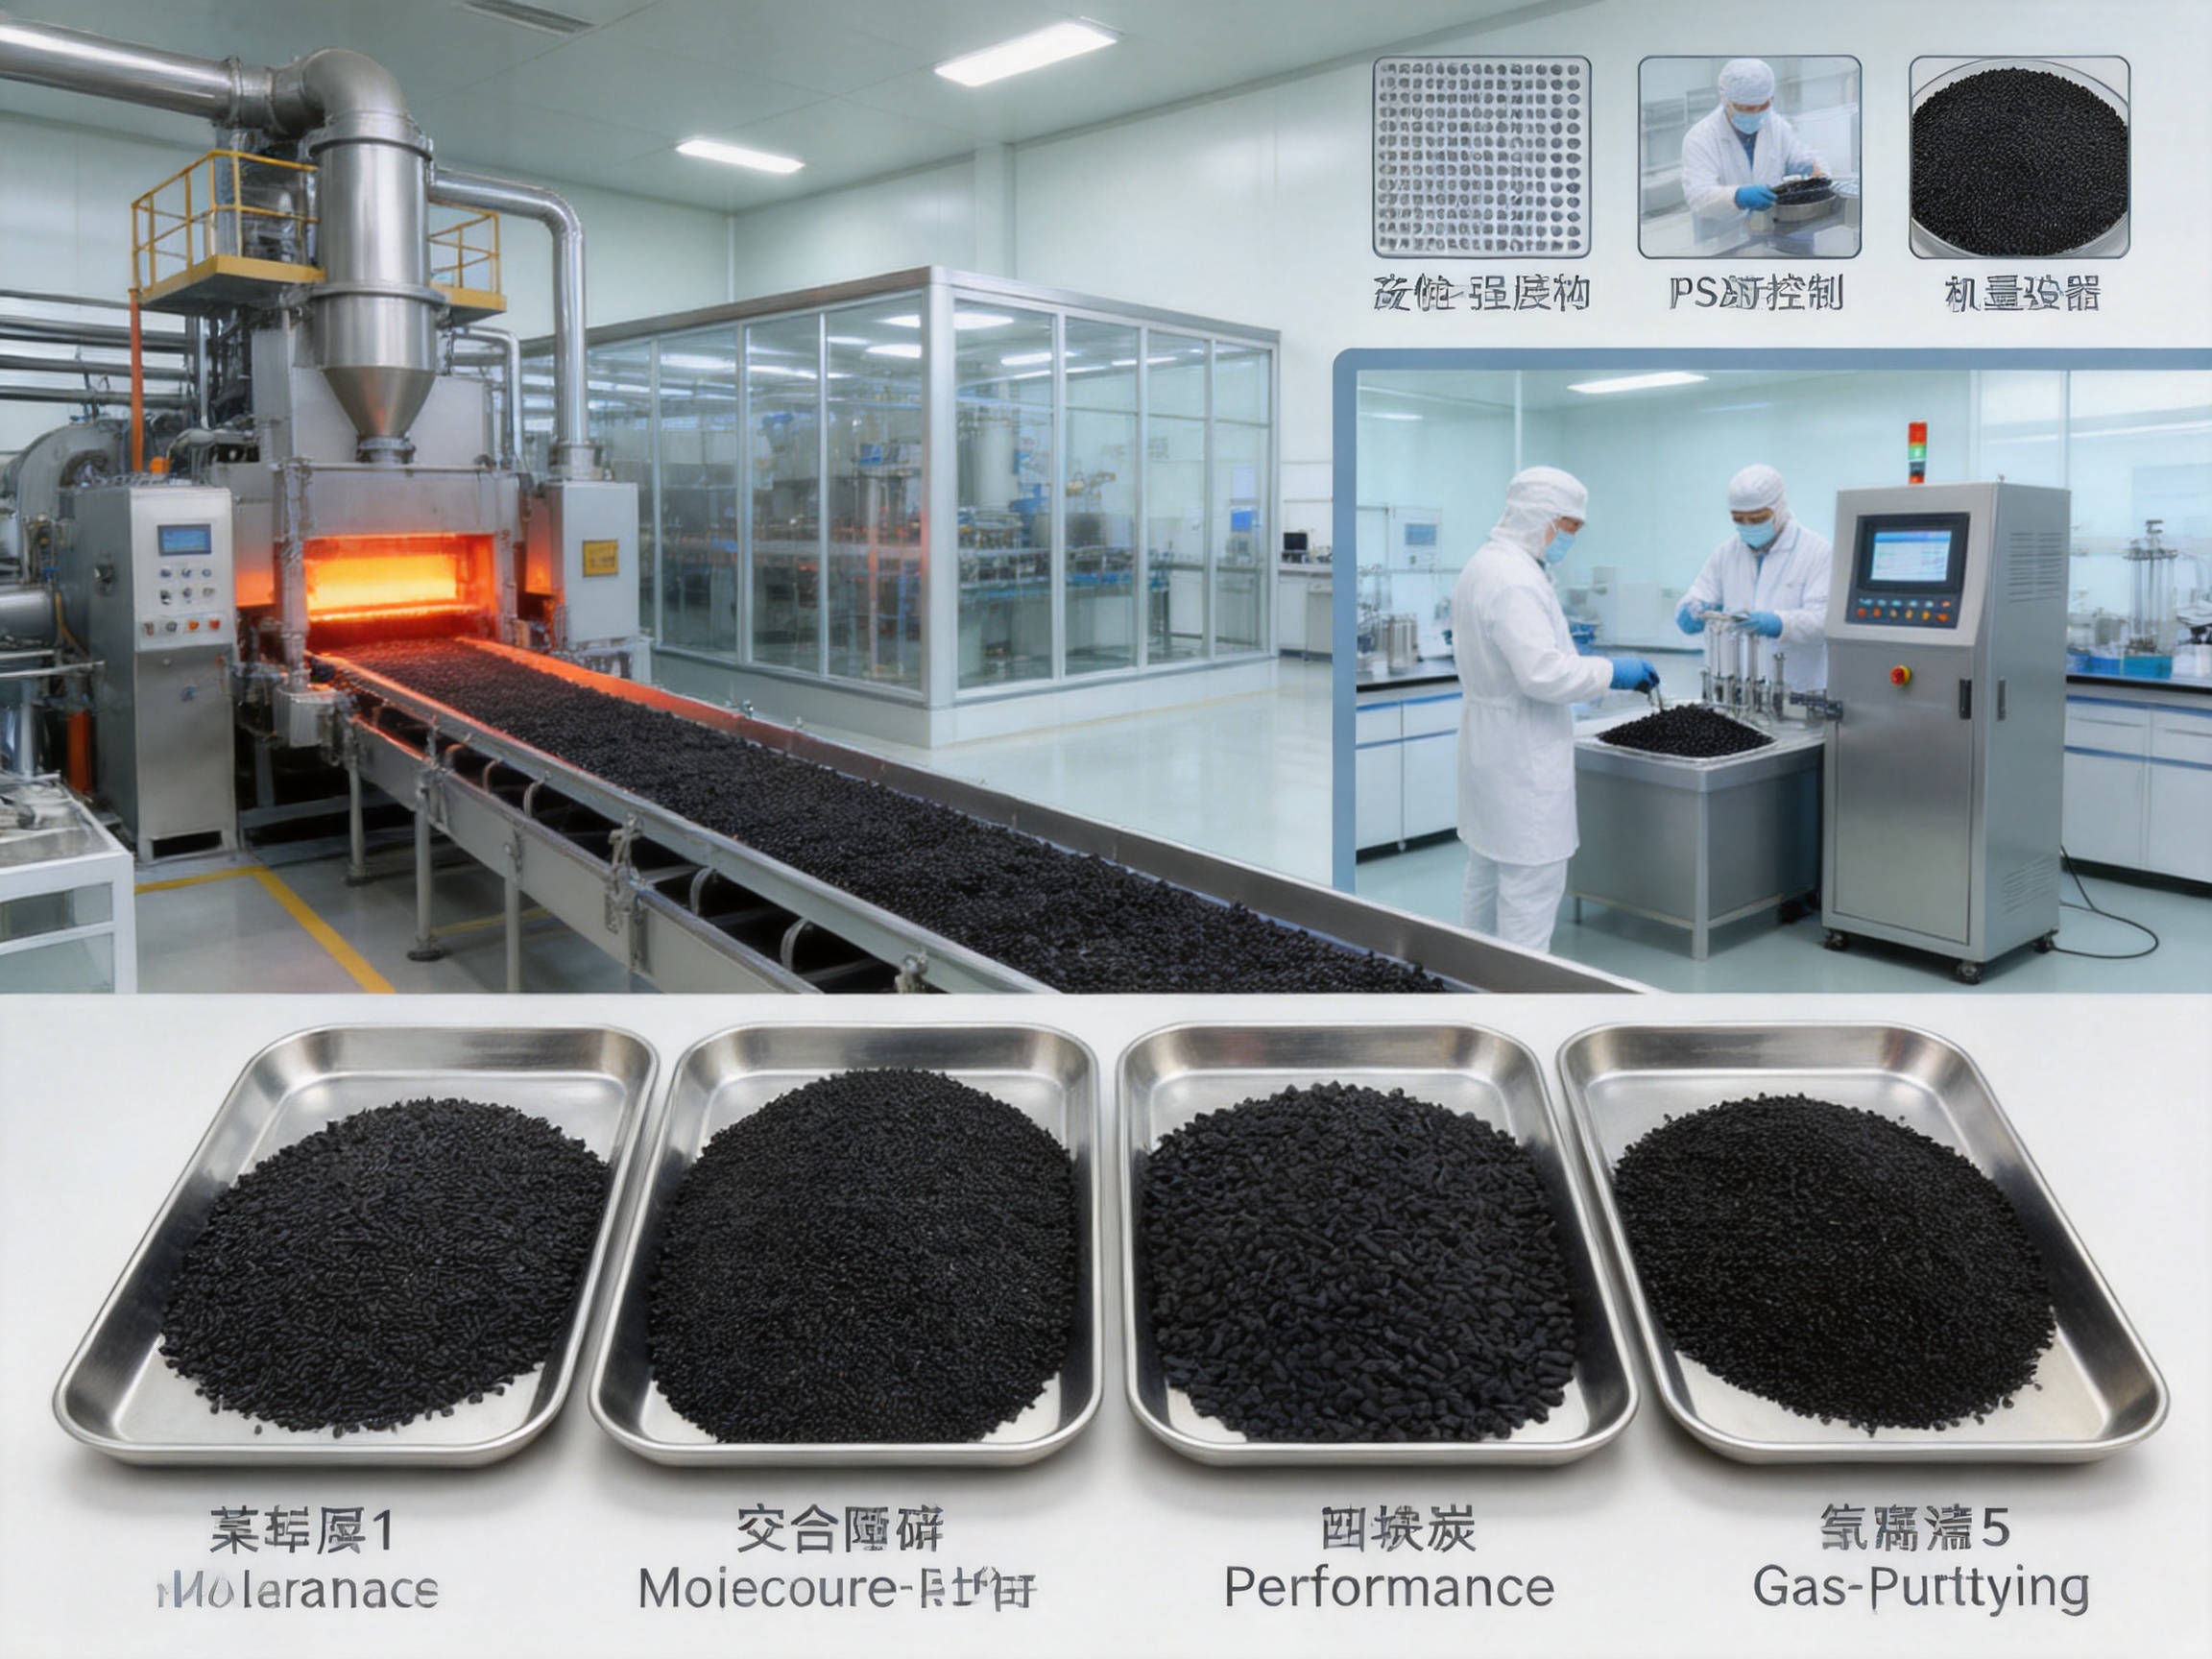
One of the most significant product-control measures described in the supplied information is the requirement that the CMS be tested in a nitrogen generator before shipment. The material must pass the application test before leaving the factory.
This approach is valuable because laboratory adsorption results do not always predict full PSA performance. A CMS may show favorable equilibrium data but produce unsatisfactory results if its mass-transfer rate, pellet strength, dust level, or pressure-drop behavior is unsuitable for the intended cycle. Testing in a working nitrogen generator allows the manufacturer to evaluate the interaction between the adsorbent and the actual process.
Application testing can examine nitrogen purity, output stability, air consumption, pressure drop, regeneration behavior, oxygen breakthrough, and cycle response. It can also reveal problems related to particle size distribution, filling density, valve timing, and bed loading. Such testing provides a stronger basis for release than appearance or basic moisture inspection alone.
High Proportion of Higher-Grade Material
The company states that approximately 90% of its CMS production reaches CMS-280 grade or above. This indicates a production objective focused on higher-performance material rather than a product range dominated by lower-grade output. The claim should be evaluated by customers through technical documentation, sample testing, and application trials, but it demonstrates the manufacturer’s emphasis on production consistency and grade quality.
Higher-grade CMS products are generally intended to provide improved output or lower air consumption under comparable conditions. However, customers should select the grade that matches their equipment. A high-performance adsorbent cannot compensate for inadequate pretreatment, incorrect cycle settings, undersized compressors, leaking valves, or poor tower design.
Recommended Quality Documentation
For industrial purchasing, customers should request a certificate of analysis or batch test report. Useful information may include adsorption performance, moisture content, ash content, bulk density, particle-size distribution, crushing strength, abrasion or attrition level, and relevant dynamic PSA test results.
The customer should also clarify the test conditions used for reported data. Pressure, temperature, cycle time, feed-air composition, nitrogen recovery, product purity measurement method, and output basis can all affect the result. Comparing two materials is meaningful only when the test conditions are sufficiently similar.
Required Air Pretreatment
Air pretreatment is essential for protecting CMS and maintaining stable nitrogen production. Compressed air from an oil-lubricated compressor may contain oil vapor, liquid oil, water, aerosols, and other contaminants. If these substances enter the CMS bed, they can block micropores and reduce the available adsorption surface.
The supplied operating guidance identifies a feed-air dew point below approximately minus 40 degrees Celsius and an oil content below approximately 0.3 parts per million. The source material contains formatting irregularities in this specification, so users should confirm the exact required values with the manufacturer and the nitrogen-generator supplier before commissioning. In general, the objective is clear: the air must be clean, dry, and substantially free of oil vapor and organic contaminants.
Typical Pretreatment Components
A PSA nitrogen system commonly includes an aftercooler, moisture separator, coalescing filters, oil-removal filtration, a refrigerated or desiccant dryer, and fine filtration before the CMS towers. The exact arrangement depends on compressor type, ambient conditions, required nitrogen purity, and system design.
The aftercooler reduces compressed-air temperature and condenses part of the water vapor. A moisture separator removes liquid condensate. Coalescing filters capture liquid aerosols and fine particles. Oil-removal filters or activated-carbon filters reduce residual oil vapor. A dryer lowers the dew point and helps protect the adsorbent from water contamination.
Filters must be maintained according to pressure drop and service life. A saturated or damaged filter may allow contaminants to pass into the CMS bed. Automatic drains should also be checked because accumulated condensate can enter downstream equipment if drainage fails.
Why Oil Contamination Is Serious
Oil contamination can be particularly damaging because oil may coat the internal pore surfaces and is difficult to remove during ordinary PSA regeneration. Once the micropores are blocked, oxygen diffusion and adsorption capacity can decline. The result may be lower nitrogen purity, reduced output, higher air consumption, or shortened adsorbent service life.
Where practical, oil-free compressors can reduce contamination risk. If an oil-lubricated compressor is used, the filtration and monitoring system must be properly designed. The use of high-quality CMS does not eliminate the need for suitable compressed-air treatment.
Operating Conditions for Reliable Performance
Adsorption Pressure
The supplied reference data use an adsorption pressure of approximately 0.75–0.80 MPa. In a general atmospheric-pressure regeneration process, the recommended operating pressure is identified as approximately 0.6–0.8 MPa. Higher pressure can increase adsorption capacity, but it also increases compressor energy consumption and places greater demands on vessels, valves, piping, and safety systems.
The best operating pressure is therefore a compromise between adsorption performance and total energy consumption. A system should not be operated at a higher pressure simply because the adsorbent can tolerate it. The pressure should be selected according to the required purity, output, nitrogen recovery, compressor efficiency, and equipment rating.
Operating Temperature
Adsorption is generally exothermic. As adsorption proceeds, heat is released and the temperature of the bed can rise. Higher temperature tends to reduce adsorption capacity, which may make it more difficult to maintain nitrogen purity at a given product flow.
The supplied material recommends an ambient temperature at or below approximately 15 degrees Celsius for optimal nitrogen-generator performance. Actual equipment may operate over a wider range, but lower and stable feed-air temperature is generally beneficial. The compressor aftercooler and cooling system should be sized to control the temperature entering the pretreatment train and adsorption towers.
Seasonal changes should be considered during system design. A nitrogen generator that performs well in a cool season may experience reduced output or increased air consumption during hot weather. Temperature compensation, conservative sizing, and appropriate control logic can help maintain stable performance.
Pressure Equalization
Pressure equalization transfers gas from a completed adsorption tower to another tower that is being regenerated or repressurized. The supplied information describes equalization from both the top and bottom directions and identifies a typical equalization time of approximately one to three seconds.
Proper equalization can recover gas energy, reduce nitrogen losses, improve recovery, and decrease the pressure shock experienced by the adsorbent bed. If the equalization step is too short, the potential energy benefit may not be fully obtained. If it is too long, the overall cycle may become inefficient or reduce the time available for productive adsorption.
Pressure equalization also helps reduce mechanical stress. Abrupt pressure changes can contribute to pellet movement, attrition, and dust generation. Correct valve sequencing and gradual pressure control are therefore important for maintaining bed integrity.
Cycle Timing
Cycle time determines how deeply the CMS bed is loaded before regeneration. The adsorption period must be controlled to avoid oxygen breakthrough. The regeneration period must be sufficient to remove the adsorbed gases and restore working capacity.
The ideal cycle depends on bed length, particle size, feed pressure, temperature, product purity, nitrogen flow, purge ratio, and CMS characteristics. A longer adsorption time may increase output per cycle but can allow the mass-transfer front to move too far through the bed. A shorter cycle may improve purity but reduce productivity and increase valve activity.
Customers should avoid changing cycle parameters without evaluating the effect on purity, recovery, compressor load, and adsorbent life. Any adjustment should be made gradually and verified with reliable oxygen analyzers and flow measurements.
Application Selection by Industry
Chemical and Petrochemical Processing
Chemical plants use nitrogen to displace oxygen from tanks, reactors, pipelines, and process equipment. Nitrogen blanketing can help reduce oxidation and limit the formation of flammable mixtures. PSA-generated nitrogen is attractive where demand is continuous and purity requirements are moderate to high.
For these applications, system reliability and flow stability may be more important than achieving the absolute maximum purity. The CMS grade should be selected according to tank volume, purge frequency, peak demand, and required oxygen concentration.
Oil and Gas Operations
Oil and gas facilities may use nitrogen for pipeline purging, vessel inerting, well-service operations, and maintenance activities. The required flow can vary significantly, so a buffer tank and appropriate control system may be necessary. The CMS generator should be protected from hydrocarbon vapors and other contaminants that could damage the adsorbent or create a safety hazard.
Food Packaging and Storage
Nitrogen can replace oxygen in food packages and storage environments to help slow oxidation and preserve product quality. The required purity depends on the product and packaging process. Stable flow, sanitary equipment design, oil-free air treatment, and dependable oxygen monitoring are essential.
Food applications may require additional documentation and materials compliance beyond the basic performance specification. The CMS itself is located upstream of the product gas, but the complete gas-generation system must be designed to prevent contamination.
Electronics and Semiconductor-Related Manufacturing
Electronics manufacturing can require nitrogen with low oxygen and moisture levels. Higher-purity operating points may therefore be appropriate, including the 99.99% and 99.999% ranges listed for the CMS grades. The generator must include effective drying, filtration, monitoring, and distribution controls.
At very high purity, small leaks, unsuitable pipe materials, moisture ingress, and analyzer errors can have a significant effect. CMS selection must therefore be combined with a complete system design that protects the nitrogen after it leaves the adsorption towers.
Metal Heat Treatment
Nitrogen atmospheres are used in heat treatment to reduce oxidation and help maintain controlled processing conditions. The required gas quality depends on the metal, temperature, furnace design, and acceptable surface condition. A continuous nitrogen supply can be more convenient than delivered gas cylinders for facilities with regular demand.
Coal, Mining, and Fire Prevention
Nitrogen can be used to reduce oxygen concentration in selected mining or storage environments and to support fire-prevention strategies. These applications require careful safety engineering and compliance with relevant regulations. CMS performance should be evaluated under the actual flow and pressure conditions, particularly when demand changes rapidly.
Advantages Over Less Specialized Adsorbents
Carbon molecular sieve has an important advantage over general-purpose activated carbon because its pore structure is designed for kinetic separation. Ordinary activated carbon may have a high surface area, but surface area alone does not determine oxygen-nitrogen selectivity. CMS is engineered to provide a more suitable balance of pore size, diffusion rate, adsorption capacity, and mechanical form.
CMS also offers advantages over technologies that are less flexible for variable demand. Cryogenic systems can be highly effective at large scale but may require greater capital investment, more complex operation, and longer startup procedures. Membrane systems can be compact and continuous, but the achievable purity, recovery, and flow characteristics may differ from those of PSA. Delivered nitrogen eliminates on-site generation but introduces transport, storage, scheduling, and supply-chain considerations.
Within the CMS market, the main competitive advantages claimed for the supplied products are controlled raw materials, proprietary carbon-based formulation, continuous production, a relatively high proportion of CMS-280 and higher grades, cooperation with research institutions, ISO 9001 certification, and testing in nitrogen generators before shipment.
These advantages matter because a nitrogen generator is a system rather than a bag of adsorbent. A product that performs consistently in the customer’s equipment can deliver more value than a nominally inexpensive product whose characteristics vary from batch to batch.
Installation, Storage, and Handling Recommendations
Storage Before Filling
CMS should remain sealed in moisture-resistant packaging until it is ready to be loaded into the adsorption tower. Bags or drums should be stored in a clean, dry indoor location away from rain, condensation, chemicals, and direct sources of heat. Damaged packages should be inspected before use.
Exposure to humid air can increase the initial water load and prolong the time required for the generator to reach stable operation. In severe cases, moisture can reduce adsorption capacity or cause the material to perform differently from the factory test condition.
Filling the Adsorption Tower
The tower should be clean and free from oil, water, rust flakes, and loose debris before filling. Screens, support layers, distributors, and retaining components must be installed correctly. CMS should be poured or conveyed in a manner that minimizes breakage and segregation.
Excessive drop height can damage pellets and create fines. The bed should be leveled and filled to the specified height and bulk density. After filling, the vessel should be closed securely, and the system should be checked for leaks before operation.
Startup and Conditioning
A new CMS bed may require a conditioning period to remove moisture and stabilize the adsorption process. Startup should follow the equipment manufacturer’s instructions. Product nitrogen should not be sent to the end-use process until the oxygen concentration and moisture level meet the required specification.
Early monitoring should include product purity, flow, pressure, temperature, pressure drop, and compressor operation. An unusual pressure drop or rapid purity deterioration may indicate contamination, poor filling, valve malfunction, channeling, or excessive fines.
Maintenance and Service-Life Considerations
CMS service life is influenced by the quality of feed air, pressure cycling, mechanical vibration, temperature, cycle design, and the frequency of abnormal operating events. Clean and dry air is the most important protection. Oil contamination, liquid water, compressor carryover, and repeated high-temperature operation can shorten the life of the adsorbent.
Operators should monitor nitrogen purity continuously or at regular intervals. A gradual increase in product oxygen may indicate normal aging, moisture contamination, oil contamination, valve leakage, or a change in cycle performance. A sudden change is more likely to indicate equipment malfunction or a severe process upset.
Pressure drop should also be tracked. An increase may result from dust accumulation, bed compaction, damaged screens, blocked filters, or pellet breakdown. Excessive pressure drop increases compressor energy use and can reduce the gas flow available for production.
Valves are critical components in PSA systems because they operate frequently. Valve leakage can mix regeneration gas with product gas, reduce pressure equalization effectiveness, and destabilize purity. Regular inspection of valves, seals, drains, filters, analyzers, and control instruments should form part of the maintenance program.
Choosing the Appropriate CMS Grade
The choice among CMS-240, CMS-260, CMS-280, and CMS-330 should begin with the required nitrogen purity and flow. The customer should then evaluate available compressor capacity, adsorption pressure, tower volume, cycle timing, air quality, operating temperature, nitrogen recovery, and acceptable energy consumption.
CMS-240 may be appropriate for general-purpose systems and applications where the required output and purity fall within its performance range. CMS-260 can provide a higher reported output at equivalent listed purity points. CMS-280 is suitable for users seeking a stronger balance between high purity and production capacity. CMS-330 is intended for demanding output targets and high-performance PSA systems.
The grade should not be selected only by its numerical designation. The number is a product identifier, not a universal performance guarantee across all equipment designs. Customers should request a technical recommendation based on their actual generator, including tower dimensions, compressor model, feed-air temperature, operating pressure, cycle sequence, and required nitrogen flow.
A site trial or representative performance test can be useful for large installations. The trial should define the acceptance criteria in advance, including nitrogen purity, output, air consumption, pressure drop, stability over time, and acceptable operating temperature.
Company Capabilities and Customer Support
Anhui Zhuoxu New Material Technology Co., Ltd. is located in Xuancheng, Anhui Province, China. It is described as a wholly owned subsidiary of Huiya Group and operates a production base serving porous-carbon materials and related industrial applications. The company reports sales across China and exports to Asia, South America, the Middle East, and Southeast Asia.
The company’s capabilities extend beyond the manufacture of one adsorbent grade. Its reported activities include porous-carbon materials, nitrogen-equipment services, research into hard-carbon structures, and development of materials for new-energy storage and industrial gas separation. This broader technical background may support cooperation with customers that need more than a standard commodity product.
The company’s integrated approach includes raw-material coordination, dedicated formulation, continuous equipment, research cooperation, quality management, and application testing. For international customers, useful support should include product selection, technical data, packaging information, storage guidance, filling instructions, application recommendations, and after-sales communication.
Q&A
What is carbon molecular sieve used for?
Carbon molecular sieve is primarily used in PSA nitrogen generators to separate nitrogen from compressed air. It preferentially adsorbs oxygen and allows nitrogen to pass through as the product gas. It is used in chemical processing, oil and gas, food packaging, electronics, metal treatment, mining, pharmaceuticals, cable production, and other industries.
What is the difference between CMS-240, CMS-260, CMS-280, and CMS-330?
They are different carbon molecular sieve grades with different reported nitrogen production rates and air-to-nitrogen ratios at comparable purity levels. In the supplied data, CMS-330 provides the highest listed production rates, followed by CMS-280, CMS-260, and CMS-240. The correct grade depends on the nitrogen generator and required operating point.
Can CMS produce 99.999% nitrogen?
Yes. The supplied performance table lists 99.999% nitrogen for all four grades. However, achieving this purity requires suitable tower design, clean and dry feed air, appropriate pressure, correct cycle timing, reliable valves, sufficient regeneration, and accurate oxygen analysis.
Why does nitrogen output decrease as purity increases?
Higher nitrogen purity requires greater removal of oxygen from the product stream. The adsorption cycle must therefore provide a greater separation duty, which can involve lower product flow, higher air consumption, longer adsorption control, additional purge, or a larger amount of adsorbent. This is a normal operating relationship in PSA nitrogen generation.
What feed-air quality does CMS require?
The feed air should be clean, dry, and substantially free of oil vapor, liquid water, organic contaminants, and particulates. The supplied guidance identifies a dew point below approximately minus 40 degrees Celsius and oil content below approximately 0.3 parts per million, but the exact specification should be confirmed for the specific generator and CMS grade.
What adsorption pressure is recommended?
The supplied reference data use approximately 0.75–0.80 MPa. The general guidance identifies approximately 0.6–0.8 MPa for an atmospheric-pressure regeneration process. The final operating pressure should be chosen according to total energy consumption, equipment design, purity, output, and nitrogen recovery.
How does temperature affect CMS performance?
Adsorption is generally reduced as temperature rises. Higher feed-air temperature can therefore lower working capacity and reduce nitrogen output or purity. Cooling the compressed air and maintaining stable operating conditions can improve performance. The supplied information identifies an ambient temperature of approximately 15 degrees Celsius or lower as favorable for nitrogen-generator operation.
How long does carbon molecular sieve last?
Service life depends on feed-air quality, operating temperature, pressure cycling, mechanical conditions, cycle design, and maintenance. There is no universal service-life value for every installation. Proper pretreatment, moisture control, oil removal, careful filling, and stable operation can help extend the useful life of the bed.
Why is factory testing in a nitrogen generator important?
Dynamic PSA testing evaluates the material under application conditions rather than relying only on laboratory adsorption data. It can reveal differences in purity, output, mass-transfer behavior, pressure drop, dust formation, and regeneration response. This provides a more practical quality check before shipment.
How should customers select a CMS supplier?
Customers should review product data, batch consistency, application-test results, quality documentation, raw-material control, technical support, packaging, delivery capability, and after-sales service. ISO 9001 certification, manufacturing capacity, research capability, and the ability to test CMS in an actual nitrogen generator are useful indicators, but the product should also be evaluated against the customer’s own operating requirements.
Conclusion
Carbon molecular sieve is the functional heart of a PSA nitrogen generator. Its controlled micropores enable selective oxygen adsorption and nitrogen production at a practical industrial scale. The performance of the adsorbent affects nitrogen purity, output, air consumption, compressor energy, pressure drop, operating stability, and service life.
CMS-240, CMS-260, CMS-280, and CMS-330 provide a range of options for nitrogen purity requirements from 99% to 99.999%. The supplied performance figures show a clear relationship between purity, production rate, and air-to-nitrogen ratio. Users can therefore select a grade according to actual process needs instead of operating every generator at the highest possible purity.
The product advantages described by the manufacturer include selective pore structure, strong adsorption capacity, flexible PSA performance, cost-effective nitrogen generation, dedicated carbon-based formulation, controlled raw materials, continuous production equipment, a relatively high proportion of CMS-280 and higher grades, research cooperation, ISO 9001 certification, and testing in nitrogen generators before shipment.
For customers, the most important lesson is that CMS quality and system operation cannot be separated. Even a high-quality adsorbent requires dry, oil-free feed air, correct pressure, suitable temperature, optimized equalization, stable cycle timing, and careful maintenance. When these factors are properly controlled, the CMS product range can support dependable nitrogen generation across a broad range of industrial applications.
References
1. Supplier technical information for CMS-240, CMS-260, CMS-280, and CMS-330 carbon molecular sieve products.
2. Supplier operating guidance for PSA nitrogen generators, including air pretreatment, adsorption pressure, temperature, pressure equalization, and purity control.
3. Anhui Zhuoxu New Material Technology Co., Ltd. company information and manufacturing capability statement.
4. General engineering principles for pressure swing adsorption gas separation and nitrogen generation.
5. General technical literature on porous carbon materials, micropore control, adsorption kinetics, and activated carbon manufacturing.
6. Quality-management principles associated with ISO 9001 production and process-control systems.
Product: Carbon Molecular Sieve (CMS)
 E-mail
anhuilisa@126.com
 Phone
+86 18603224420
 Address
No. 26 Kunshan Road, Xuanzhou Economic Development Zone, Liqiao Town, Xuanzhou District, Xuancheng City, Anhui Province, P.R.China
Copyright Anhui Zhuoxu New Material Technology Co., Ltd. All rights reserved.
 Carbon Molecular Sieve Manufacturer Carbon Molecular Sieve Supplier