 English
 中文简体
 русский
 Français
 Español
 عربى
 CONTACT US


Carbon Molecular Sieve for High-Performance PSA Nitrogen Generation
2026-10-15
Content
- 1 What Is Carbon Molecular Sieve?
- 2 How CMS Produces Nitrogen in a PSA System
- 3 Key Performance Advantages of Carbon Molecular Sieve
- 4 Available CMS Grades for Nitrogen Generators
- 5 Comparison of the CMS Grades
- 6 Manufacturing Strengths and Process Control
- 7 Why Manufacturing Quality Matters More Than a Product Grade Alone
- 8 Feed-Air Preparation Requirements
- 9 Operating Conditions for Stable Performance
- 10 Applications Across Major Industries
- 11 Installation and Handling Recommendations
- 12 Maintenance and Service-Life Considerations
- 13 Advantages Over Less Specialized Adsorbents
- 14 Quality Assurance and Customer Support
- 15 How to Select the Correct CMS Grade
- 16 Q&A: Carbon Molecular Sieve for PSA Nitrogen Generators
- 16.1 What is the main function of carbon molecular sieve?
- 16.2 What CMS grades are available?
- 16.3 Which CMS grade has the highest reported production rate?
- 16.4 Can CMS produce 99.999% nitrogen?
- 16.5 Why does nitrogen production decrease when purity increases?
- 16.6 What adsorption pressure is recommended?
- 16.7 How important is feed-air drying?
- 16.8 Can oil damage carbon molecular sieve?
- 16.9 How long does CMS last?
- 16.10 Why is generator testing useful before shipment?
- 16.11 Is CMS-330 always the best choice?
- 16.12 What information should a customer provide when requesting a recommendation?
- 17 Conclusion
- 18 References
- 19 Product: Carbon Molecular Sieve (CMS)
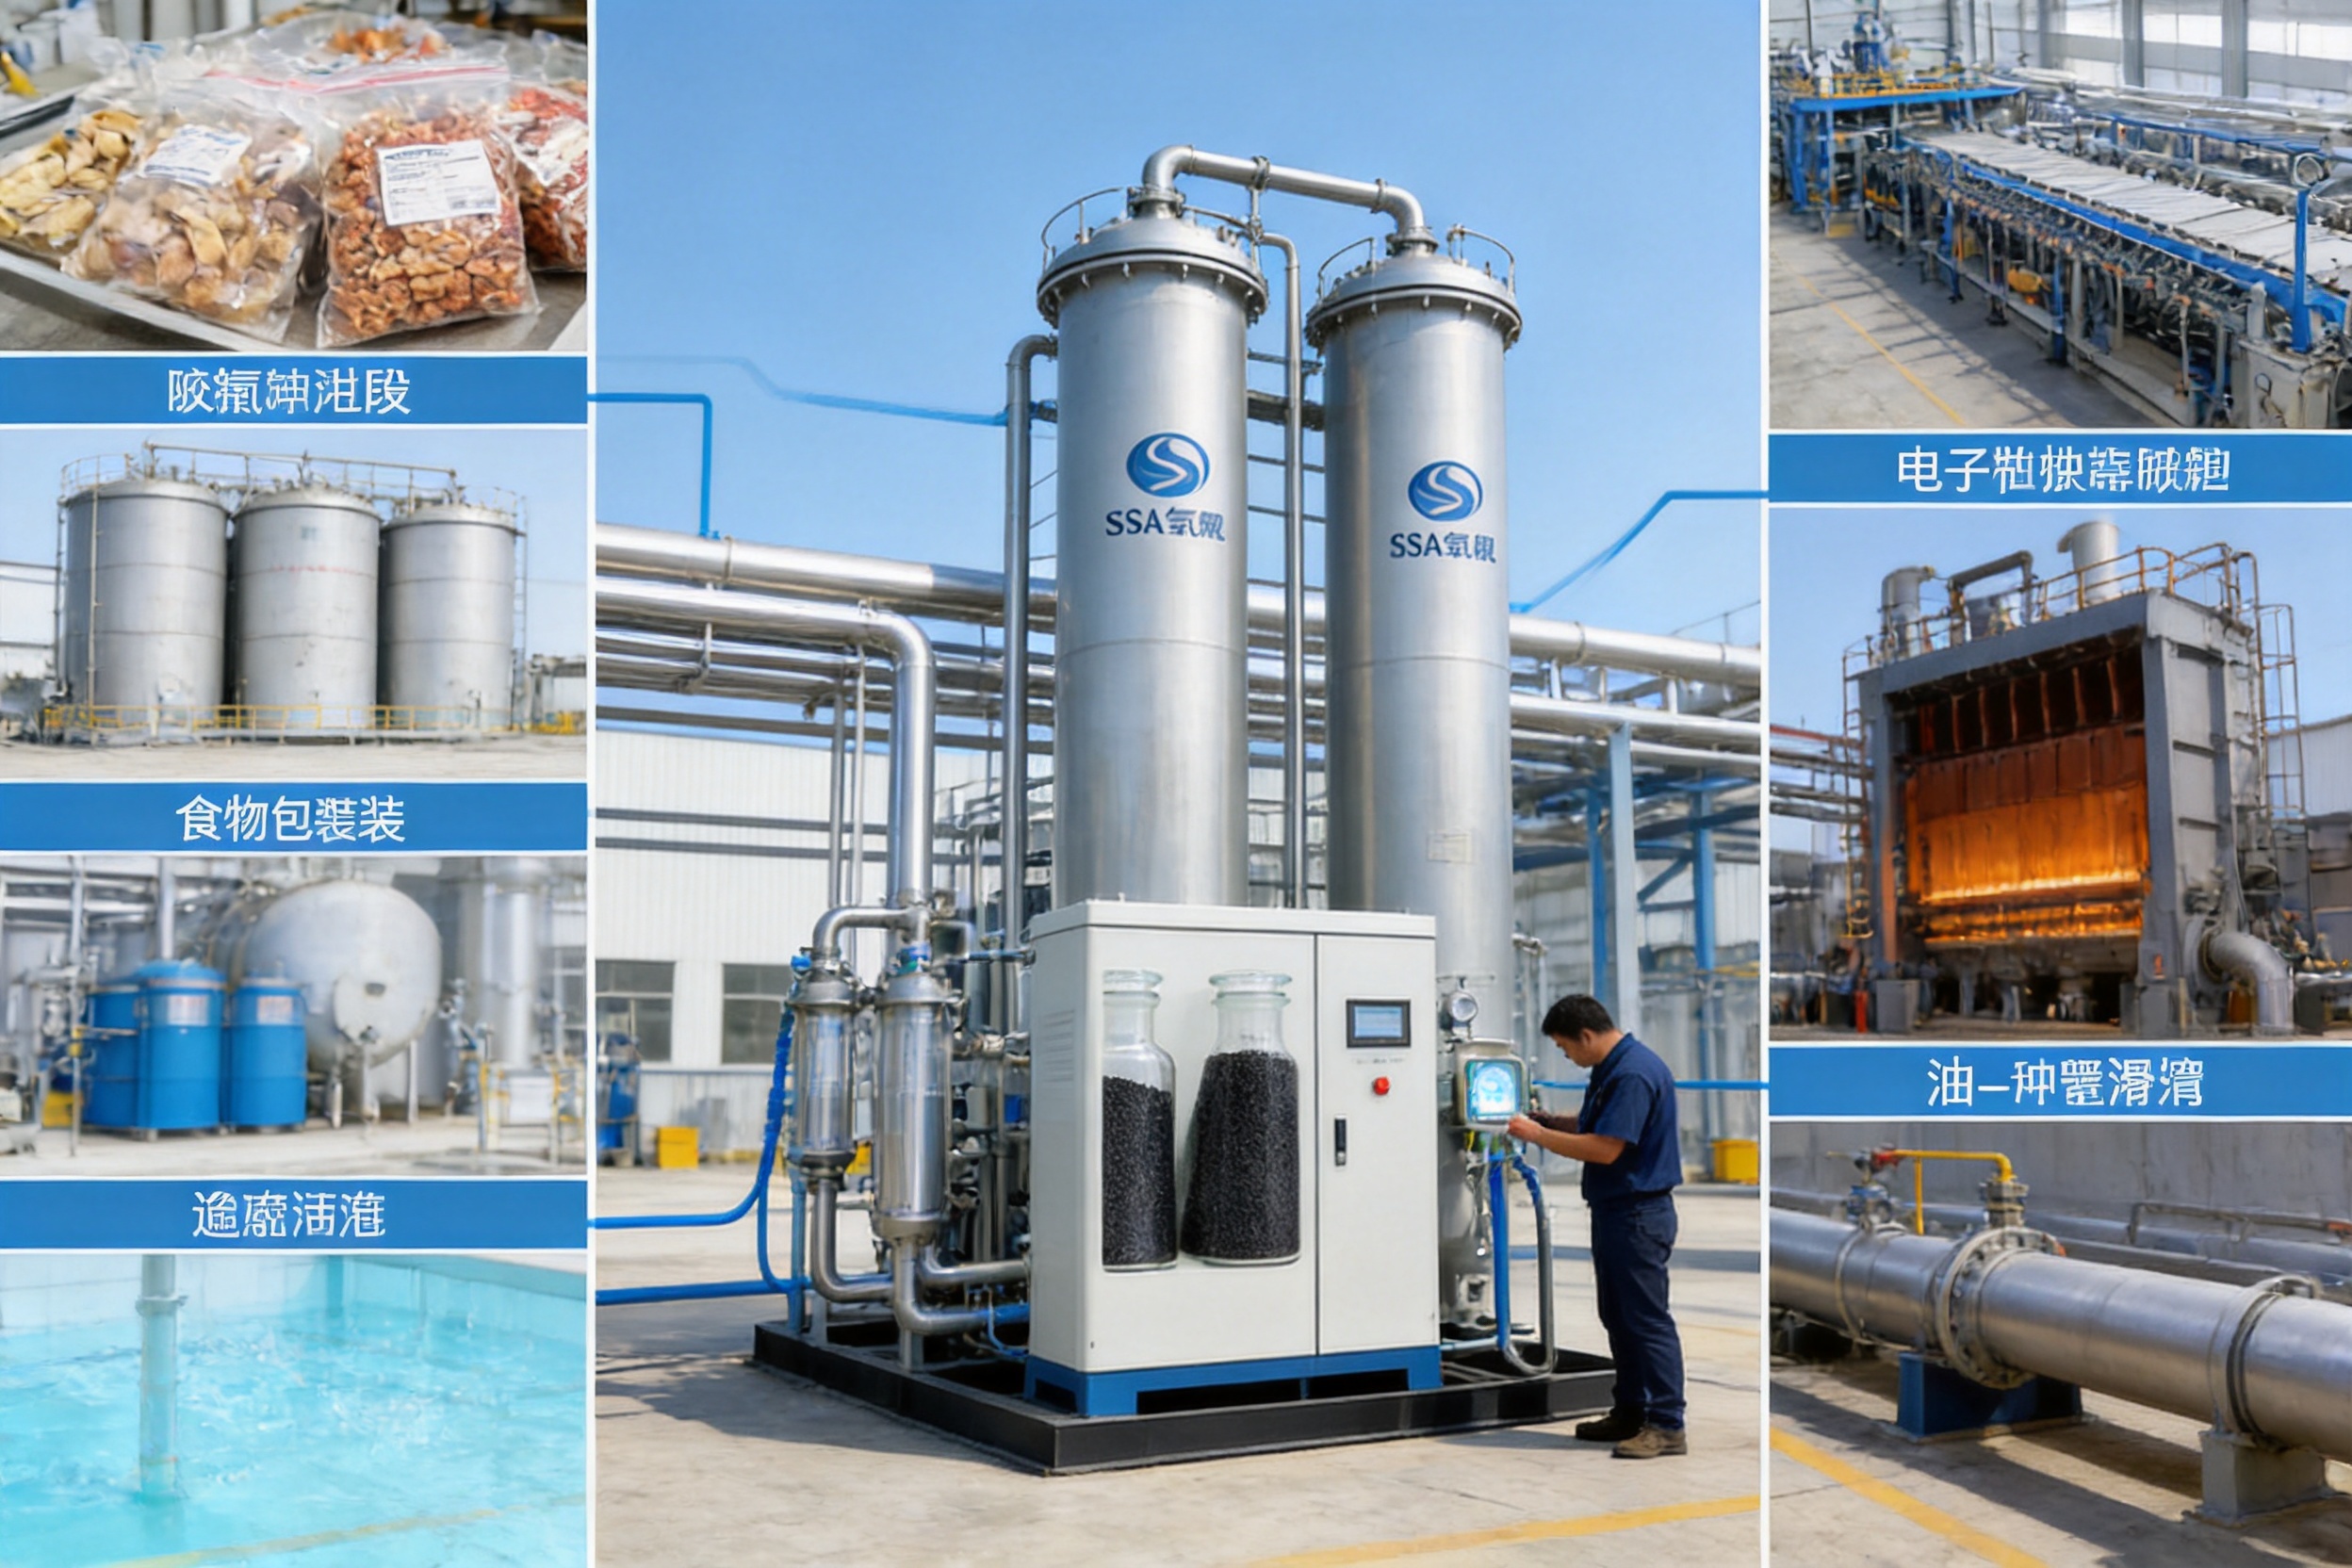
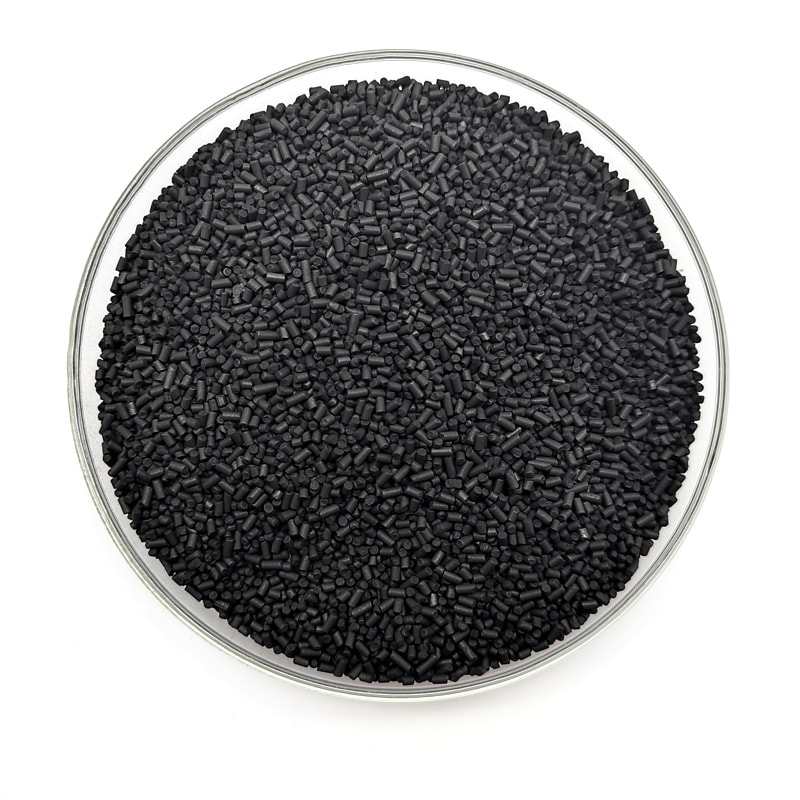
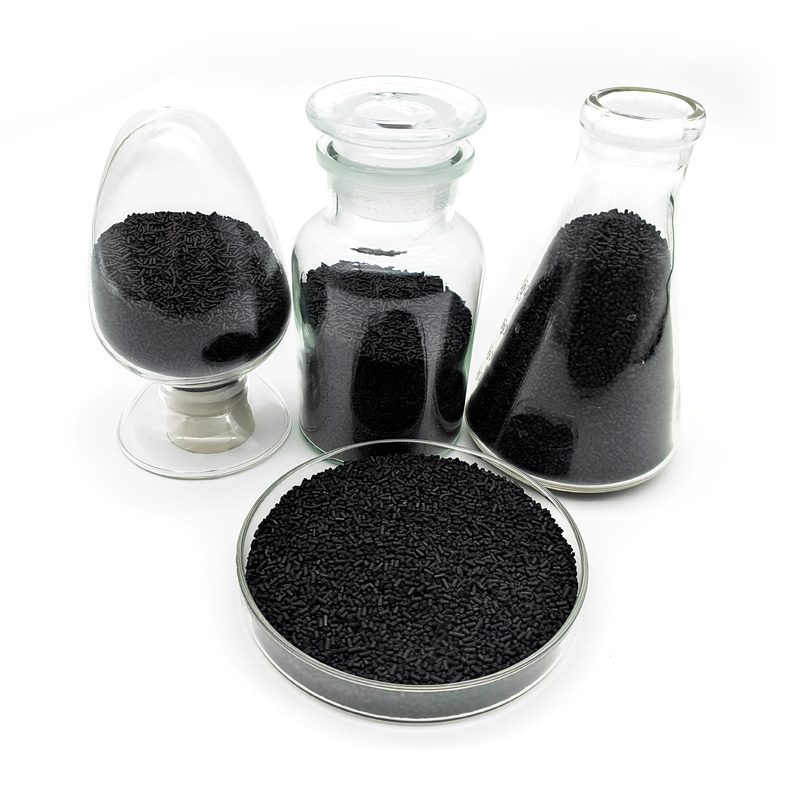
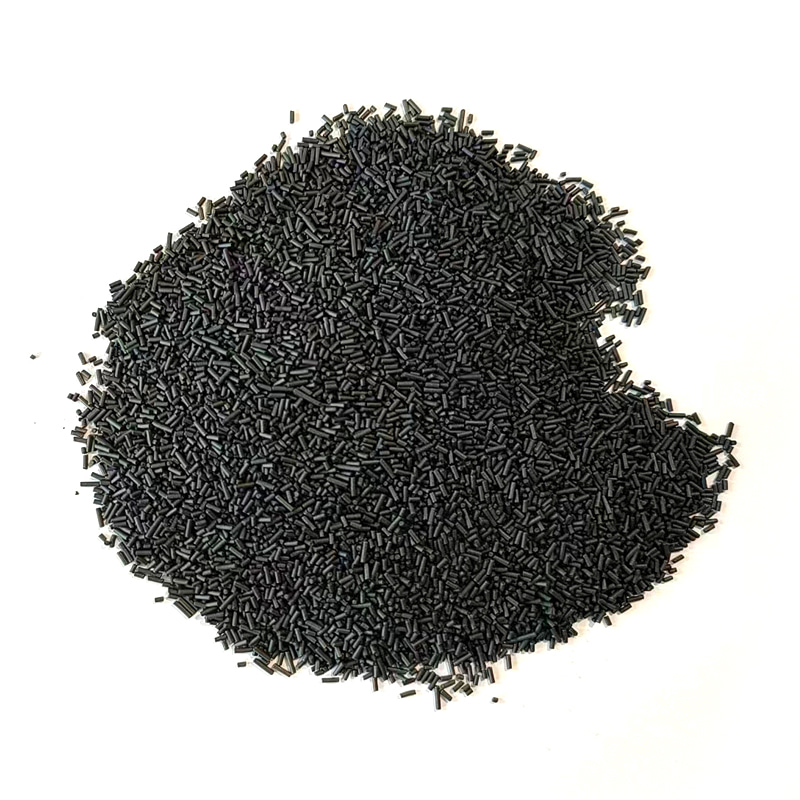
Carbon molecular sieve (CMS) is a specialized porous carbon adsorbent used to separate nitrogen from compressed air in pressure swing adsorption (PSA) nitrogen generators. By selectively adsorbing oxygen and allowing nitrogen to pass through the adsorption bed, CMS enables the continuous production of nitrogen with adjustable purity, flow rate, and operating cost.
For industrial users, the quality of the molecular sieve is one of the most important factors affecting nitrogen generator performance. A CMS with properly controlled pore size, high adsorption capacity, strong mechanical strength, low dust generation, and stable regeneration characteristics can improve nitrogen recovery, reduce energy consumption, extend equipment service life, and maintain reliable gas purity over long operating periods.
Anhui Zhuoxu New Material Technology Co., Ltd. supplies CMS-240, CMS-260, CMS-280, and CMS-330 carbon molecular sieve grades for PSA nitrogen generators. These grades are designed to support different combinations of nitrogen purity and production capacity, allowing equipment manufacturers, system integrators, and industrial gas users to select a suitable adsorbent for their process requirements.
What Is Carbon Molecular Sieve?
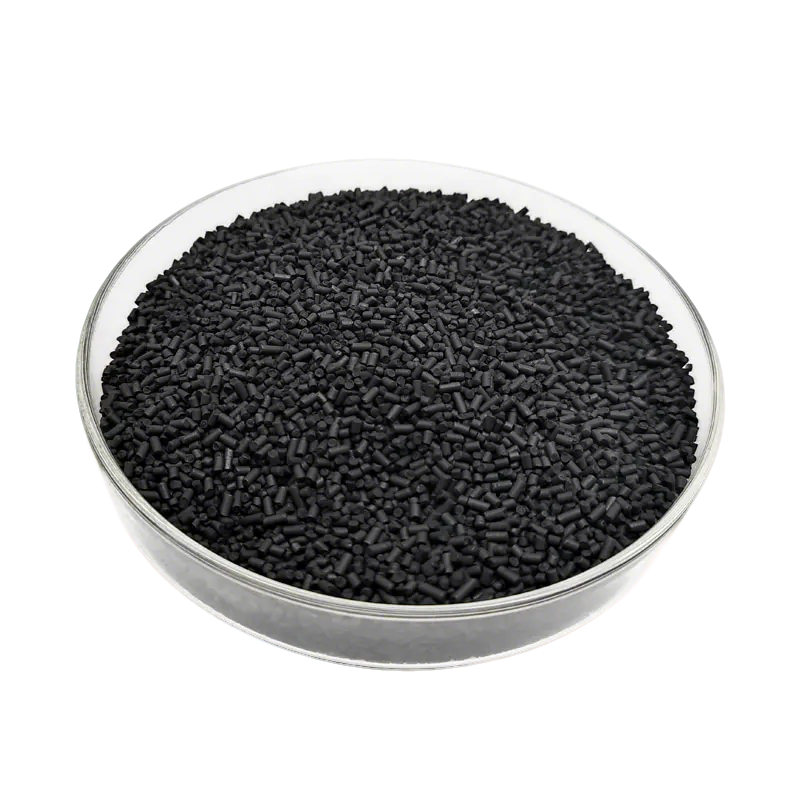
Carbon molecular sieve is a porous carbon material with a carefully controlled microporous structure. Its separation performance is based primarily on differences in the diffusion rates of gas molecules rather than only on differences in equilibrium adsorption capacity.
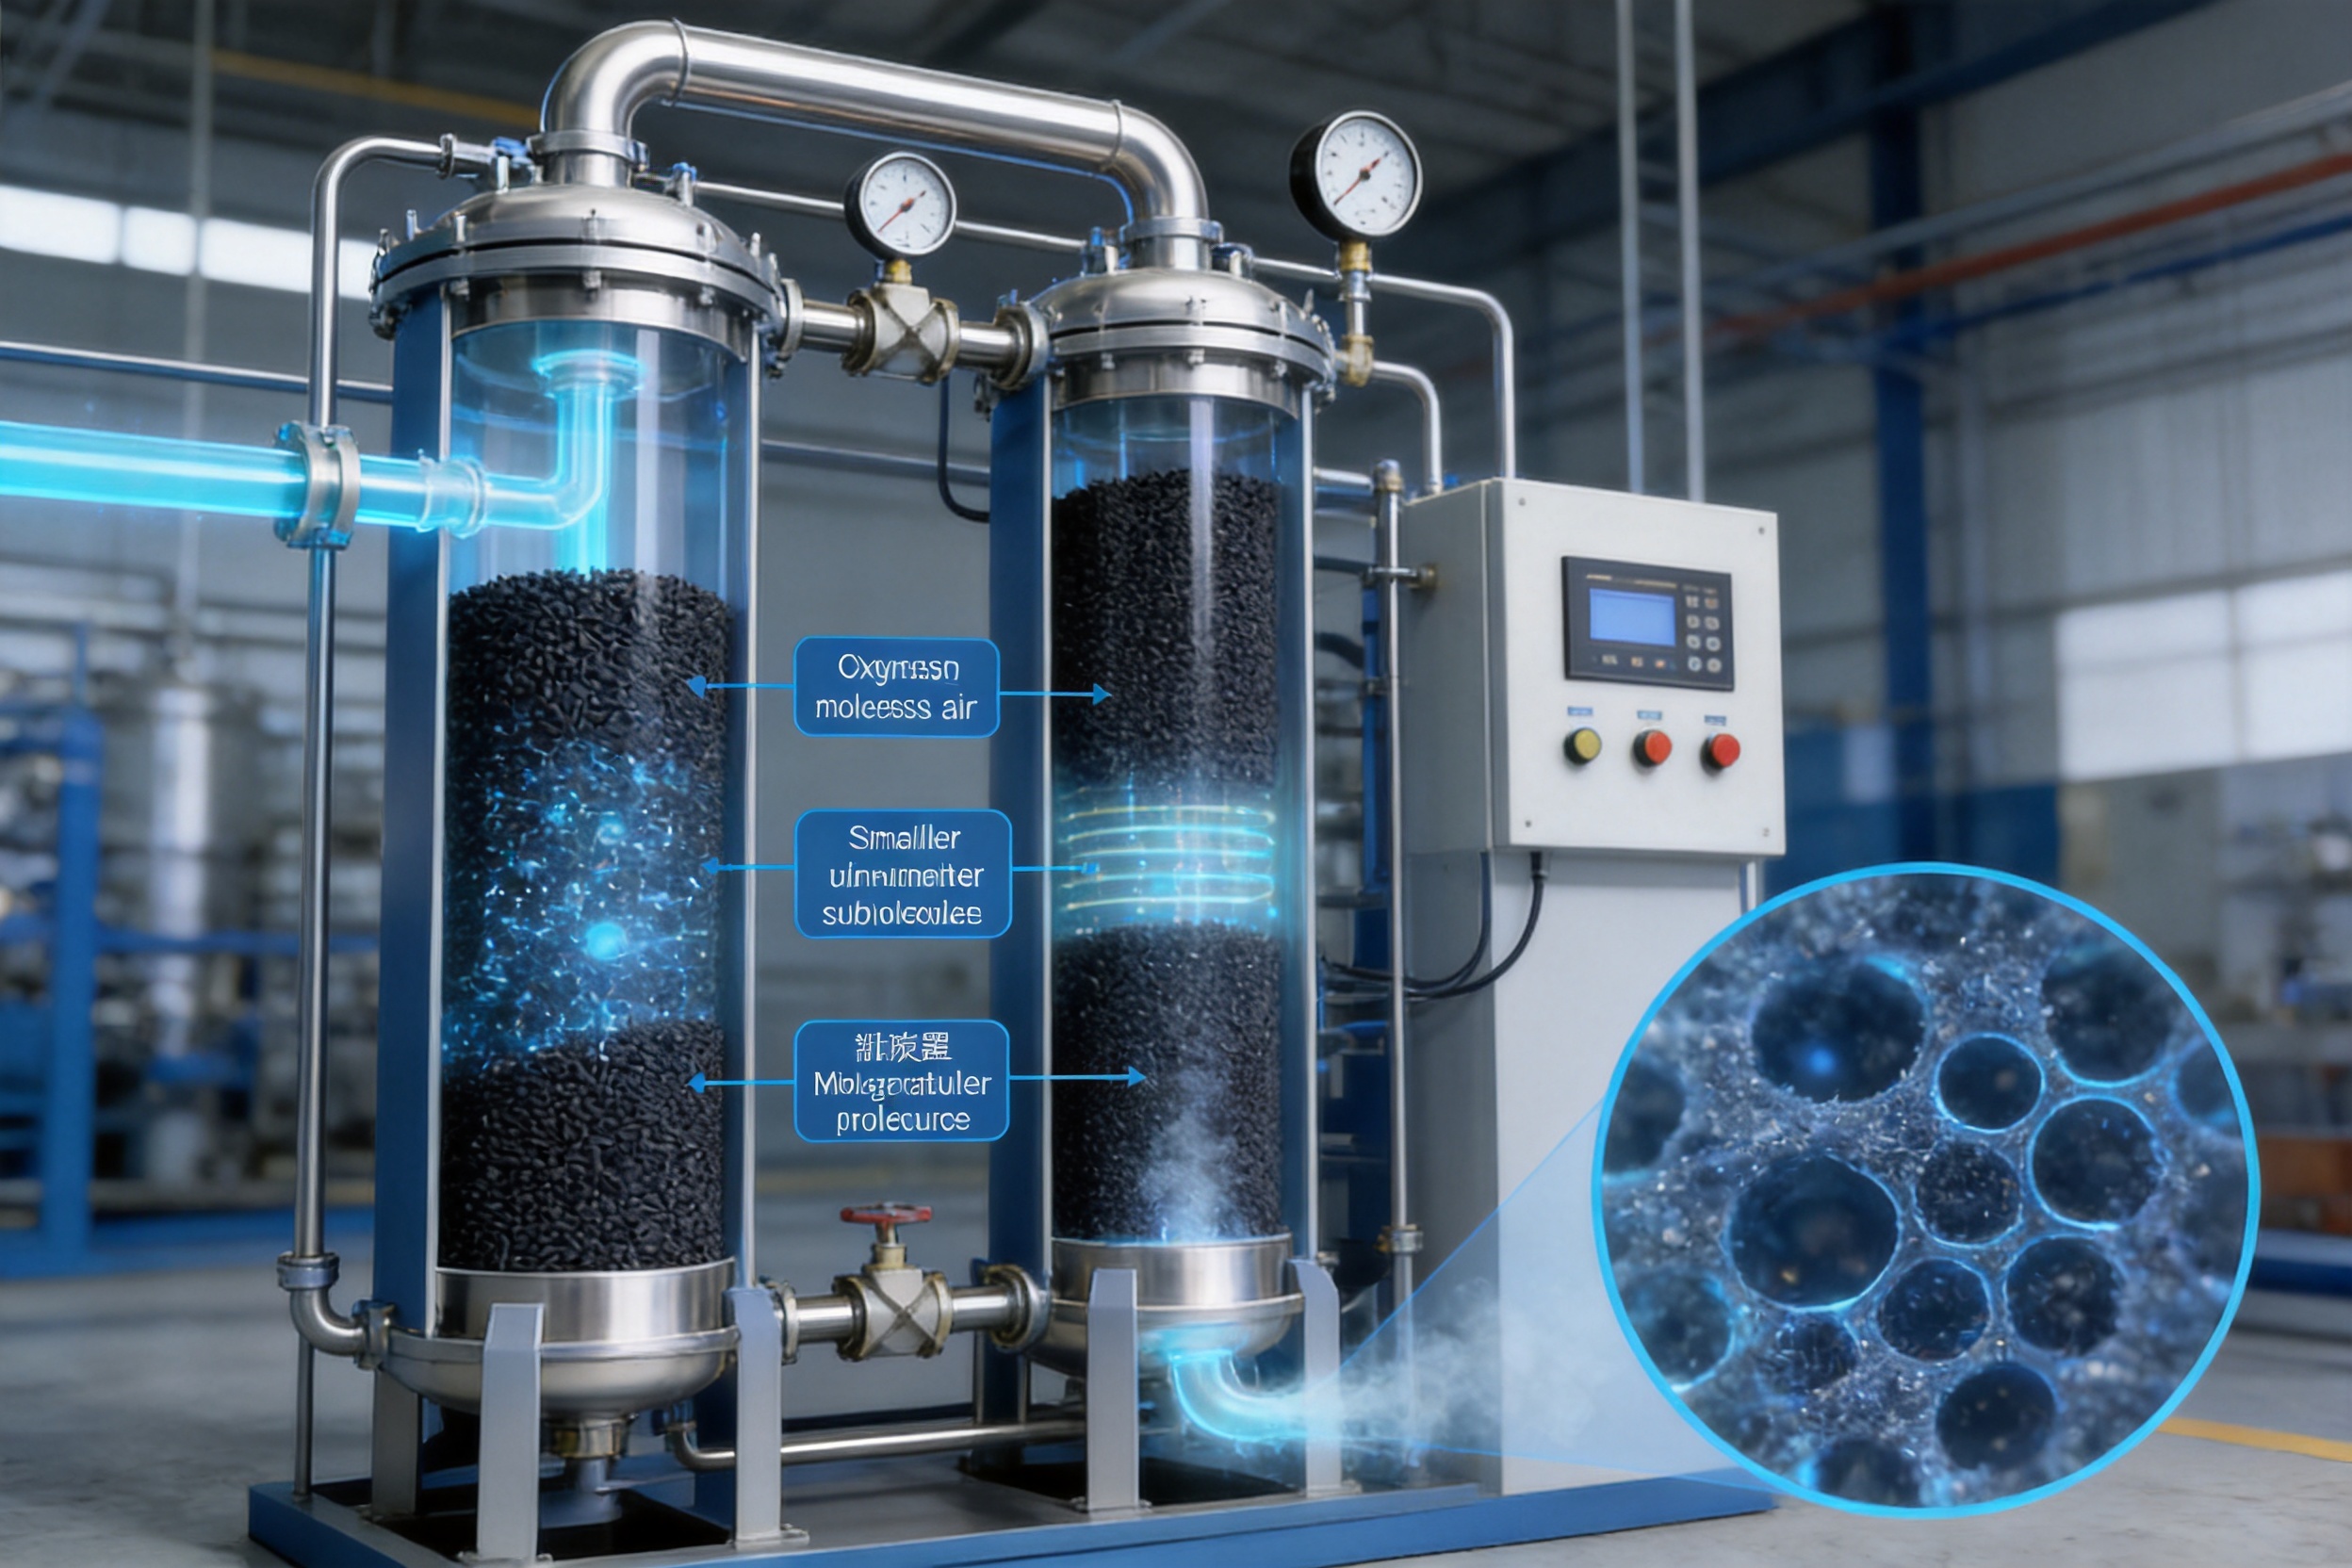
In compressed air, oxygen, nitrogen, argon, carbon dioxide, water vapor, oil vapor, and trace contaminants are present in different concentrations. The micropores in CMS are engineered so that oxygen molecules diffuse into the pore system more rapidly than nitrogen molecules. During the adsorption stage of a PSA cycle, oxygen is preferentially retained by the CMS, while nitrogen passes through the adsorption tower as the product gas.
The effective pore size of nitrogen-generation CMS is generally within the sub-nanometer range. The supplied product information identifies a typical pore-size range of approximately 0.28 to 0.38 nanometers. This narrow pore distribution is important because even small changes in pore structure can influence oxygen adsorption, nitrogen recovery, product purity, pressure drop, regeneration behavior, and operating stability.
Unlike ordinary activated carbon, CMS for nitrogen generation is not selected only for a large total surface area. A PSA adsorbent must combine pore-size selectivity with adequate adsorption kinetics and mechanical durability. It must also tolerate repeated pressurization, depressurization, equalization, and regeneration cycles without excessive abrasion or pulverization.
How CMS Produces Nitrogen in a PSA System
A typical PSA nitrogen generator contains two or more adsorption towers filled with carbon molecular sieve. While one tower is producing nitrogen, another tower is regenerated. The towers alternate continuously, creating a steady product-gas flow.
Adsorption Stage
Pre-treated compressed air enters an adsorption tower at an elevated pressure. Oxygen and other faster-diffusing components enter the micropores of the CMS more readily than nitrogen. Nitrogen therefore leaves the tower as the product gas, while oxygen is retained inside the adsorbent bed.
Pressure Reduction and Regeneration
When the CMS in the operating tower approaches its working adsorption capacity, the tower is depressurized. Lower pressure reduces the loading of the adsorbed gases and allows oxygen to leave the micropores. Depending on the equipment design, regeneration may occur through atmospheric-pressure depressurization, vacuum regeneration, or a combination of pressure release and purge gas.
Pressure Equalization
Many efficient PSA systems use pressure equalization between towers. Gas remaining in a completed adsorption tower is transferred to a regenerated tower from the top, bottom, or both directions. This recovers part of the compressed gas energy and reduces the pressure disturbance applied to the adsorbent.
The supplied operating guidance indicates that a pressure-equalization period of approximately one to three seconds may be suitable for many systems. The correct timing depends on tower volume, valve response, operating pressure, gas flow, bed geometry, and the selected CMS grade. Equalization that is too short may waste energy, while equalization that is too aggressive may increase mechanical stress and promote particle breakdown.
Repressurization
After regeneration, the tower is repressurized with product nitrogen, feed air, or a combination of both. The tower then returns to the adsorption stage. Correct sequencing is essential because the cycle must maintain the required product purity while minimizing nitrogen loss and compressor energy consumption.
Key Performance Advantages of Carbon Molecular Sieve
Selective Oxygen-Nitrogen Separation
The principal advantage of CMS is its selective gas-separation capability. The controlled micropores provide a kinetic separation mechanism that favors oxygen adsorption and diffusion. This makes CMS particularly suitable for PSA nitrogen generation, where the objective is to remove oxygen from air while recovering nitrogen as the product gas.
A uniform microporous structure helps reduce performance variation within the adsorbent bed. When pore-size distribution is properly controlled, the CMS can provide predictable adsorption kinetics and more stable purity during repeated PSA cycles.
High Adsorption Capacity
Carbon molecular sieve can maintain substantial adsorption capacity even when the concentration of a gas component is relatively low. This is important during the later part of an adsorption step, when oxygen concentration near the product end of the tower may be reduced.
High working capacity can allow a system to produce more nitrogen from a given quantity of adsorbent. It may also permit a smaller adsorption tower for a specified output, although actual equipment sizing must consider feed pressure, cycle time, purity, recovery, temperature, and allowable pressure drop.
Rapid Adsorption Kinetics
PSA nitrogen generation is a cyclic process. The adsorbent must respond rapidly to changes in pressure and gas composition. CMS with suitable diffusion characteristics can support short cycle times and high productivity per unit of adsorbent.
Rapid kinetics are especially valuable in compact nitrogen generators, modular systems, and applications requiring frequent changes in gas demand. However, speed must be balanced with mass-transfer-zone development. An excessively short cycle may not allow sufficient separation, while an excessively long cycle may reduce adsorbent utilization.
Adjustable Nitrogen Purity and Flow
One important advantage of PSA technology is its flexibility. Nitrogen purity and production rate can be adjusted according to the application. In general, increasing nitrogen purity requires a lower product flow rate or a higher quantity of feed air per unit of nitrogen. Reducing the flow rate gives the CMS more opportunity to remove oxygen and achieve a higher nitrogen concentration.
The supplied product data show performance points ranging from approximately 99% nitrogen purity to 99.999% nitrogen purity. These figures demonstrate the range of operating conditions supported by the different CMS grades. Actual results depend on the generator design, feed-air quality, cycle configuration, pressure, temperature, and measurement method.
Good Cost Efficiency
PSA nitrogen generation avoids the need to purchase and transport large quantities of liquid nitrogen or high-pressure nitrogen cylinders for many applications. Once the generator, compressor, purification system, and CMS beds are installed, nitrogen can be produced on demand at the point of use.
Carbon molecular sieve contributes to cost efficiency through its ability to operate in repeated pressure cycles, support high productivity, and generate nitrogen without cryogenic refrigeration. A well-matched CMS grade can reduce the amount of adsorbent and compressed air required for a given production target.
Broad Industrial Application
CMS-based nitrogen generators are used across a wide range of industries. Applications include chemical processing, oil and gas operations, electronics manufacturing, food packaging, pharmaceuticals, coal mining, cable production, metal heat treatment, transportation, warehousing, and storage.
Nitrogen may be used for inerting, blanketing, purging, oxidation prevention, fire and explosion-risk reduction, product preservation, pipeline drying, and controlled-atmosphere processing. The correct purity depends on the application. Some processes require only approximately 95% to 99% nitrogen, while sensitive electronics, pharmaceutical, or specialty chemical operations may require 99.999% nitrogen or a specified residual oxygen concentration.
Carbon Molecular Sieve (CMS)
Available CMS Grades for Nitrogen Generators
The CMS-240, CMS-260, CMS-280, and CMS-330 grades are designed to provide different performance levels in PSA nitrogen-generation systems. The grade number is used as a product designation and should not be interpreted as a universal industry standard. Users should compare complete technical data and conduct application testing before making a final selection.
| CMS Grade | Typical Adsorption Pressure | Target Nitrogen Purity | Reported Nitrogen Production Rate | Reported Air-to-Nitrogen Ratio |
|---|---|---|---|---|
| CMS-240 | 0.75–0.80 MPa | 99.999% | 70 m³/h·t | 6.5 |
| CMS-240 | 0.75–0.80 MPa | 99.99% | 110 m³/h·t | 4.6 |
| CMS-240 | 0.75–0.80 MPa | 99.9% | 165 m³/h·t | 3.6 |
| CMS-240 | 0.75–0.80 MPa | 99.5% | 240 m³/h·t | 2.6 |
| CMS-260 | 0.75–0.80 MPa | 99.999% | 80 m³/h·t | 6.4 |
| CMS-260 | 0.75–0.80 MPa | 99.9% | 175 m³/h·t | 3.5 |
| CMS-260 | 0.75–0.80 MPa | 99.5% | 260 m³/h·t | 2.5 |
| CMS-280 | 0.75–0.80 MPa | 99.999% | 90 m³/h·t | 6.2 |
| CMS-280 | 0.75–0.80 MPa | 99.9% | 195 m³/h·t | 3.3 |
| CMS-280 | 0.75–0.80 MPa | 99.5% | 280 m³/h·t | 2.3 |
| CMS-330 | 0.75–0.80 MPa | 99.999% | 100 m³/h·t | 6.2 |
| CMS-330 | 0.75–0.80 MPa | 99.9% | 250 m³/h·t | 3.3 |
| CMS-330 | 0.75–0.80 MPa | 99.5% | 330 m³/h·t | 2.3 |
The reported production rates should be treated as reference values rather than guaranteed results for every PSA generator. Nitrogen output is affected by tower dimensions, bed fill density, cycle time, valve performance, feed-air pressure, humidity, oil contamination, ambient temperature, and product-gas specifications.
Comparison of the CMS Grades
CMS-240 is suitable for nitrogen generators where the required purity and capacity are moderate or where the system is designed around a lower productivity grade. It may be considered for general inerting, packaging, storage, and industrial applications where the balance between air consumption and nitrogen output is acceptable.
CMS-260 provides a higher reported production rate than CMS-240 at comparable purity points. It may be appropriate for systems seeking a practical balance between nitrogen recovery, output, and investment cost.
CMS-280 is positioned as a higher-performance grade with reported production rates of up to 90 m³/h·t at 99.999% purity and 280 m³/h·t at 99.5% purity under the stated conditions. The company reports that approximately 90% of its CMS production reaches CMS-280 performance or above, indicating a manufacturing focus on higher-grade material consistency.
CMS-330 is designed for applications requiring a particularly high production rate. The supplied data report up to 100 m³/h·t at 99.999% purity, 250 m³/h·t at 99.9% purity, and 330 m³/h·t at 99.5% purity. This grade may help system designers reduce the amount of adsorbent needed for a target nitrogen flow, provided that the complete PSA design is optimized for the material.
Manufacturing Strengths and Process Control
Integrated Raw-Material Supply
A major challenge in CMS production is maintaining consistent raw-material quality. Variations in precursor composition, moisture, ash content, binder behavior, and carbonization characteristics can influence the final pore structure and adsorption performance.
Anhui Zhuoxu New Material Technology Co., Ltd. reports strategic cooperation with raw-material suppliers and access to exclusive raw materials through affiliated group companies. This integrated supply approach can reduce dependence on changing spot-market materials and help improve batch-to-batch consistency.
More direct control over raw materials can also reduce unnecessary intermediary costs. These cost savings may be passed to customers while preserving investment in process control, testing, and product development.
Specialized Carbon Material and Formulation Technology
The company uses a specialized carbon-material base developed for CMS production. The supplied information refers to a patented special floral-mud base material used in the carbon molecular sieve manufacturing process. According to the company, this formulation allows one ton of new CMS carbon material to produce a higher quantity of finished carbon molecular sieve compared with conventional approaches.
A high-yield formulation can improve material utilization and reduce manufacturing costs. More importantly, a controlled formulation can support consistent particle formation, pore development, mechanical strength, and adsorption kinetics. The commercial value of the formulation therefore depends not only on yield, but also on the performance of the final CMS in an operating nitrogen generator.
Continuous Production Equipment
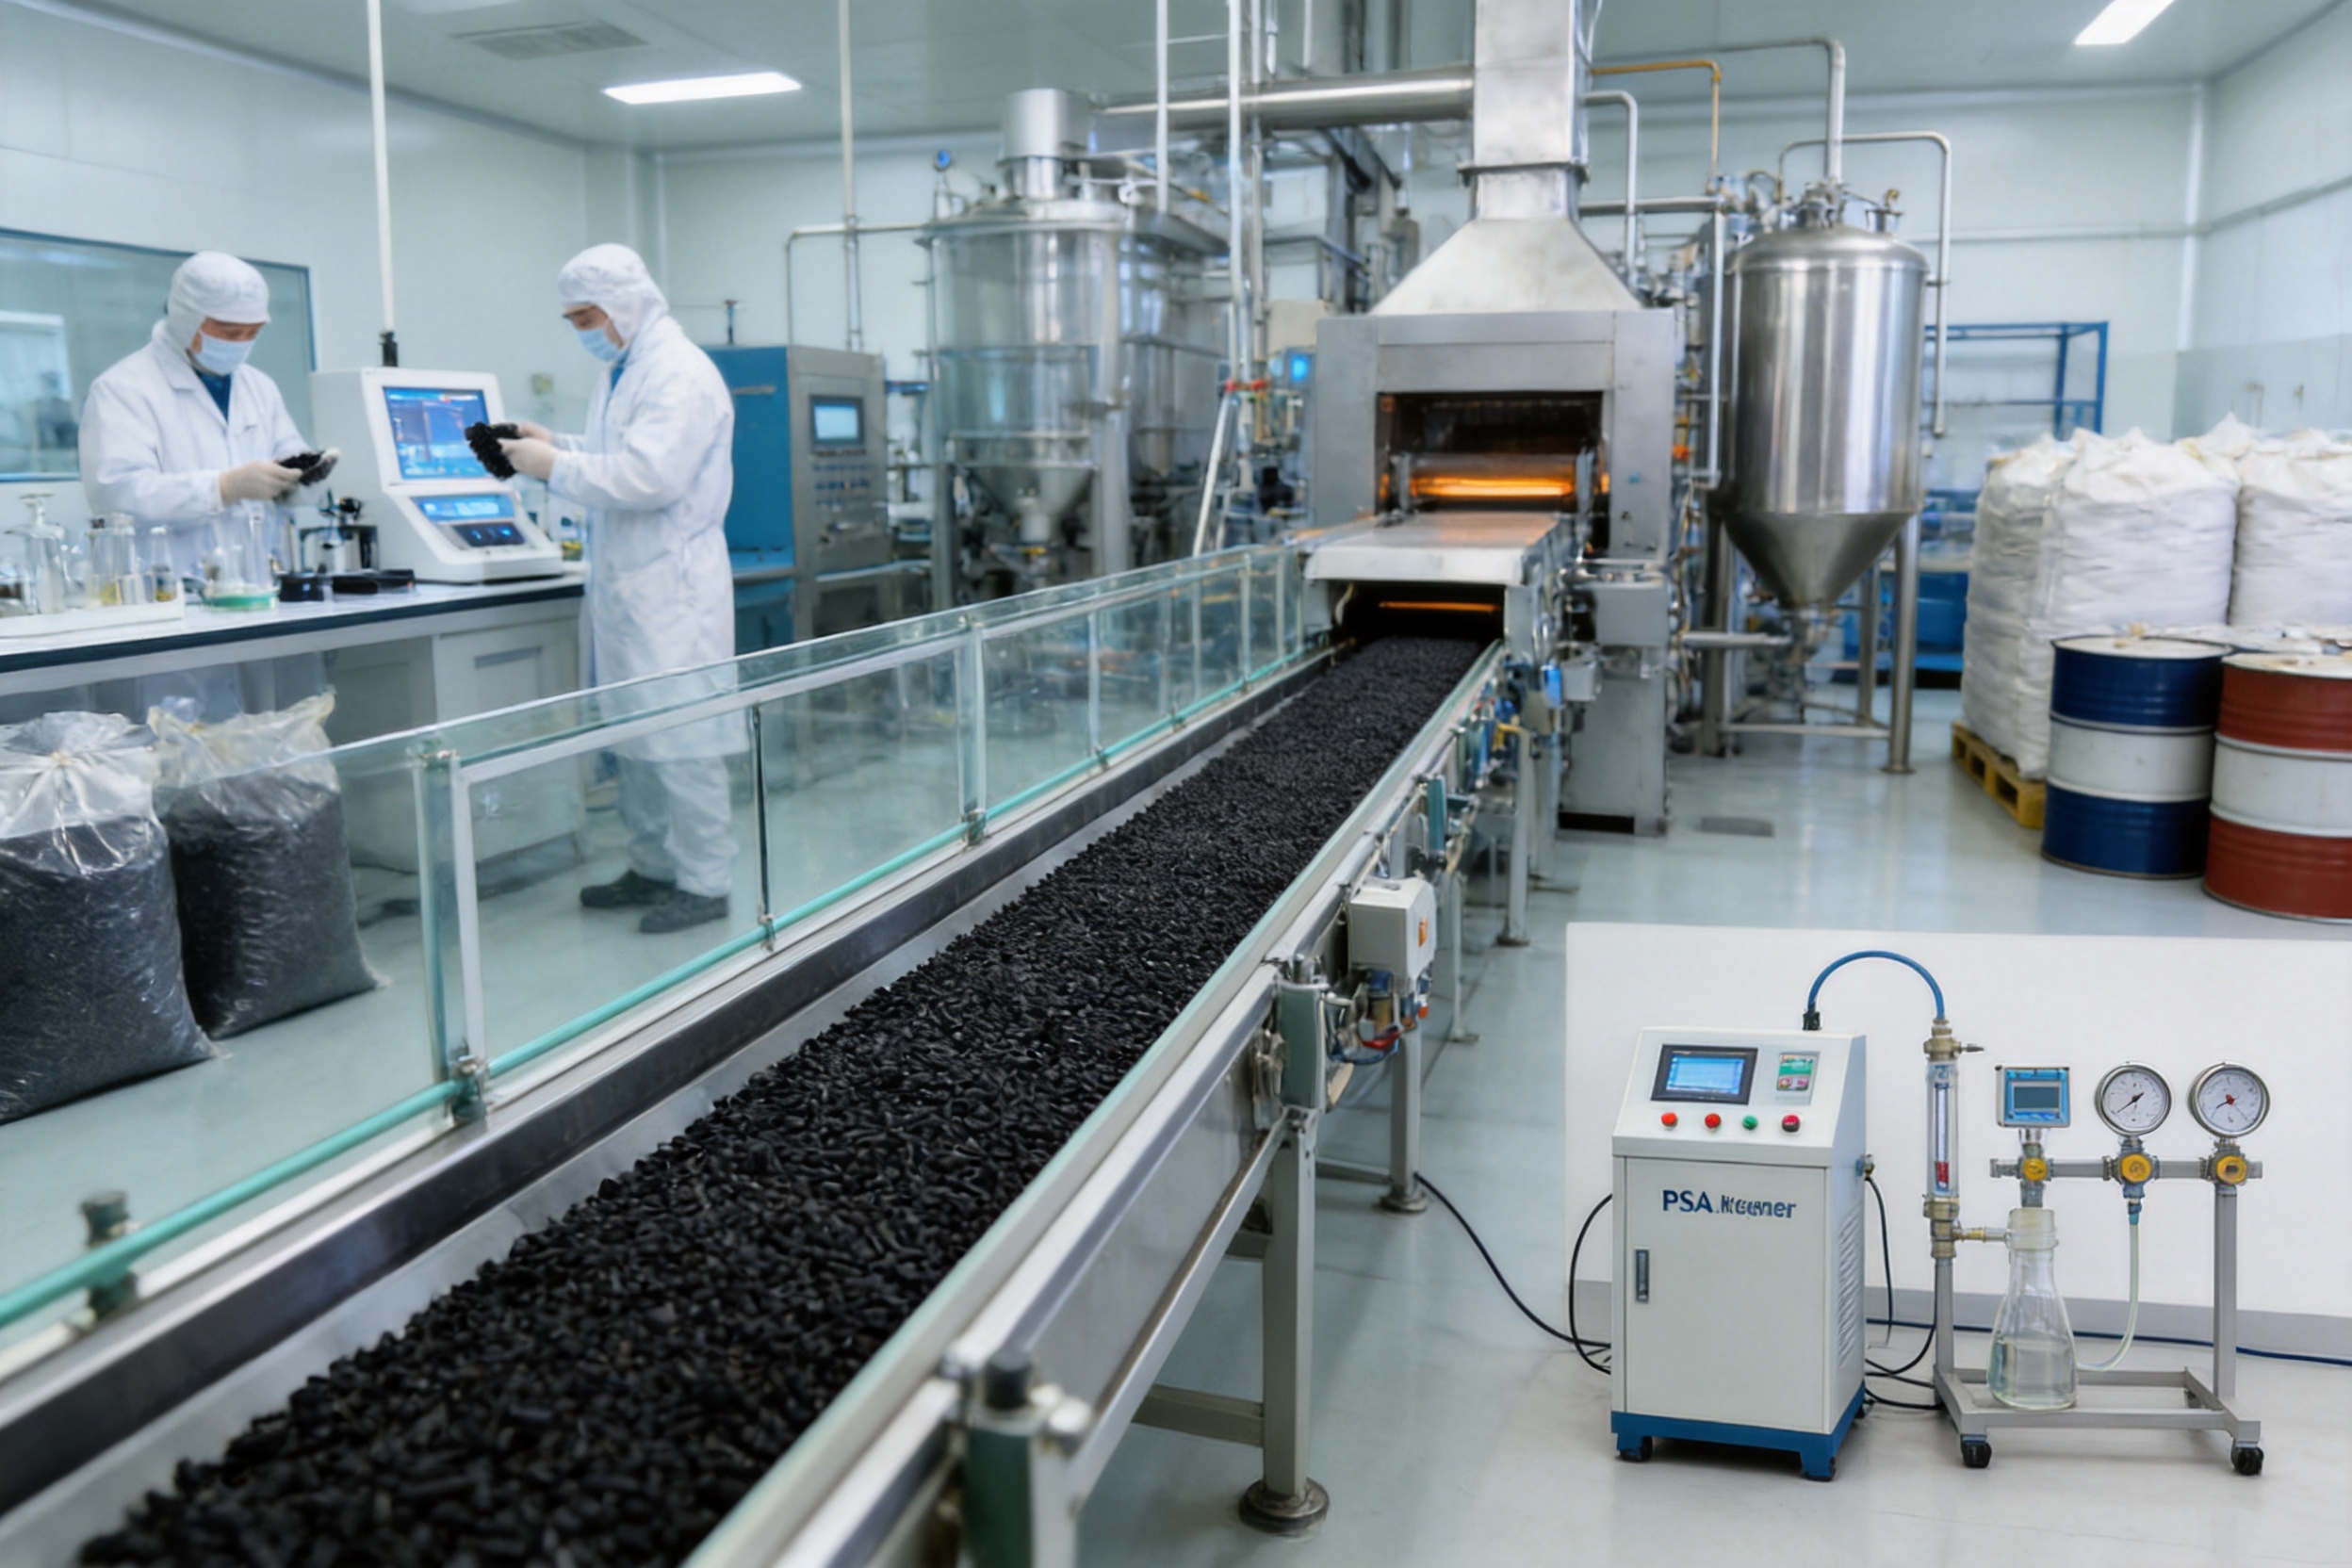
Continuous production equipment can provide several advantages over highly manual processing. Automated or continuous systems help stabilize residence time, temperature exposure, material flow, and production throughput. They can also reduce the number of direct workers required for routine operations.
Lower dependence on manual handling reduces the influence of individual operating habits on product consistency. It may also reduce contamination risks, improve process repeatability, and support more efficient production planning.
In carbon molecular sieve manufacturing, continuous control is especially important during shaping, drying, carbonization, activation, and final conditioning. Small differences in thermal history or moisture removal can produce measurable changes in the pore structure. Consistent equipment operation helps narrow these variations.
Location and Environmental Conditions
The company’s production base is located in northern Anhui Province, where relatively low atmospheric humidity is considered favorable for carbon molecular sieve production. Lower humidity can simplify moisture management during raw-material handling, shaping, drying, packaging, and storage.
Moisture control is important because water can occupy adsorption sites and affect the apparent performance of CMS during testing and commissioning. A controlled production environment helps ensure that finished material is properly dried and packaged before shipment.
Research and Development Cooperation
Anhui Zhuoxu New Material Technology Co., Ltd. reports cooperation with Jinan Shengquan Group and China University of Mining and Technology for research and development. Such cooperation supports the study of carbon materials, pore structures, adsorption behavior, and process optimization.
External technical cooperation can complement industrial manufacturing experience with academic research methods. It can also support the development of improved CMS grades, better process controls, and more efficient testing protocols.
Product Testing Before Shipment
The company states that CMS performance is tested in a nitrogen generator before the product leaves the factory. This is a significant quality-control approach because laboratory characterization alone cannot fully represent performance in a cyclic PSA process.
Generator-based testing can evaluate nitrogen purity, nitrogen flow, pressure behavior, air consumption, cycle stability, and the interaction between the adsorbent and the equipment. It provides a more application-oriented assessment than relying only on measurements such as iodine number, surface area, crush strength, or particle-size distribution.
Testing the material in a nitrogen generator also helps identify unsuitable batches before shipment. This can reduce the risk of commissioning problems and give customers greater confidence that the product has been evaluated under practical operating conditions.
Why Manufacturing Quality Matters More Than a Product Grade Alone
Two CMS products with similar grade names may not perform identically in the same nitrogen generator. The final result depends on a combination of pore structure, particle size, bulk density, crush strength, attrition resistance, moisture content, bed design, cycle timing, and feed-air preparation.
A high-capacity CMS can provide excellent productivity when used under suitable conditions. However, if the material generates excessive dust, has inconsistent particle dimensions, or is exposed to oil and liquid water, the advantages may be lost. For this reason, selecting a supplier with integrated production, documented quality control, and application testing is essential.
The company’s reported strengths address several of these concerns. Control over raw materials supports uniformity. Specialized formulation supports pore development and production yield. Continuous equipment reduces human variation. Low-humidity production conditions support moisture management. Research cooperation supports technological improvement. Nitrogen-generator testing links the product specification to real operating performance.
Feed-Air Preparation Requirements
Carbon molecular sieve is highly sensitive to contaminants that can block or damage the microporous structure. The compressed air entering the adsorption towers must therefore be properly cooled, separated, filtered, and dried.
Oil Removal
Oil vapor and liquid oil are among the most harmful contaminants for CMS. Oil can coat the external surface of particles and enter the micropores, reducing oxygen adsorption and slowing gas diffusion. In severe cases, oil contamination can permanently reduce the working capacity of the adsorbent.
Oil-lubricated compressors require suitable downstream treatment, including cooling, condensate separation, coalescing filtration, and adsorption or catalytic oil-removal equipment where necessary. The filtration system should be selected according to the compressor type, oil carryover level, operating pressure, and required gas quality.
Water and Moisture Control
Compressed air leaves the compressor at an elevated temperature and often contains substantial water vapor. As the air cools, liquid water may condense. Water entering the CMS bed can occupy adsorption sites, increase pressure drop, weaken particles, and interfere with accurate nitrogen production.
The supplied operating guidance identifies a feed-air dew point requirement below approximately minus 40°C and an oil-content target below 0.3 ppm. Because the source material contains formatting inconsistencies, users should confirm the exact dew-point and oil-content specifications with the supplier and equipment manufacturer before commissioning.
Particle and Chemical Contaminants
Dust, rust, compressor wear particles, and pipe scale can accumulate in the adsorption bed. These contaminants may increase pressure drop and obstruct gas flow. Appropriate particulate filters should be installed upstream of the CMS towers.
Organic vapors and chemical contaminants should also be evaluated. Solvents, plasticizers, cleaning chemicals, and process vapors may be adsorbed strongly by carbon materials and can be difficult to remove during normal regeneration. The air-treatment system should therefore be designed for the actual plant environment rather than only for a standard compressor outlet.
Operating Conditions for Stable Performance
Adsorption Pressure
Higher adsorption pressure generally increases the amount of gas that can be adsorbed by the CMS. However, excessive pressure increases compressor energy consumption, equipment requirements, valve stress, and capital cost.
The supplied data identify an adsorption pressure range of approximately 0.75 to 0.80 MPa for the listed performance points. General process guidance also suggests approximately 0.6 to 0.8 MPa for atmospheric-pressure regeneration systems. The optimum pressure should be established through a complete energy and productivity assessment rather than selected solely from the highest possible adsorption capacity.
Temperature
Adsorption is generally exothermic. As the CMS bed temperature increases, adsorption capacity may decrease. Higher temperature can therefore reduce nitrogen purity or production capacity if the cycle and feed conditions remain unchanged.
The supplied guidance recommends an ambient temperature of 15°C or lower for optimal nitrogen-generator performance. In practical installations, the compressor aftercooler, air receiver, dryer, tower insulation, ventilation, and room temperature should all be considered. The temperature inside an adsorption bed may be higher than the surrounding air because of compression and adsorption heat.
Cycle Time
Cycle time controls how long the CMS is exposed to feed air and how deeply it is regenerated. A short cycle can increase productivity but may cause incomplete separation or incomplete regeneration. A long cycle may improve utilization in some conditions but reduce overall productivity and increase the size of the equipment required.
The appropriate cycle depends on the CMS grade, adsorption-tower dimensions, feed-air pressure, target purity, product flow, and valve configuration. System designers should validate the cycle experimentally rather than applying a fixed timing to every grade.
Pressure Equalization
Pressure equalization can lower compressed-air consumption and reduce the pressure swing experienced by the adsorbent. The suggested equalization time of one to three seconds provides a starting point for system design, but exact timing must be matched to the generator hardware.
Gentle pressure transitions can help reduce attrition. Sudden valve opening, excessive gas velocity, or poor bed support may cause particle movement and dust formation. Proper distributors, screens, support layers, and valve sequencing are therefore important for long CMS service life.
Applications Across Major Industries
Chemical and Petrochemical Processing
Nitrogen is widely used to inert storage tanks, purge pipelines, protect reactive chemicals, and reduce oxygen exposure during manufacturing. PSA nitrogen generators can provide a dependable on-site supply for facilities that need continuous or intermittent nitrogen.
Oil and Gas
Oil and gas facilities use nitrogen for tank blanketing, pipeline purging, pressure testing, well-service operations, and maintenance activities. The required purity and flow can vary considerably, so the CMS grade and PSA system should be selected for the specific operating duty.
Food Packaging and Storage
Nitrogen can displace oxygen in food packages and storage environments, helping reduce oxidation and extend product shelf life. Applications may include snacks, coffee, edible oils, fresh produce, and other oxygen-sensitive products. Food applications require hygienic equipment design and suitable gas-quality verification.
Electronics Manufacturing
Electronics production often uses nitrogen during soldering, reflow, component storage, and process protection. Oxygen concentration control can influence solder quality, oxidation, and product reliability. High-purity CMS grades may be selected for systems requiring stable low-oxygen nitrogen.
Pharmaceutical Production
Pharmaceutical operations may use nitrogen for inerting, blanketing, drying, packaging, and protecting sensitive formulations. The nitrogen generator and air-treatment system must meet the site’s quality, validation, and contamination-control requirements.
Metal Heat Treatment
Nitrogen is used in furnaces and heat-treatment lines to reduce oxidation and control the processing atmosphere. Depending on the material and process, the nitrogen may be combined with hydrogen or another controlled gas. Stable flow and purity are essential for repeatable metallurgical results.
Cable, Mining, and Transportation Applications
Nitrogen can be used in cable manufacturing, coal-mine safety systems, tire inflation, transportation, and storage. On-site PSA generation is attractive where cylinder handling is inconvenient or where nitrogen demand is continuous.
Installation and Handling Recommendations
CMS should be transported and stored in sealed, moisture-resistant packaging. The material should not be exposed unnecessarily to rain, high humidity, oil mist, chemical vapors, or open air before loading.
Before filling an adsorption tower, the equipment should be clean and dry. Internal screens, distributors, support materials, valves, and seals should be inspected. Any loose construction debris or welding residue should be removed because it can contaminate the CMS and obstruct gas flow.
Loading should be performed carefully to avoid excessive drop height and particle breakage. The bed should be leveled evenly, and the recommended bulk density and fill height should be followed. After loading, the tower should be checked for channeling, voids, and uneven settling.
Initial commissioning should include gradual pressurization and controlled regeneration. Sudden pressure changes may move the bed or produce dust. Nitrogen purity should be monitored during startup until the system reaches stable operating conditions.
Maintenance and Service-Life Considerations
The service life of CMS depends heavily on the quality of feed air and the mechanical design of the generator. Clean, dry air helps preserve adsorption capacity. Stable pressure control prevents unnecessary stress. Proper valve maintenance reduces shock loading and cycle irregularities.
Filters and dryers should be inspected according to a preventive-maintenance schedule. Differential pressure across filters can indicate blockage or saturation. Dew-point instruments and oil monitors should be calibrated and checked regularly.
CMS performance may decline gradually because of moisture exposure, oil contamination, dust accumulation, thermal aging, or mechanical attrition. Changes in nitrogen purity, increased air consumption, increased pressure drop, or reduced product flow may indicate an adsorbent or equipment problem.
When troubleshooting, users should first verify feed-air quality, compressor operation, dryer performance, valve timing, pressure sensors, product-flow measurement, and analyzer calibration. Prematurely replacing CMS without checking the rest of the system may not solve the underlying problem.
Advantages Over Less Specialized Adsorbents
General-purpose activated carbon may have a high surface area, but it does not necessarily have the narrow pore structure and kinetic selectivity required for efficient oxygen-nitrogen separation. CMS is engineered specifically for the pressure-swing conditions of nitrogen generation.
Compared with an unsuitable adsorbent, properly manufactured CMS can provide more consistent nitrogen purity, higher productivity, better recovery, and improved cycle stability. Its value comes from the combination of pore-size control, adsorption kinetics, strength, and repeatable manufacturing—not from surface area alone.
The product range also provides an advantage over a one-grade approach. CMS-240, CMS-260, CMS-280, and CMS-330 allow system designers to match the adsorbent to the required purity, capacity, and air-consumption target. This flexibility can help avoid using an unnecessarily expensive high-performance material in a low-purity application or an insufficient grade in a demanding high-purity system.
Quality Assurance and Customer Support
Anhui Zhuoxu New Material Technology Co., Ltd. operates as a wholly owned subsidiary of Huiya Group and reports an annual production capacity of 4,000 tons of porous carbon materials and 30,000 cubic meters of floral foam. A second-phase 3,000-ton porous-carbon project is scheduled to begin operation in 2026, with a focus on porous carbon for PSA applications and new-energy materials.
The company reports 21 core patents and ISO 9001 certification. These resources support a structured approach to process management, technical development, and product quality control.
Its wider material platform includes Resin-Based Porous Carbon technology. This technology uses polymer resin as a precursor and high-temperature carbonization to form a stable hard-carbon structure. Although the company applies porous-carbon expertise across several industries, the same emphasis on precursor control, thermal processing, and pore-structure design is relevant to the development of CMS for gas separation.
The company serves customers in China and exports to Asia, South America, the Middle East, and Southeast Asia. Its integrated material and nitrogen-equipment capabilities can support customers that need more than a bulk adsorbent supplier. Technical assistance may include grade selection, application evaluation, performance testing, and coordination with PSA nitrogen-generator design.
How to Select the Correct CMS Grade
The first selection factor is the required nitrogen purity. A system requiring 99.5% nitrogen may be designed around a much higher production rate than a system requiring 99.999% nitrogen. The second factor is nitrogen demand, including average flow, peak flow, operating hours, and future expansion.
The third factor is the available compressed-air capacity. A CMS grade with a favorable production rate may still be unsuitable if the compressor cannot supply the required air volume at the correct pressure. The fourth factor is the operating environment, including ambient temperature, humidity, compressor type, contaminants, and maintenance capability.
System designers should also consider tower diameter, bed height, valve response, pressure equalization, regeneration method, purge requirements, and product-gas buffer capacity. A technical evaluation should compare nitrogen output, purity, air-to-nitrogen ratio, pressure drop, expected service life, and total cost of ownership.
Before commercial adoption, the selected grade should be tested in the customer’s nitrogen generator or in a representative pilot system. This approach confirms that the material performs as expected under actual cycle conditions rather than only under standardized laboratory measurements.
Q&A: Carbon Molecular Sieve for PSA Nitrogen Generators
What is the main function of carbon molecular sieve?
CMS selectively adsorbs oxygen from compressed air while allowing nitrogen to pass through the adsorption bed. This kinetic separation produces nitrogen for industrial use.
What CMS grades are available?
The listed grades are CMS-240, CMS-260, CMS-280, and CMS-330. They are designed for different combinations of nitrogen purity, production rate, and air consumption.
Which CMS grade has the highest reported production rate?
Among the listed grades, CMS-330 has the highest reported production rate at the stated purity points. The data indicate up to 330 m³/h·t at 99.5% nitrogen purity and up to 100 m³/h·t at 99.999% purity under the specified reference conditions.
Can CMS produce 99.999% nitrogen?
Yes. The supplied performance data include 99.999% nitrogen purity for CMS-240, CMS-260, CMS-280, and CMS-330. Actual purity depends on the generator design, cycle settings, feed-air quality, pressure, temperature, and flow rate.
Why does nitrogen production decrease when purity increases?
Higher purity requires more complete oxygen removal. This normally requires a lower product flow, a longer or more carefully controlled cycle, increased adsorbent capacity, or greater feed-air consumption. Therefore, a PSA generator generally produces less nitrogen at 99.999% purity than at 99.5% purity.
What adsorption pressure is recommended?
The product data list approximately 0.75 to 0.80 MPa for the reported performance values. General guidance for atmospheric-pressure regeneration systems identifies approximately 0.6 to 0.8 MPa. The final pressure should be optimized for the complete system.
How important is feed-air drying?
Feed-air drying is essential. Water can occupy adsorption sites, reduce CMS capacity, increase pressure drop, and contribute to particle degradation. A suitable dryer and condensate-removal system should be installed upstream of the adsorption towers.
Can oil damage carbon molecular sieve?
Yes. Oil vapor or liquid oil can block micropores and permanently reduce adsorption performance. Oil-lubricated compressors require effective oil removal and monitoring.
How long does CMS last?
Service life depends on feed-air quality, pressure cycling, temperature, valve operation, bed support, and maintenance. Clean and dry air, controlled pressure transitions, and regular equipment inspections can extend service life.
Why is generator testing useful before shipment?
Generator testing evaluates the CMS under cyclic adsorption and regeneration conditions. It can confirm practical nitrogen purity, production rate, and stability more directly than isolated laboratory measurements.
Is CMS-330 always the best choice?
Not necessarily. CMS-330 has higher reported productivity, but the best grade depends on the required purity, flow, compressor capacity, energy target, equipment design, and total operating cost. A lower grade may be more economical for a moderate-duty application.
What information should a customer provide when requesting a recommendation?
The customer should provide required nitrogen purity, nitrogen flow, operating pressure, ambient temperature, compressor type, feed-air quality, operating hours, regeneration method, tower dimensions, and any special gas-quality requirements.
Conclusion
Carbon molecular sieve is the functional core of many PSA nitrogen generators. Its controlled microporous structure enables selective oxygen adsorption, rapid gas separation, adjustable nitrogen purity, and cost-effective on-site nitrogen production.
The CMS-240, CMS-260, CMS-280, and CMS-330 grades provide a range of performance options for applications from general inerting and packaging to high-purity industrial gas generation. The supplied data indicate nitrogen purity levels from approximately 99% to 99.999%, with production rates that vary according to the selected grade and operating target.
The strongest advantage of a CMS supplier is not simply the availability of several product grades. Consistent raw materials, specialized formulation, continuous manufacturing equipment, humidity control, research cooperation, ISO 9001 quality management, and nitrogen-generator testing all contribute to dependable performance.
Anhui Zhuoxu New Material Technology Co., Ltd. combines porous-carbon manufacturing with PSA nitrogen-application knowledge. Its production capacity, patented technologies, integrated raw-material strategy, and application-oriented testing provide a foundation for supplying carbon molecular sieve to nitrogen-generator manufacturers and industrial users worldwide.
For the best result, CMS should be selected as part of a complete system evaluation. Feed-air treatment, adsorption pressure, temperature, cycle time, pressure equalization, tower design, and maintenance practices all influence the final outcome. When these factors are properly matched, high-quality carbon molecular sieve can support stable nitrogen production, lower operating costs, and long-term PSA system reliability.
References
1. Perry’s Chemical Engineers’ Handbook, sections concerning adsorption, gas separation, and pressure swing adsorption.
2. Ruthven, D. M., Principles of Adsorption and Adsorption Processes.
3. Yang, R. T., Gas Separation by Adsorption Processes.
4. ISO 9001, Quality Management Systems—Requirements.
5. Technical product information for CMS-240, CMS-260, CMS-280, and CMS-330 carbon molecular sieve.
6. Technical guidance on PSA nitrogen-generator design, feed-air purification, pressure equalization, and adsorbent handling.
7. Technical information concerning porous carbon materials and resin-based porous carbon production.
Product: Carbon Molecular Sieve (CMS)
 E-mail
anhuilisa@126.com
 Phone
+86 18603224420
 Address
No. 26 Kunshan Road, Xuanzhou Economic Development Zone, Liqiao Town, Xuanzhou District, Xuancheng City, Anhui Province, P.R.China
Copyright Anhui Zhuoxu New Material Technology Co., Ltd. All rights reserved.
 Carbon Molecular Sieve Manufacturer Carbon Molecular Sieve Supplier