 English
 中文简体
 русский
 Français
 Español
 عربى
 CONTACT US


Carbon Molecular Sieve for High-Efficiency PSA Nitrogen Generation
2026-10-05
Content
- 1 What Is Carbon Molecular Sieve?
- 2 How CMS Works in a PSA Nitrogen Generator
- 3 Principal Advantages of Carbon Molecular Sieve
- 4 Available CMS Grades and Performance Selection
- 5 Manufacturing Strengths and Process Control
- 6 Important Raw Air Pretreatment Requirements
- 7 Operating Conditions for Stable CMS Performance
- 8 How the Product Compares with Less Specialized Alternatives
- 9 Quality Control and Purchasing Considerations
- 10 Storage, Handling, and Installation
- 11 Applications of CMS Nitrogen Generation
- 12 Advantages of an Integrated Supplier
- 13 Frequently Asked Questions
- 13.1 What is the main purpose of carbon molecular sieve?
- 13.2 How do CMS-240, CMS-260, CMS-280, and CMS-330 differ?
- 13.3 Does the highest CMS grade always provide the lowest operating cost?
- 13.4 What purity levels can these CMS grades support?
- 13.5 Why is compressed-air pretreatment important?
- 13.6 What adsorption pressure is recommended?
- 13.7 What temperature is suitable for PSA nitrogen generation?
- 13.8 How long can carbon molecular sieve last?
- 13.9 Can CMS be used in an existing nitrogen generator?
- 13.10 How should CMS be stored before use?
- 13.11 What information should be provided when requesting a quotation?
- 14 Conclusion
- 15 References
- 16 Product: Carbon Molecular Sieve (CMS)
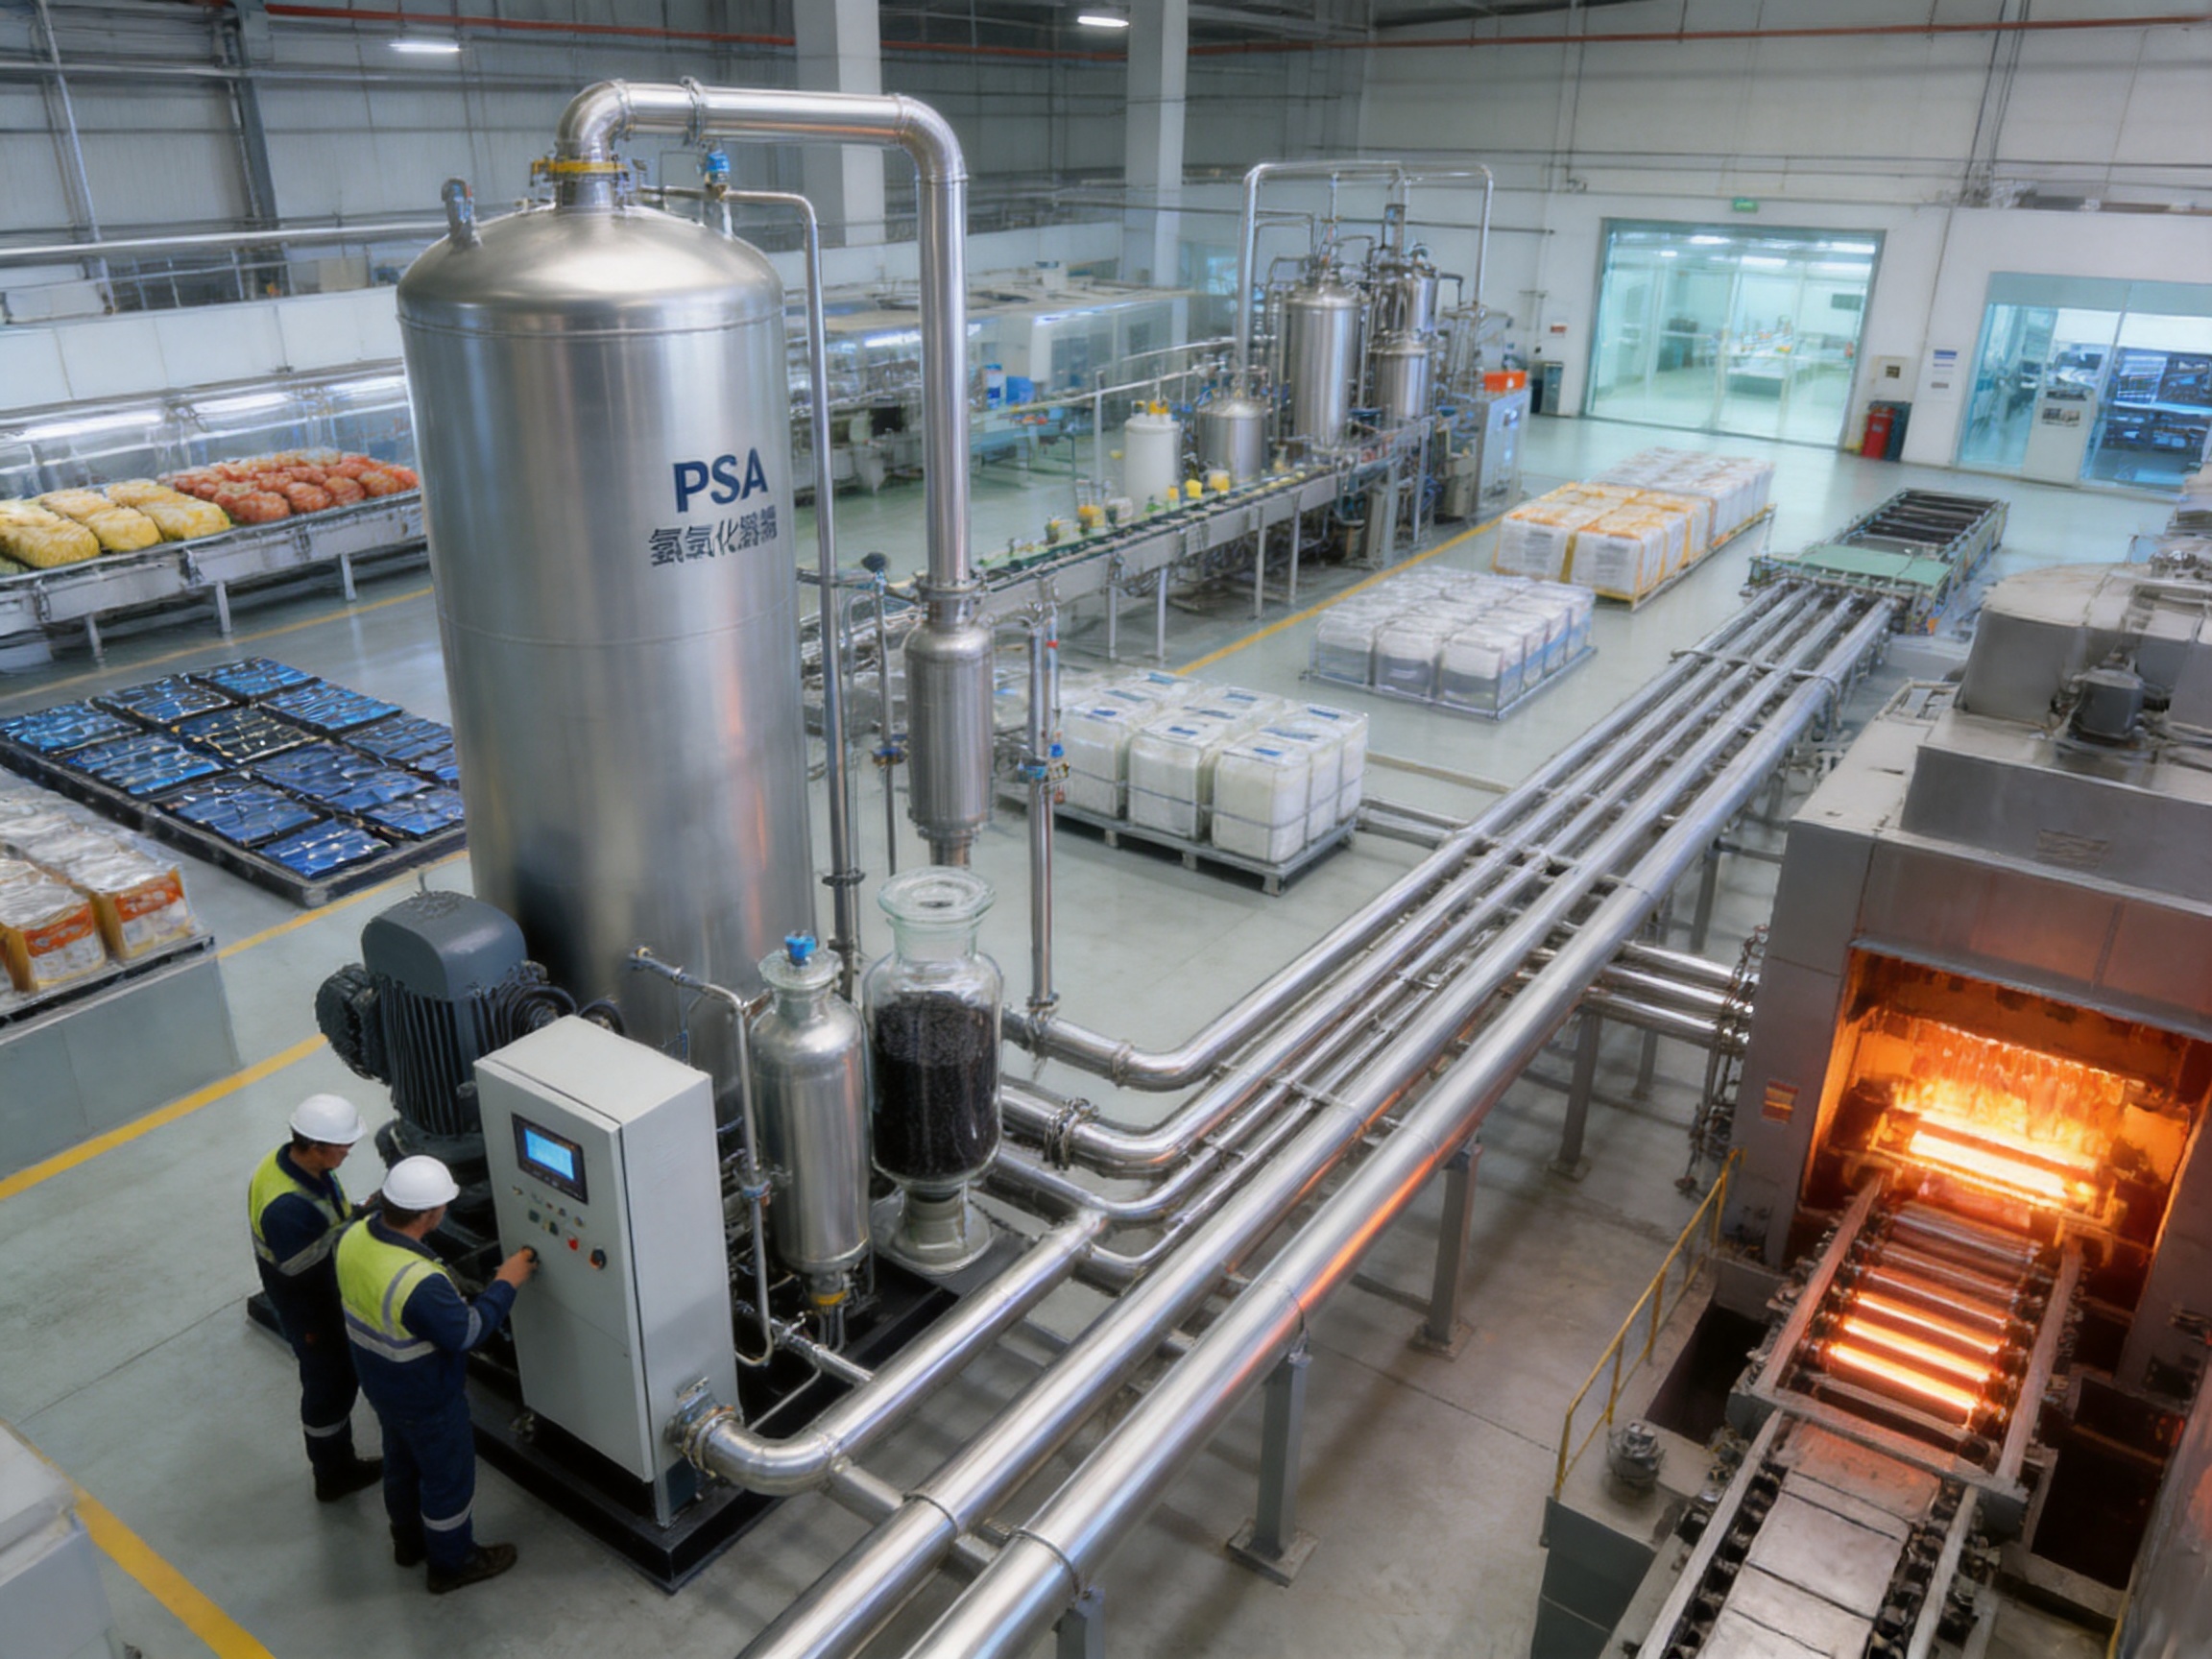
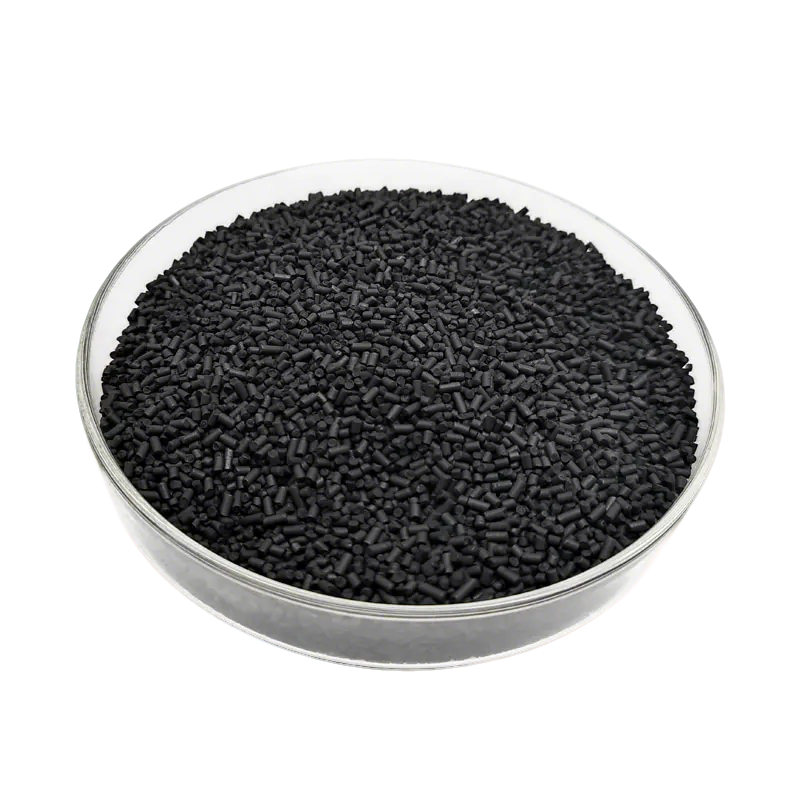
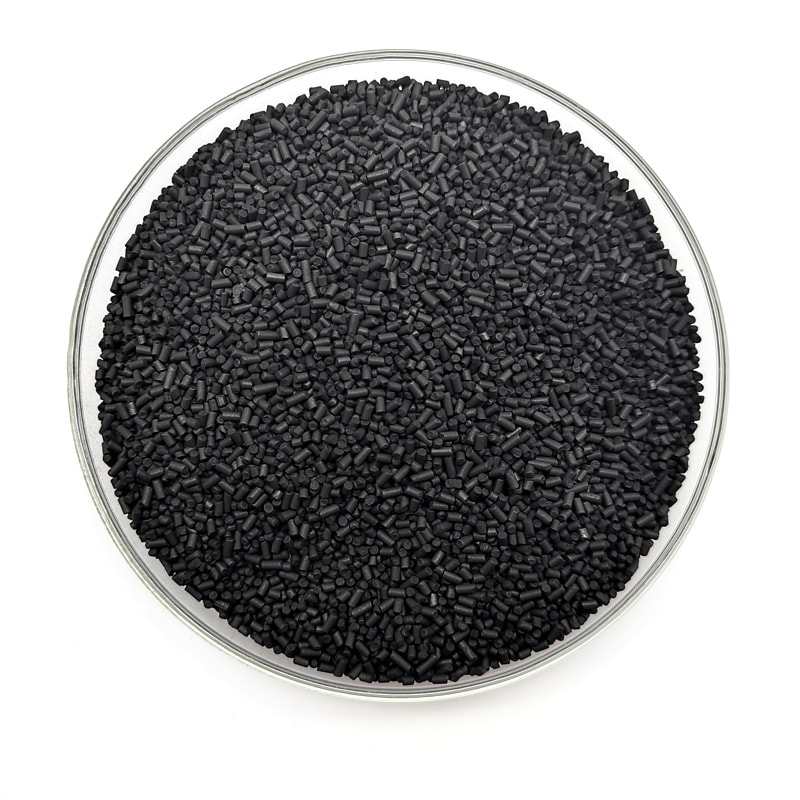
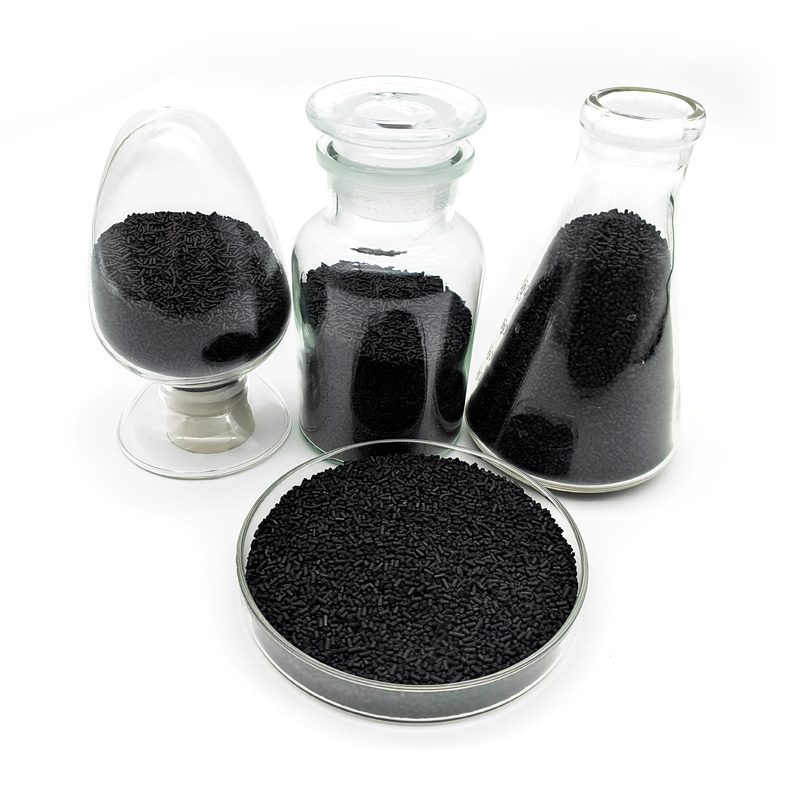
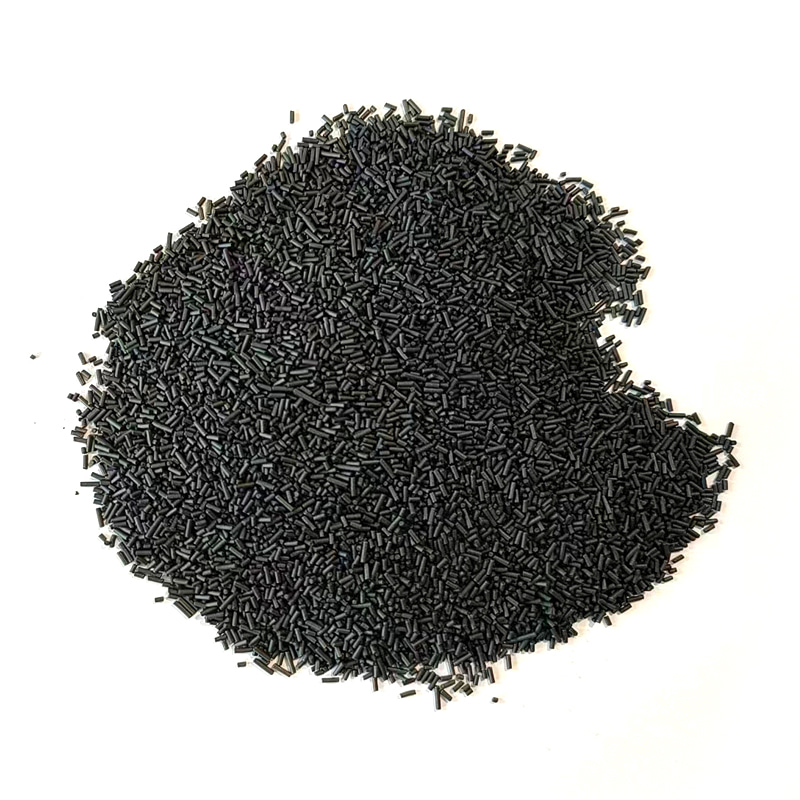
Carbon molecular sieve (CMS) is a specialized porous carbon adsorbent used in pressure swing adsorption (PSA) nitrogen generators. Its primary function is to separate oxygen and nitrogen from compressed air by preferentially adsorbing oxygen, carbon dioxide, moisture, and other more easily diffused components while allowing nitrogen to pass through as the product gas. The performance of a PSA nitrogen generator depends heavily on the quality, pore structure, mechanical strength, and consistency of the CMS filling its adsorption towers.
Modern nitrogen applications require reliable gas purity, stable production, low operating costs, and long adsorbent service life. Carbon molecular sieve models such as CMS-240, CMS-260, CMS-280, and CMS-330 are designed for different combinations of nitrogen purity and production capacity. By selecting the appropriate grade and operating the PSA system under suitable conditions, users can produce nitrogen for chemical processing, electronics, food packaging, pharmaceuticals, metal treatment, oil and gas operations, cable manufacturing, coal applications, transportation, and storage.
Anhui Zhuoxu New Material Technology Co., Ltd. supplies carbon molecular sieve for PSA nitrogen generators and provides several grades intended for industrial nitrogen production. The company combines porous carbon material production, continuous manufacturing equipment, product testing, research cooperation, and nitrogen equipment application experience. This integrated approach helps connect adsorbent properties with actual generator performance rather than evaluating the CMS only through isolated laboratory indicators.
What Is Carbon Molecular Sieve?
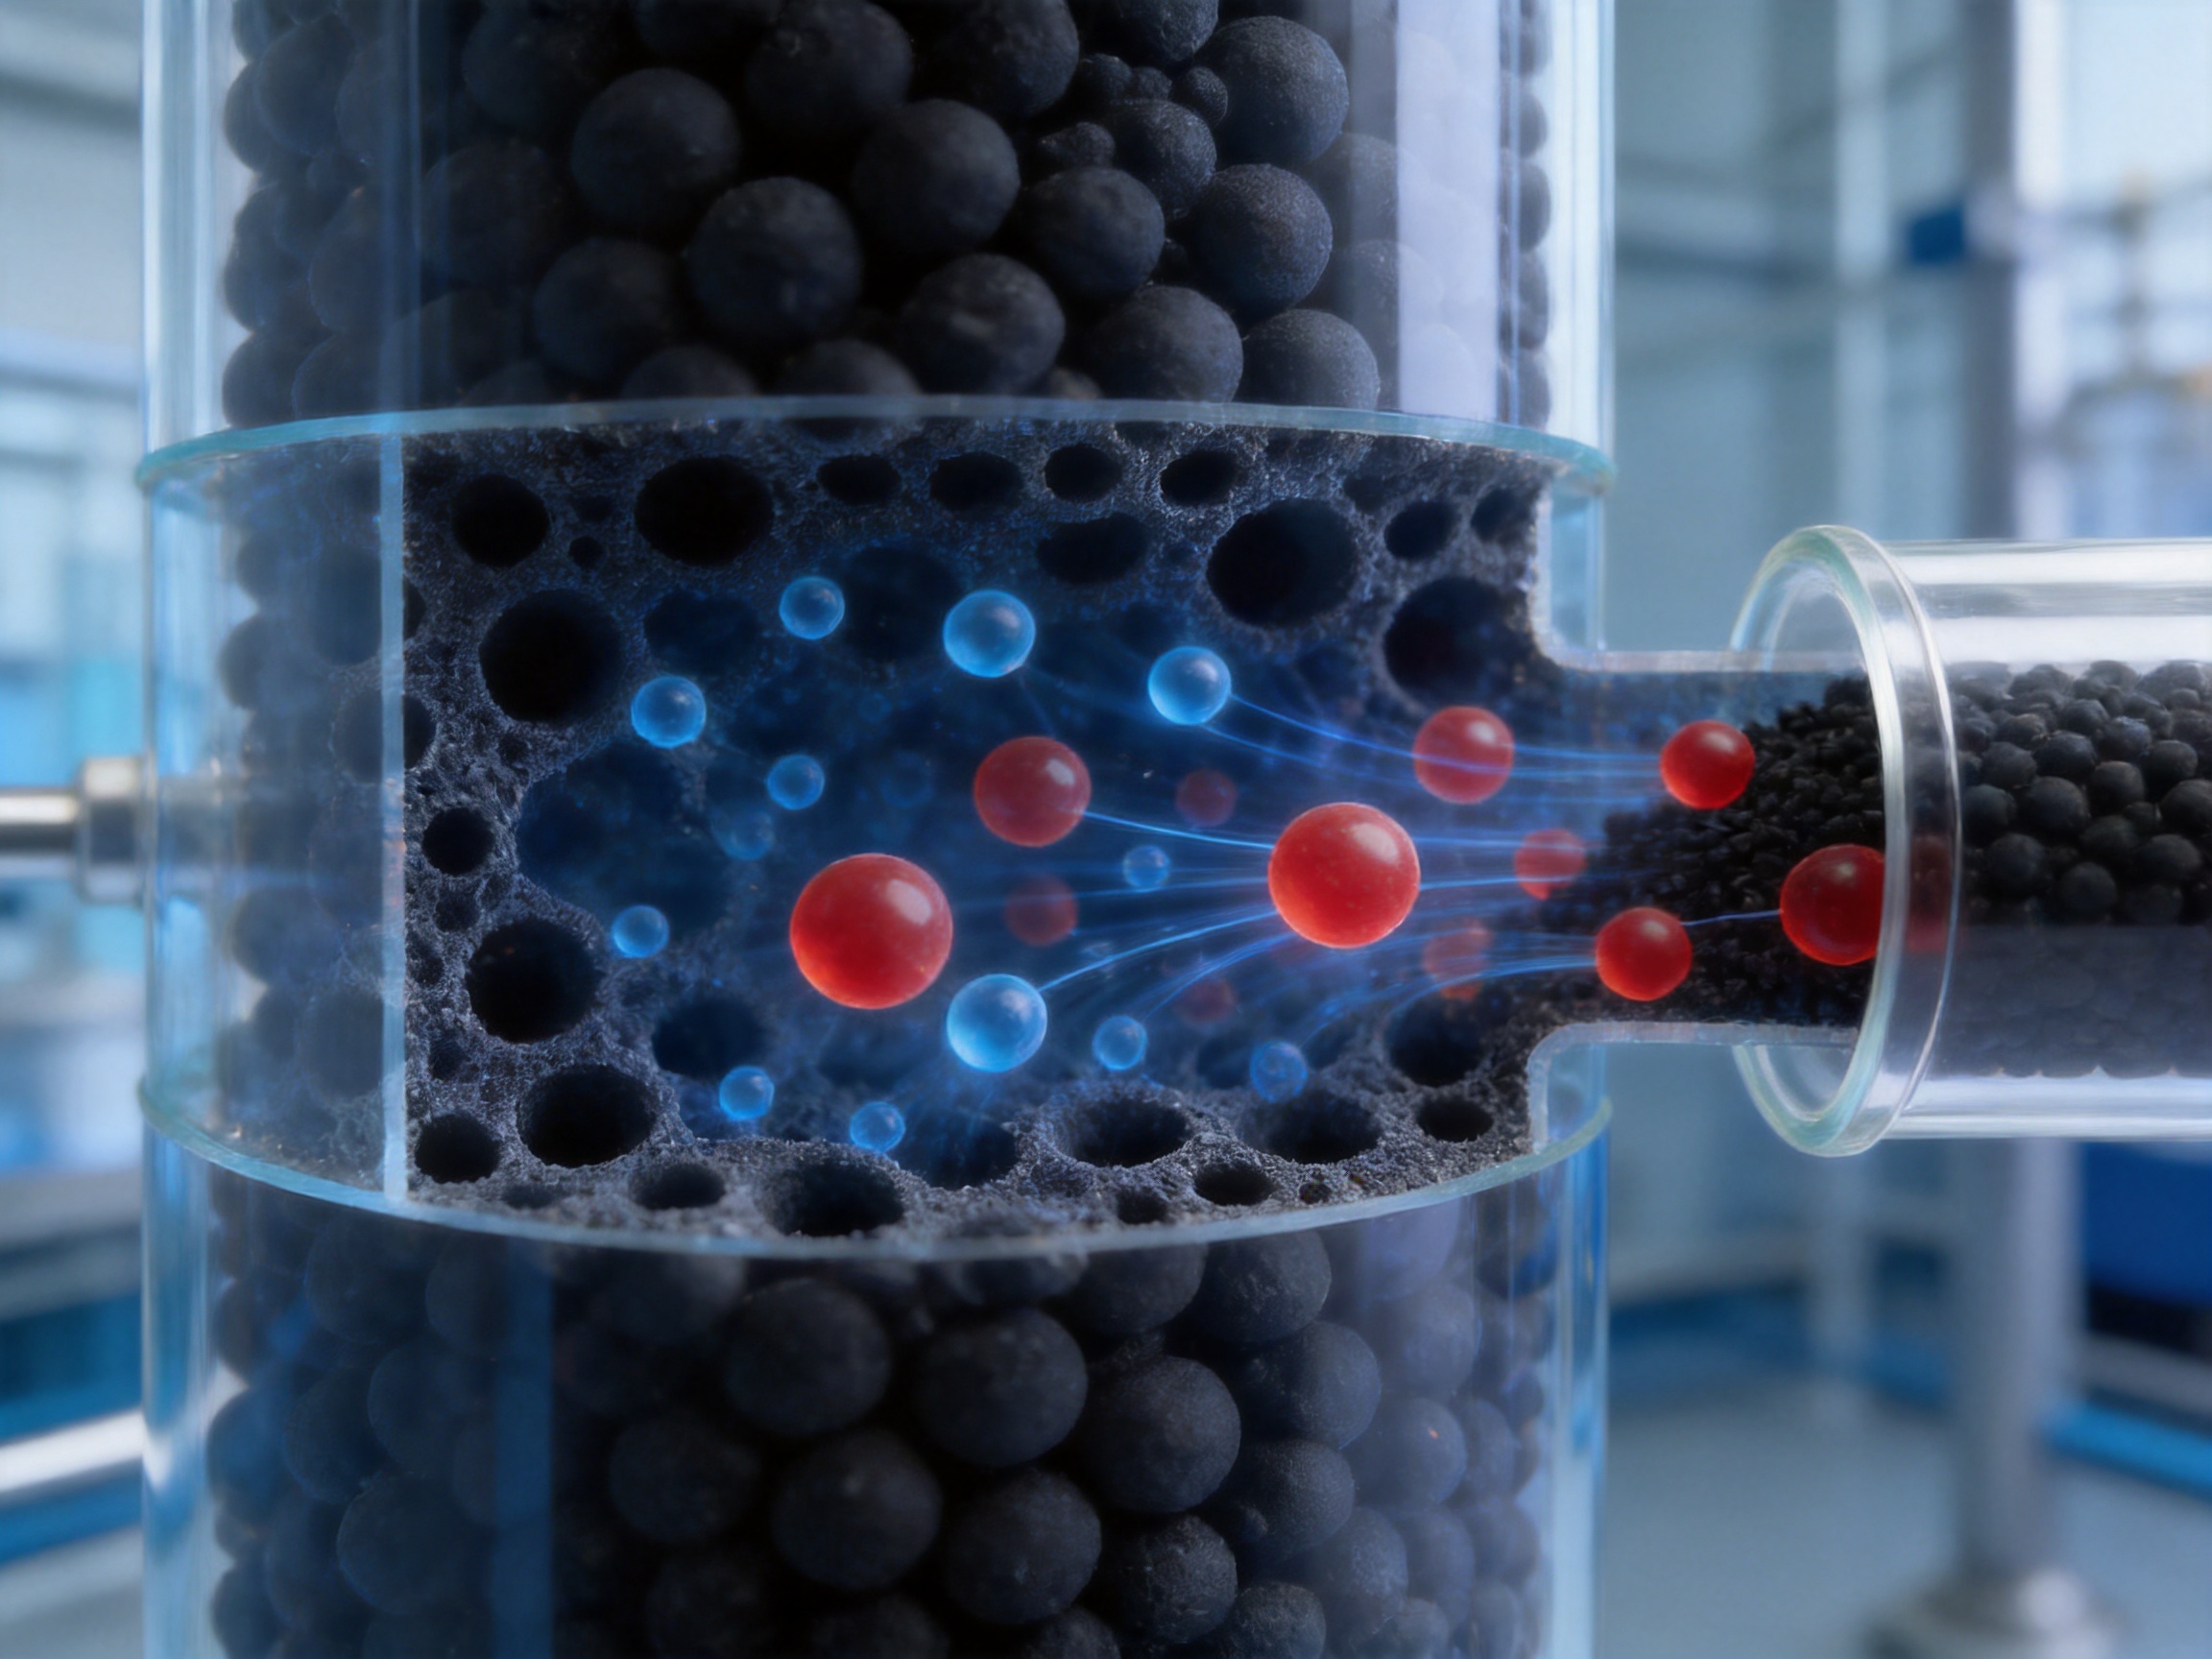
Carbon molecular sieve is a carbon-based adsorbent containing a highly developed network of micropores. These pores are engineered to create differences in the adsorption and diffusion rates of gases. In air separation, oxygen molecules diffuse into the micropores more rapidly than nitrogen molecules. As a result, oxygen is preferentially retained by the CMS, while nitrogen passes through the adsorption bed and is collected as product gas.
The selective separation mechanism is not based simply on the molecular size of oxygen and nitrogen. It also depends on pore-mouth dimensions, pore distribution, surface chemistry, adsorption kinetics, pressure, temperature, particle shape, and the time available for gas diffusion. A high-quality CMS must therefore provide a carefully controlled pore structure instead of merely having a large total surface area.
Typical effective micropore dimensions for oxygen-nitrogen separation are approximately 0.28 to 0.38 nanometers. Within this range, the pore network can create the desired kinetic separation. Oxygen enters and is adsorbed in the micropores comparatively quickly, while nitrogen diffusion is slower. During the adsorption step, nitrogen leaves the tower as the product gas. During regeneration, pressure is reduced and the adsorbed gases are released from the CMS.
The term “molecular sieve” refers to the material’s ability to discriminate between different molecules. Carbon molecular sieve differs from zeolite molecular sieve in composition and separation behavior. CMS is particularly well established for PSA nitrogen generation because its adsorption kinetics can be tailored for oxygen-nitrogen separation and because it can deliver high nitrogen productivity in compact systems.
How CMS Works in a PSA Nitrogen Generator
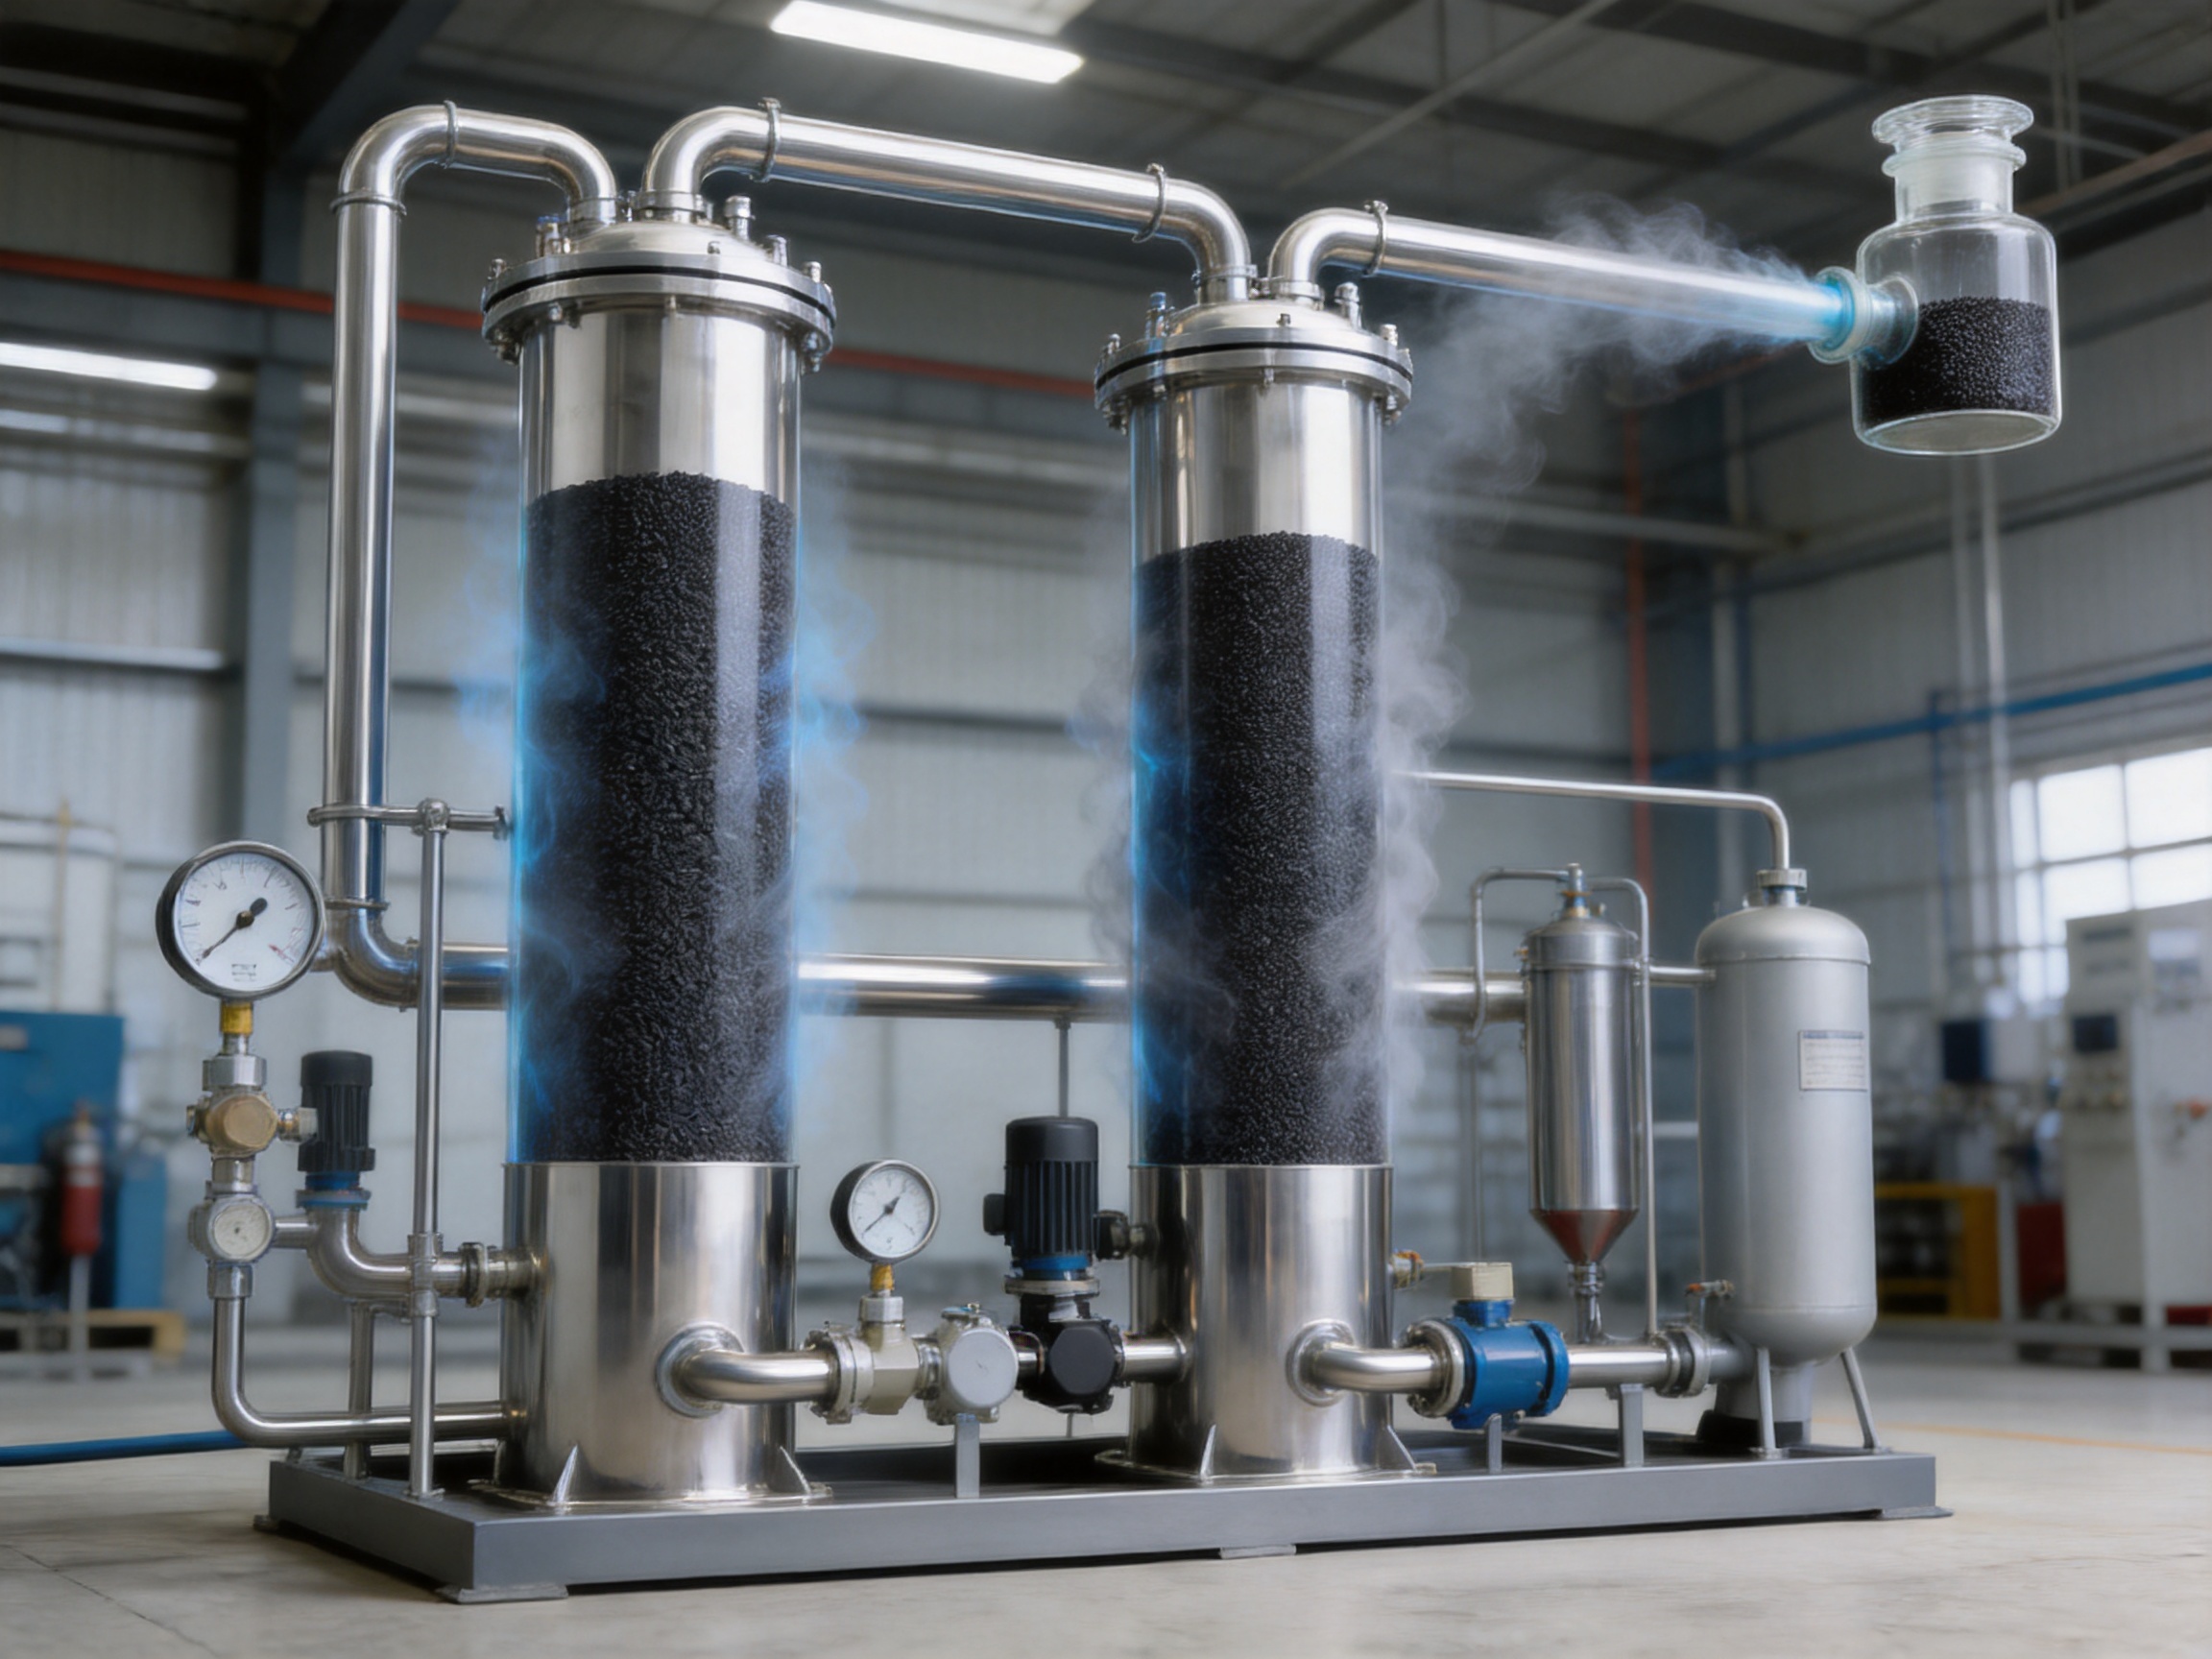
A PSA nitrogen generator normally contains two or more adsorption towers filled with carbon molecular sieve. While one tower is producing nitrogen, another tower is being depressurized and regenerated. Automatic valves alternate the towers through adsorption, pressure equalization, blowdown, purge, and repressurization steps. This cyclic process allows the generator to provide a continuous nitrogen supply.
Adsorption Stage
Compressed and purified air enters an adsorption tower at elevated pressure. Oxygen, carbon dioxide, residual water vapor, and certain trace impurities are preferentially adsorbed by the CMS. Nitrogen, which is less strongly retained under the selected operating conditions, passes through the bed and exits as product gas.
The adsorption time must be carefully controlled. If the cycle is too long, the mass-transfer zone may move through the bed and oxygen concentration in the product can rise. If the cycle is too short, the CMS capacity is not fully used and the system may require excessive valve switching or a larger quantity of adsorbent. The correct cycle depends on the CMS grade, tower dimensions, air pressure, product purity, and required flow rate.
Regeneration Stage
Once the CMS in a tower approaches its working adsorption capacity, the tower is depressurized. The reduction in pressure lowers the loading of adsorbed gases and releases oxygen and other retained components. In many nitrogen generators, regeneration occurs close to atmospheric pressure. A portion of product nitrogen may be used to purge the regenerated bed and improve desorption.
Regeneration quality has a direct effect on the next adsorption cycle. Incomplete regeneration leaves residual oxygen in the CMS, reducing available adsorption capacity and potentially lowering nitrogen purity. Proper regeneration also contributes to stable long-term operation and helps prevent the gradual accumulation of contaminants.
Pressure Equalization
Pressure equalization transfers gas from a tower completing adsorption into another tower that is being regenerated or repressurized. This process can recover part of the compressed gas energy and reduce pressure fluctuations. It can also reduce mechanical stress on the adsorbent bed when properly designed.
The supplied technical information recommends a pressure equalization period of approximately one to three seconds as a general reference. The actual setting should be established through commissioning and adjusted according to tower volume, valve response, system pressure, CMS loading, and desired energy efficiency.
Product Nitrogen Control
Nitrogen purity and production capacity are normally inversely related. When the user requires higher purity, the generator may need a lower product flow, a longer adsorption period, a larger CMS bed, increased purge, or a different cycle configuration. When lower purity is acceptable, the system can usually produce more nitrogen from the same adsorbent volume.
This operating flexibility allows users to select a practical balance between nitrogen quality and cost. For example, high-purity nitrogen may be required for electronics or sensitive pharmaceutical processes, while a lower purity level may be adequate for inerting, food storage, metal heat treatment, or certain oil and gas applications.
Carbon Molecular Sieve (CMS)
Principal Advantages of Carbon Molecular Sieve
Selective Oxygen-Nitrogen Separation
The most important advantage of CMS is its selective adsorption behavior. A properly manufactured carbon molecular sieve has a controlled micropore structure that promotes rapid oxygen diffusion while restricting nitrogen diffusion. This creates a strong kinetic separation effect, which is essential for producing nitrogen at commercially useful rates.
Uniform pore dimensions are especially important. If the pores are too large, nitrogen may diffuse too quickly and the separation factor can decline. If the pores are too small or poorly connected, oxygen diffusion may become too slow, reducing productivity. Consistent pore engineering helps the material maintain a useful balance between purity, capacity, and cycle speed.
High Adsorption Capacity
Carbon molecular sieve can retain significant quantities of target gas components even when their concentrations are relatively low. Its adsorption capacity remains useful across the temperature range encountered in industrial PSA operation. This is valuable because compressed air becomes warm after compression, and adsorption conditions are not always ideal.
High working capacity means that a reasonable volume of CMS can support a substantial nitrogen flow. It may also allow equipment manufacturers to design compact adsorption towers, reduce the footprint of nitrogen generators, and lower the amount of adsorbent required for a specified output.
Fast Nitrogen Production
CMS is well suited to cyclic PSA operation because oxygen adsorption and desorption can occur rapidly. Fast kinetics support shorter cycles and high productivity. A fast cycle can increase the amount of nitrogen generated per unit of adsorbent, provided that the tower, valves, controls, and air-treatment equipment are correctly matched.
Rapid operation must not be confused with uncontrolled operation. Excessively short cycles may increase pressure shocks, valve wear, bed movement, dust generation, and incomplete regeneration. The best performance comes from matching the CMS characteristics to a stable cycle design.
Cost-Effective Nitrogen Production
PSA nitrogen generation generally avoids the need for cryogenic air separation when the required nitrogen flow and purity fall within the practical range of PSA technology. A PSA system can be installed near the point of use, reducing dependence on delivered liquid or compressed nitrogen. This may lower logistics costs, reduce cylinder handling, and improve supply security.
CMS contributes to this cost advantage by providing a reusable adsorption medium. Instead of being consumed during normal operation, it is repeatedly regenerated. The main economic factors are CMS working capacity, service life, pressure requirements, purge consumption, compressor efficiency, maintenance, and the value of nitrogen produced.
Broad Industrial Applicability
Carbon molecular sieve nitrogen generators can serve many industries. In chemical plants, nitrogen is used for blanketing, inerting, purging, and preventing oxidation. In the oil and gas sector, nitrogen can support pipeline purging, tank inerting, well services, and process safety operations.
Electronics manufacturers often use nitrogen to limit oxidation and contamination during production. Food companies use nitrogen for modified-atmosphere packaging and storage. Pharmaceutical facilities use nitrogen in controlled environments and for protecting sensitive products. Metal heat-treatment operations use nitrogen atmospheres to reduce oxidation, decarburization, or unwanted chemical reactions.
CMS-based nitrogen systems are also used in coal handling, cable production, transportation, warehousing, and other applications where an inert atmosphere or oxygen reduction is required. The appropriate nitrogen specification depends on the application’s safety, process, purity, pressure, and flow requirements.
Available CMS Grades and Performance Selection
The CMS-240, CMS-260, CMS-280, and CMS-330 grades are designed to provide different nitrogen production levels and air consumption ratios. The model number is used as a product designation rather than a direct guarantee of performance in every generator. Actual output depends on the equipment design, operating pressure, cycle time, air pretreatment, tower dimensions, and required nitrogen purity.
| Model | Adsorption Pressure | Nitrogen Purity | Nitrogen Production Rate | Air-to-Nitrogen Ratio |
| CMS-240 | 0.75–0.80 MPa | 99.999% | 70 | 6.5 |
| CMS-240 | 0.75–0.80 MPa | 99.99% | 110 | 4.6 |
| CMS-240 | 0.75–0.80 MPa | 99.9% | 165 | 3.6 |
| CMS-240 | 0.75–0.80 MPa | 99.5% | 240 | 2.6 |
| CMS-240 | 0.75–0.80 MPa | 99% | 290 | 2.3 |
| CMS-260 | 0.75–0.80 MPa | 99.999% | 80 | 6.4 |
| CMS-260 | 0.75–0.80 MPa | 99.99% | 120 | 4.5 |
| CMS-260 | 0.75–0.80 MPa | 99.9% | 175 | 3.5 |
| CMS-260 | 0.75–0.80 MPa | 99.5% | 260 | 2.5 |
| CMS-260 | 0.75–0.80 MPa | 99% | 305 | 2.2 |
| CMS-280 | 0.75–0.80 MPa | 99.999% | 90 | 6.2 |
| CMS-280 | 0.75–0.80 MPa | 99.99% | 135 | 4.2 |
| CMS-280 | 0.75–0.80 MPa | 99.9% | 195 | 3.3 |
| CMS-280 | 0.75–0.80 MPa | 99.5% | 280 | 2.3 |
| CMS-280 | 0.75–0.80 MPa | 99% | 335 | 1.9 |
| CMS-330 | 0.75–0.80 MPa | 99.999% | 100 | 6.2 |
| CMS-330 | 0.75–0.80 MPa | 99.99% | 170 | 4.0 |
| CMS-330 | 0.75–0.80 MPa | 99.9% | 250 | 3.3 |
| CMS-330 | 0.75–0.80 MPa | 99.5% | 330 | 2.3 |
| CMS-330 | 0.75–0.80 MPa | 99% | 360 | 1.9 |
The production-rate figures in the supplied data are presented as nitrogen production rate values for the corresponding model and purity level. Equipment manufacturers and end users should confirm the precise unit convention, commonly expressed as normal cubic meters per hour per tonne of CMS or a related reference basis, before using the figures for final equipment sizing.
CMS-240 may be selected for systems requiring a balance between standard purity and economical operation. CMS-260 provides a higher stated production rate at comparable purity levels. CMS-280 is suitable for applications seeking stronger productivity and improved air utilization. CMS-330 provides the highest stated production figures among the listed grades, particularly at 99.5% and 99.9% nitrogen purity.
The correct model should not be selected solely by choosing the grade with the highest nominal production. A system producing high-purity nitrogen may achieve a lower flow than a system producing 99% nitrogen. Users should consider the complete operating target, including nitrogen flow, purity, pressure, duty cycle, compressor capacity, energy cost, and acceptable product loss.
Manufacturing Strengths and Process Control
Integrated Porous Carbon Material Supply
Anhui Zhuoxu New Material Technology Co., Ltd. is a wholly owned subsidiary of Huiya Group and operates in the porous carbon material sector. The company reports an annual production capacity of approximately 4,000 tons of porous carbon materials, together with a production base serving air separation and related porous-material applications.
Control over the principal carbon material supply can reduce dependence on multiple intermediaries. It also supports more consistent raw material specifications, which is important because precursor composition and structure influence carbonization behavior, pore development, strength, and adsorption kinetics.
For CMS manufacturers, raw material consistency is a central competitive factor. Variations in ash content, volatile components, particle structure, moisture, or precursor chemistry can produce differences in the final molecular sieve. An integrated material chain gives the manufacturer greater opportunity to monitor these variables before they affect the finished product.
Specialized Carbon-Based Formulation
The manufacturing program uses a dedicated carbon-based material system and a proprietary flower-mud base material associated with the group’s porous carbon technology. According to the supplied information, this approach is intended to improve production efficiency and increase the amount of finished CMS obtained from a given quantity of new carbon material.
While yield improvements are important for commercial competitiveness, the finished product must still meet performance requirements. Higher material yield is valuable only when the resulting CMS retains appropriate pore distribution, adsorption kinetics, crush strength, attrition resistance, and low dust generation. The company’s approach therefore links formulation development with performance testing.
Continuous Production Equipment
Continuous production equipment is used to reduce direct labor requirements and limit the effect of individual operator differences. Compared with highly manual production, continuous processing can improve repeatability in mixing, forming, drying, carbonization, activation, screening, and packaging when the equipment is properly calibrated and maintained.
Continuous manufacturing can also support more stable process temperatures and residence times. These factors are important for carbon molecular sieve because small variations in thermal treatment may alter pore-mouth size and adsorption selectivity. Process automation helps create more uniform batches and makes production data easier to record and analyze.
Low-Humidity Production Conditions
The production base is located in northern China, where the company identifies relatively low atmospheric humidity as a favorable condition for CMS production. Moisture control is significant because water can occupy adsorption sites, interfere with processing, and influence the final moisture content of the product.
A controlled drying and packaging process remains necessary regardless of climate. CMS should be protected from ambient moisture after manufacture, during storage, and before loading into the nitrogen generator. Proper packaging and warehouse handling help preserve the adsorbent’s initial performance.
Research and Development Cooperation
The company reports cooperation with Jinan Shengquan Group and China University of Mining and Technology in the research and development of carbon materials and carbon molecular sieve performance. Cooperation with external industrial and academic organizations can support material characterization, process optimization, application testing, and product iteration.
Research into CMS should consider both material-level and equipment-level behavior. A sample may show strong adsorption in a laboratory test but perform differently in a full-size tower if particle size distribution, pressure drop, heat effects, regeneration, or cycle timing are not properly controlled. Application-oriented research is therefore particularly valuable for industrial adsorbents.
Application-Based Factory Testing
One of the stated quality procedures is testing the CMS in a nitrogen generator before shipment. This approach is more representative than relying only on isolated physical or chemical measurements. Generator testing can reveal whether the material achieves the expected nitrogen purity and production rate under actual PSA cycling conditions.
Application testing may also expose problems related to dust, bed settling, pressure drop, valve switching, heat release, and regeneration. When the product is tested in an operating generator, the manufacturer can compare material performance with the specified model grade and identify deviations before delivery.
The company reports that approximately 90% of its CMS production reaches CMS-280 or higher performance levels. This indicates a focus on producing higher-grade material, although buyers should request current test reports and confirm the definition of the stated grade under agreed testing conditions.
Important Raw Air Pretreatment Requirements
Carbon molecular sieve is durable under appropriate operating conditions, but it is not designed to compensate for contaminated compressed air. Oil vapor, liquid water, excessive moisture, particles, and organic contaminants can block micropores or change the adsorbent surface. Once contaminants enter the bed, regeneration may not fully restore the original performance.
Oil Removal
Oil-lubricated compressors can discharge oil vapor and aerosol particles. These contaminants may deposit inside the CMS bed and reduce oxygen adsorption capacity. A suitable aftercooler, water separator, coalescing filter, and oil-removal system should be installed before the adsorption towers.
The supplied operating guidance identifies an oil content target below approximately 0.3 parts per million. The actual specification should be confirmed according to the compressor design, filter manufacturer, nitrogen purity requirement, and relevant industry standards.
Moisture Control
Compressed air temperature rises during compression and may carry substantial water vapor. After cooling, liquid water can condense and must be removed. A dryer is generally needed to keep the feed air within the required dew-point range.
The supplied information gives a dew point below approximately minus 4 degrees Celsius as a general raw-air requirement. Some installations may require a substantially lower pressure dew point depending on ambient conditions, operating pressure, equipment design, and the sensitivity of the CMS. The most important principle is to prevent liquid water and excessive vapor loading from entering the adsorbent bed.
Particle and Organic Contaminant Removal
Dust and mechanical particles can increase pressure drop, damage valves, and create channels through the adsorbent bed. Organic vapors may be more difficult to remove and can permanently reduce adsorption performance. Multi-stage filtration and regular filter replacement should therefore be included in the maintenance plan.
Air pretreatment is not an optional accessory. It is part of the CMS protection system and has a direct effect on adsorbent service life. In many cases, a relatively small investment in filtration and drying prevents a much larger cost associated with premature CMS replacement.
Operating Conditions for Stable CMS Performance
Adsorption Pressure
Higher adsorption pressure generally increases the amount of gas that can be adsorbed. However, higher pressure also increases compressor energy consumption and may increase the cost and complexity of the pressure vessel, valves, and piping. The supplied guidance recommends an adsorption pressure of approximately 0.6 to 0.8 MPa for a typical atmospheric-pressure regeneration process, while the product performance table lists 0.75 to 0.80 MPa.
The actual pressure should be selected through a complete energy and capacity analysis. A higher pressure is not automatically more economical if the additional nitrogen production is smaller than the increase in compressor power. Pressure should also remain within the certified operating limits of the adsorption tower and associated equipment.
Operating Temperature
Adsorption is generally exothermic. As gas is adsorbed, heat is released and the bed temperature may rise. Higher temperature commonly reduces adsorption capacity, which can affect nitrogen purity and production rate. The supplied guidance identifies an ambient temperature of 15 degrees Celsius or below as favorable for nitrogen generator performance.
In practice, the compressor aftercooler, receiver, ventilation system, and site environment all influence the air temperature entering the CMS. Stable cooling conditions help prevent seasonal fluctuations in nitrogen output. If the feed air is too warm, the system may require a longer cycle, a lower product flow, additional CMS, or a revised control strategy.
Pressure Equalization Time
Pressure equalization is a short but important stage in the PSA cycle. A general equalization time of one to three seconds is identified in the operating guidance. The correct value depends on pipe diameter, valve speed, tower volume, pressure difference, and the amount of gas exchanged.
If equalization is too aggressive, the bed may experience unnecessary mechanical movement or pressure shock. If it is too slow or poorly controlled, potential energy recovery may be lost. Proper valve sequencing and controller tuning are required to obtain the benefits of equalization.
Bed Loading and Mechanical Protection
CMS particles must be loaded evenly and supported by suitable screens, grids, and inert layers where required. Uneven loading can create preferential flow paths, causing some parts of the bed to be underused while other areas become overloaded. Mechanical vibration and repeated pressure changes can also cause particle movement.
Bed protection measures should minimize attrition and dust. The tower should be designed to prevent excessive fluidization, and the start-up and shutdown sequence should avoid sudden pressure surges. These precautions help preserve particle size distribution and maintain stable pressure drop.
How the Product Compares with Less Specialized Alternatives
Carbon molecular sieve offers several advantages over general-purpose activated carbon when the objective is oxygen-nitrogen separation. Standard activated carbon may provide broad adsorption capacity, but it does not necessarily have the pore-mouth control and diffusion selectivity required for efficient PSA nitrogen production. CMS is engineered specifically for kinetic gas separation.
Compared with poorly controlled or inconsistent carbon adsorbents, a specialized CMS can provide more predictable nitrogen purity, production rate, and cycle behavior. Uniform pore structure and controlled particle properties help reduce variation between batches. This consistency is particularly important for equipment manufacturers who need to reproduce generator performance across multiple installations.
CMS also offers advantages over nitrogen supply methods that depend entirely on cylinders or delivered liquid nitrogen when the user has a continuous, on-site requirement. On-site PSA generation can reduce transportation dependence and provide a flexible production rate. However, PSA is not the best solution for every application. Very large nitrogen demand, extremely high purity, or special pressure requirements may justify other technologies.
The competitive strength of a CMS supplier should therefore be evaluated across the complete value chain: raw material control, pore-structure design, manufacturing consistency, mechanical strength, application testing, technical support, and compatibility with the user’s generator. A low purchase price alone does not guarantee the lowest total cost of ownership.
Quality Control and Purchasing Considerations
Buyers should request a technical data sheet for the selected CMS grade and confirm the test conditions used to determine purity, production rate, pressure, temperature, air ratio, and service life. Performance values should be compared using the same reference conditions. Differences in cycle time, feed-air quality, nitrogen recovery, and purity measurement can create misleading comparisons.
Important purchasing parameters include particle diameter, bulk density, crush strength, attrition resistance, moisture content, dust content, adsorption performance, nitrogen productivity, packaging method, and recommended storage period. The buyer should also confirm the quantity required for each tower and whether the material is supplied in drums, bags, or another sealed package.
For a new nitrogen generator, CMS selection should be completed together with the equipment designer. The tower diameter, bed height, valve configuration, compressor capacity, product receiver volume, and control program must all be compatible with the selected adsorbent. For an existing generator, replacement CMS should be compared with the original material in terms of particle size and operating behavior to avoid pressure-drop or cycle-control problems.
Batch traceability is another important consideration. Each shipment should be associated with a production batch, test record, packaging date, and recommended storage conditions. Traceability allows the supplier and customer to investigate changes in nitrogen purity or production rate and supports consistent maintenance planning.
Storage, Handling, and Installation
Carbon molecular sieve should be kept sealed and dry before use. The packaging should remain intact until the material is ready to load. Open containers should not be left exposed to humid air because CMS can adsorb moisture before entering the PSA tower.
During installation, workers should avoid dropping bags or handling the material in a way that creates excessive dust. The adsorption tower should be clean, dry, and free from oil or loose particles. Screens and support layers should be inspected before loading. The CMS should be distributed evenly, and the final bed height should be recorded.
After loading, the system should be gradually pressurized and checked for leaks. Initial operation may require a conditioning period to stabilize moisture and remove residual air from the system. Nitrogen purity should be monitored until the product reaches the required specification.
During service, filters, dryers, valves, pressure sensors, oxygen analyzers, and control systems should be maintained according to the generator manufacturer’s schedule. A gradual decline in purity or output may indicate CMS aging, contamination, valve leakage, insufficient regeneration, compressor problems, or changes in operating temperature.
Applications of CMS Nitrogen Generation
Chemical and Petrochemical Processing
Nitrogen is commonly used to blanket storage tanks, purge pipelines, displace oxygen from process vessels, and protect reactive chemicals. CMS-based generators can provide nitrogen on demand at the location where it is needed, reducing reliance on transported gas.
Oil and Gas Operations
Oil and gas facilities use nitrogen for inerting, pressure maintenance, pipeline purging, equipment commissioning, and safety-related operations. The appropriate purity and flow depend on the process and hazard assessment. Reliable CMS performance helps maintain a stable nitrogen supply for continuous or intermittent operations.
Food Packaging and Storage
Nitrogen can displace oxygen in packaging and storage spaces, helping limit oxidation and preserve product quality. Food applications may require clean, dry, and appropriately certified nitrogen. The generator and air pretreatment system should be selected according to applicable hygiene and gas-quality requirements.
Electronics and Semiconductor-Related Processes
Electronics manufacturing often uses nitrogen to reduce oxidation and protect sensitive materials during soldering, assembly, heat treatment, or storage. These applications may require high purity and careful control of moisture and oxygen residuals. CMS-280 and CMS-330 may be considered where high purity and stable production are required, subject to application testing.
Pharmaceutical Manufacturing
Pharmaceutical processes can use nitrogen for blanketing, transfer, packaging, and protection of oxygen-sensitive products. The generator design should address cleanliness, validation, monitoring, and regulatory requirements. CMS performance is only one part of the complete gas-quality system.
Metal Heat Treatment
Nitrogen atmospheres can help reduce oxidation during heat treatment and protect metal surfaces. The required flow and purity vary according to furnace design, material, temperature, and process duration. A PSA generator can provide a practical on-site source for facilities with steady nitrogen consumption.
Cable, Coal, Transportation, and Warehousing
Other applications include cable manufacturing, coal storage, transportation, warehouse inerting, and product preservation. In these uses, nitrogen may be required to reduce oxygen concentration, prevent oxidation, limit fire risk, or protect stored materials. The required gas specification should be determined through a process and safety evaluation.
Advantages of an Integrated Supplier
An integrated CMS supplier can offer benefits beyond the supply of a bulk adsorbent. When the supplier understands raw carbon production, CMS processing, PSA equipment, and nitrogen application, it can provide more relevant technical recommendations. This may include model selection, purity-flow balancing, pretreatment requirements, cycle adjustment, and troubleshooting support.
Anhui Zhuoxu New Material Technology Co., Ltd. presents itself as a porous carbon material manufacturer, CMS supplier, and participant in nitrogen equipment services. Its reported 21 core patents and ISO 9001 certification indicate an emphasis on formalized development and quality management. Certification does not replace product testing, but it can provide a framework for documented production and process control.
The company’s broader development plan includes a second-phase porous carbon project with a reported annual capacity of 3,000 tons, focusing on silicon-carbon anode materials for new energy batteries and PSA applications. This cross-industry experience may support continued development of carbon structures, pore engineering, and high-performance porous materials.
The company reports that its products are sold in China and exported to Asia, South America, the Middle East, and Southeast Asia. International supply requires attention to packaging, documentation, shipping protection, local operating conditions, and technical communication. These factors are important when CMS is shipped over long distances or stored in humid climates.
Frequently Asked Questions
What is the main purpose of carbon molecular sieve?
The main purpose of CMS in a PSA nitrogen generator is to selectively adsorb oxygen from compressed air while allowing nitrogen to pass through as the product gas. It enables on-site nitrogen production through repeated adsorption and regeneration cycles.
How do CMS-240, CMS-260, CMS-280, and CMS-330 differ?
They are different CMS grades with different stated nitrogen production rates and air-to-nitrogen ratios at defined purity levels. CMS-330 has the highest listed production figures among the four grades, while CMS-240 represents the lower end of the listed performance range. The final selection must consider the complete generator design and operating target.
Does the highest CMS grade always provide the lowest operating cost?
No. A higher productivity grade may reduce the required adsorbent volume, but total operating cost also depends on compressor power, nitrogen recovery, purge consumption, pressure, cycle control, equipment cost, and service life. A grade should be selected through a total-cost analysis.
What purity levels can these CMS grades support?
The supplied performance table lists nitrogen purity levels from 99% to 99.999%, depending on the CMS model and operating conditions. Higher purity generally requires lower production capacity or greater adsorbent and energy consumption.
Why is compressed-air pretreatment important?
Oil vapor, liquid water, moisture, particles, and organic contaminants can block CMS micropores, reduce adsorption capacity, increase pressure drop, and shorten service life. Cooling, separation, filtration, oil removal, and drying should be installed before the CMS towers.
What adsorption pressure is recommended?
The supplied guidance identifies approximately 0.6 to 0.8 MPa as a general range for atmospheric-pressure regeneration, while the performance table uses 0.75 to 0.80 MPa. The correct pressure depends on the generator design and should be confirmed through application testing.
What temperature is suitable for PSA nitrogen generation?
Lower adsorption temperatures generally improve adsorption capacity. The supplied information identifies an ambient temperature of 15 degrees Celsius or below as favorable. Actual performance depends on feed-air temperature, cooling equipment, site conditions, and cycle configuration.
How long can carbon molecular sieve last?
Service life depends on air cleanliness, moisture control, pressure cycling, bed loading, mechanical stress, operating temperature, and regeneration quality. A supplier should provide a service-life estimate based on agreed operating conditions rather than a universal number.
Can CMS be used in an existing nitrogen generator?
It may be possible, but the replacement material should match the existing tower, particle size, bulk density, pressure drop, cycle, and control settings. Application testing and commissioning are recommended before full-scale replacement.
How should CMS be stored before use?
CMS should remain in sealed, moisture-resistant packaging in a dry warehouse. Containers should be opened only immediately before loading, and the adsorbent should be protected from liquid water, oil, dust, and humid ambient air.
What information should be provided when requesting a quotation?
Buyers should provide required nitrogen purity, flow rate, outlet pressure, operating hours, feed-air pressure, ambient temperature, compressor type, existing generator information, application, delivery location, and expected operating schedule. These details help the supplier recommend the correct grade and quantity.
Conclusion
Carbon molecular sieve is the core functional material in many PSA nitrogen generators. Its controlled micropore structure enables kinetic separation of oxygen and nitrogen, while its adsorption capacity, fast diffusion behavior, and reusability support economical on-site nitrogen production. CMS-240, CMS-260, CMS-280, and CMS-330 provide options for different combinations of purity, production rate, and air consumption.
The advantages of a CMS product should be evaluated through more than a single performance number. Raw material consistency, pore-structure control, mechanical strength, continuous manufacturing, moisture protection, batch traceability, and actual nitrogen-generator testing all influence practical results. Anhui Zhuoxu New Material Technology Co., Ltd. combines porous carbon production, specialized CMS processing, research cooperation, ISO 9001 quality management, and application-based testing to serve industrial nitrogen-generation requirements.
For the end user, the most reliable approach is to select the CMS grade together with the PSA equipment design. Proper air pretreatment, controlled adsorption pressure, suitable temperature, optimized equalization, careful bed loading, and regular maintenance are essential for realizing the material’s potential. When these conditions are managed correctly, carbon molecular sieve can provide a stable, flexible, and cost-effective source of nitrogen for a wide range of industrial applications.
References
1. Company-provided technical information for CMS-240, CMS-260, CMS-280, and CMS-330 carbon molecular sieve.
2. Company-provided information on porous carbon production capacity, manufacturing processes, research cooperation, patents, and ISO 9001 certification.
3. General principles of pressure swing adsorption and cyclic gas separation.
4. General engineering guidance for compressed-air filtration, drying, oil removal, and PSA nitrogen generator operation.
5. General industrial practice for adsorbent handling, adsorption-bed loading, regeneration, pressure equalization, and nitrogen purity control.
Product: Carbon Molecular Sieve (CMS)
 E-mail
anhuilisa@126.com
 Phone
+86 18603224420
 Address
No. 26 Kunshan Road, Xuanzhou Economic Development Zone, Liqiao Town, Xuanzhou District, Xuancheng City, Anhui Province, P.R.China
Copyright Anhui Zhuoxu New Material Technology Co., Ltd. All rights reserved.
 Carbon Molecular Sieve Manufacturer Carbon Molecular Sieve Supplier