 English
 中文简体
 русский
 Français
 Español
 عربى
 CONTACT US


Carbon Molecular Sieve for High-Efficiency PSA Nitrogen Generation
2026-11-08
Content
- 1 What Is Carbon Molecular Sieve?
- 2 Why CMS Performance Matters in Nitrogen Generators
- 3 Key Advantages of the CMS Product Range
- 4 Product Models and Typical Performance
- 5 Manufacturing Strengths and Quality Advantages
- 6 How CMS Works in a PSA Nitrogen Generator
- 7 Recommended Operating Conditions
- 8 Applications Across Major Industries
- 9 Choosing the Correct CMS Grade
- 10 Installation, Filling, and Maintenance
- 11 Competitive Advantages of the Product and Manufacturer
- 12 Frequently Asked Questions
- 12.1 What is the main function of CMS in a nitrogen generator?
- 12.2 What is the difference between CMS-240, CMS-260, CMS-280, and CMS-330?
- 12.3 Can CMS produce 99.999% nitrogen?
- 12.4 Does higher nitrogen purity reduce product flow?
- 12.5 Why must compressed air be dried before entering the CMS tower?
- 12.6 Why is oil removal important?
- 12.7 What adsorption pressure is recommended?
- 12.8 How long can CMS last?
- 12.9 Can CMS be used in an existing nitrogen generator?
- 12.10 How should CMS be stored?
- 12.11 What information should a buyer provide when requesting a quotation?
- 12.12 Are the listed production rates guaranteed for every generator?
- 13 Conclusion
- 14 References
- 15 Product: Carbon Molecular Sieve (CMS)
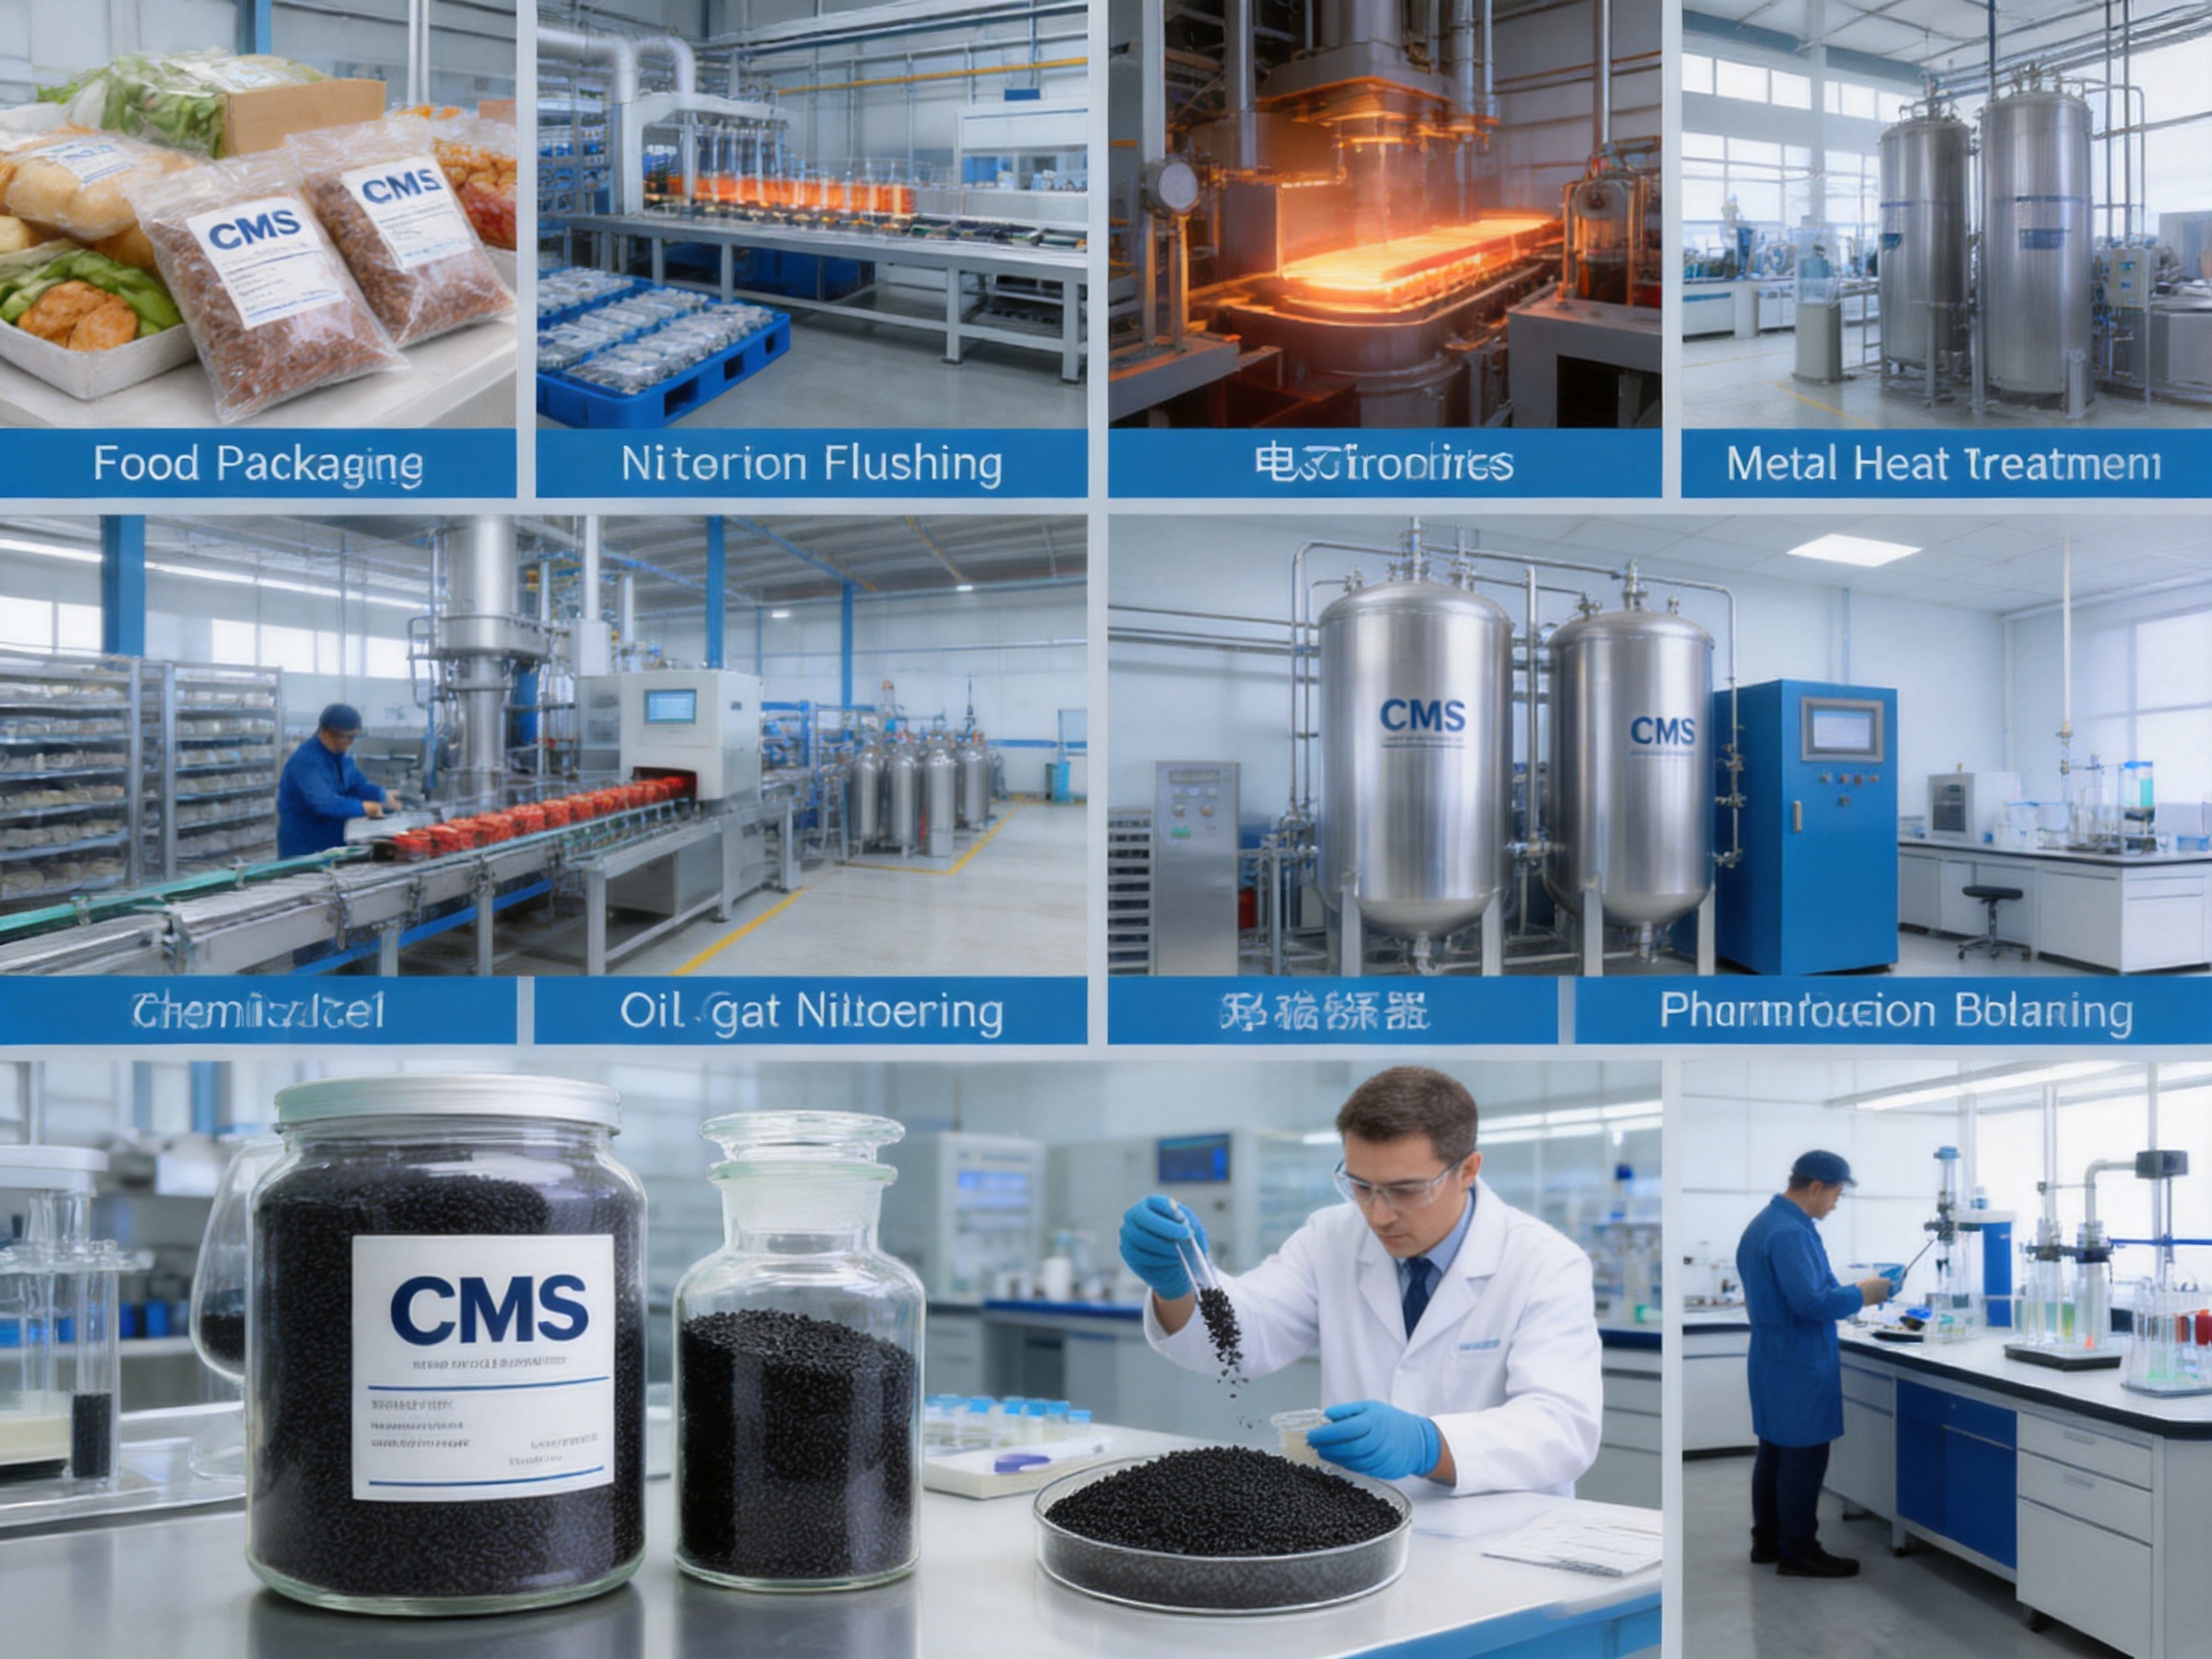
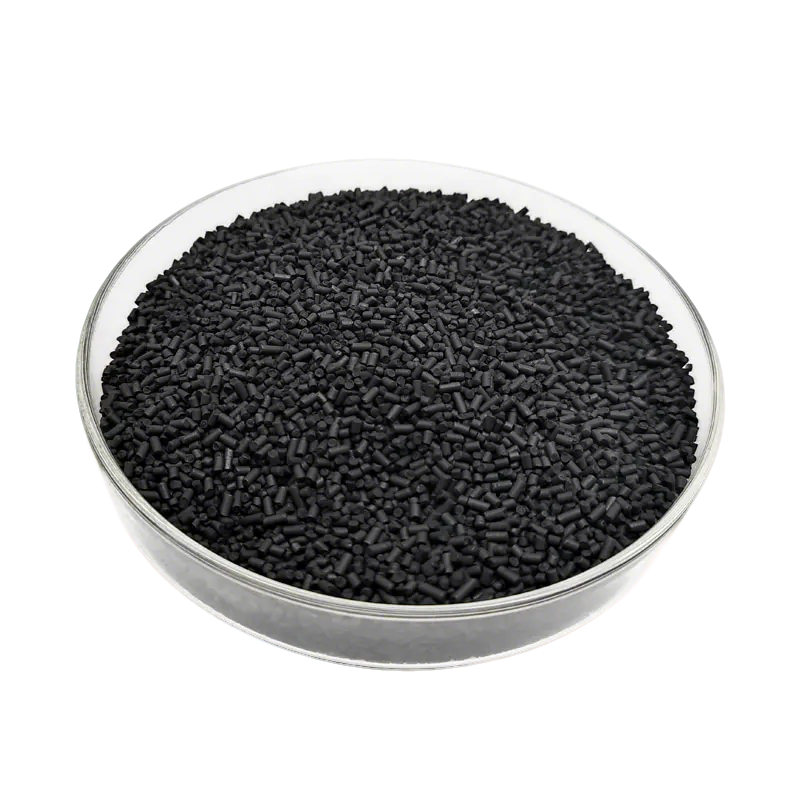
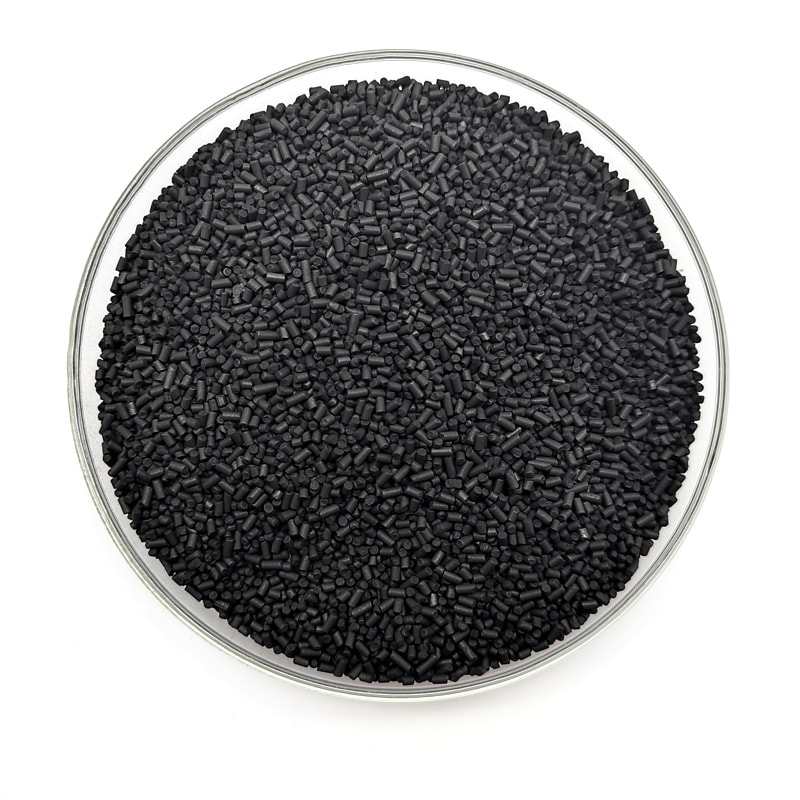
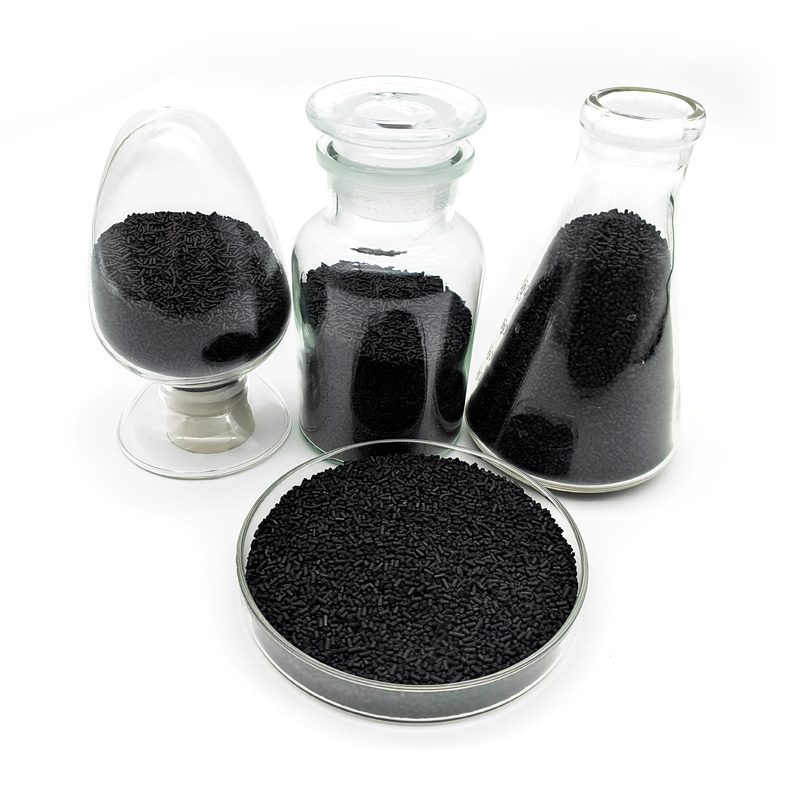
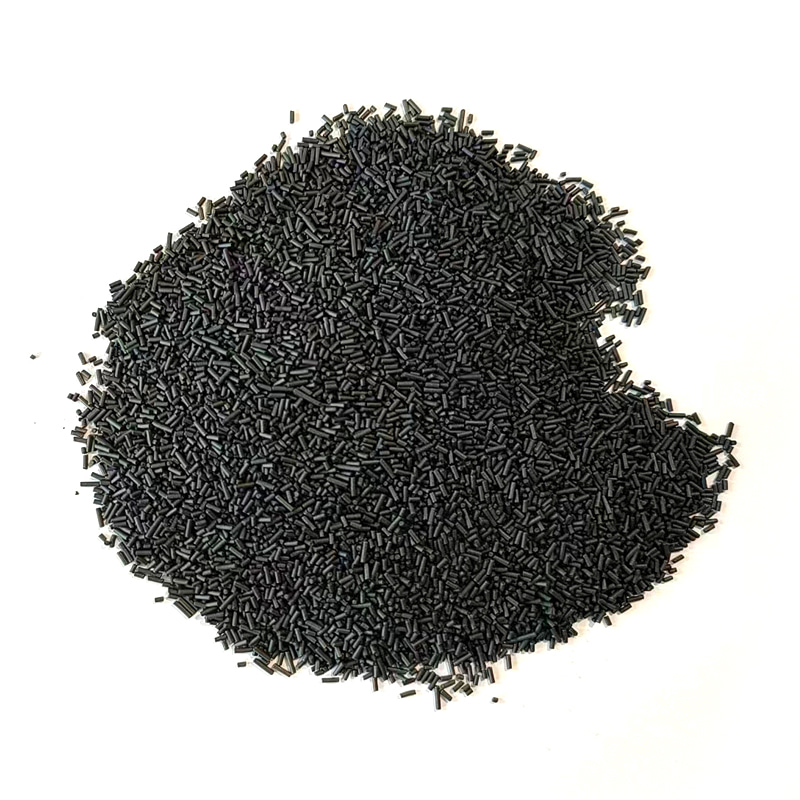
Carbon molecular sieve (CMS) is a specialized porous carbon adsorbent used to separate oxygen and nitrogen from compressed air. It is the central working material in pressure swing adsorption (PSA) nitrogen generators, where its carefully controlled microporous structure allows oxygen to be adsorbed more rapidly than nitrogen. This difference in adsorption and diffusion rates makes it possible to produce nitrogen with adjustable purity, stable flow, and comparatively low operating cost.
Modern nitrogen-generation systems require an adsorbent that can provide more than basic gas separation. The material must offer consistent pore structure, high mechanical strength, strong adsorption performance, low attrition, reliable regeneration, and compatibility with continuous industrial operation. CMS-240, CMS-260, CMS-280, and CMS-330 are designed for these requirements and provide different performance levels for nitrogen generators serving applications from general industrial protection to high-purity gas supply.
Manufactured by Anhui Zhuoxu New Material Technology Co., Ltd., a wholly owned subsidiary of Huiya Group, these carbon molecular sieve grades are supported by integrated porous-carbon production capabilities, dedicated carbon molecular sieve manufacturing, nitrogen-generator testing, research cooperation, and ISO 9001 quality management. Their production system is intended to improve raw-material consistency, reduce unnecessary intermediate costs, and provide customers with an adsorbent selected according to actual nitrogen purity and capacity requirements.
Carbon Molecular Sieve (CMS)
What Is Carbon Molecular Sieve?
Carbon molecular sieve is a carbon-based adsorbent containing an extensive network of micropores. Unlike conventional activated carbon, which is generally optimized for broad adsorption of many compounds, CMS is engineered to create a more selective difference between gas molecules. In air separation, the pore structure is adjusted so that oxygen molecules enter and diffuse through the micropores more readily than nitrogen molecules.
The effective pore size of a carbon molecular sieve used for nitrogen production is commonly within approximately 0.28 to 0.38 nanometers. This range is small enough to create a meaningful kinetic separation between oxygen and nitrogen while still allowing rapid oxygen adsorption under PSA operating conditions. The separation is therefore based primarily on differences in molecular diffusion rates rather than on a simple molecular-size exclusion mechanism.
During the adsorption stage, compressed air passes through a bed of CMS particles. Oxygen, moisture traces, carbon dioxide, and certain other components are preferentially retained by the adsorbent, while nitrogen passes through the bed as the product gas. When the bed approaches its adsorption capacity, the pressure is reduced and the adsorbed gases are released during regeneration. The adsorbent can then be reused in the next cycle.
A PSA nitrogen generator normally contains two or more adsorption towers. While one tower is producing nitrogen, another tower is being depressurized and regenerated. Alternating the towers creates a substantially continuous nitrogen supply. The performance of the complete system depends on the interaction of the adsorbent, air pretreatment equipment, valves, controls, pressure cycle, regeneration method, and product-gas requirements.
Why CMS Performance Matters in Nitrogen Generators
The quality of the carbon molecular sieve directly affects the main operating indicators of a PSA nitrogen generator. These indicators include nitrogen purity, nitrogen recovery, product flow, compressed-air consumption, pressure stability, cycle time, service life, and the frequency of adsorbent replacement.
A CMS with a uniform micropore distribution can provide a more predictable separation response. If the pore structure is inconsistent, some particles may adsorb oxygen too slowly while others become saturated too quickly. This can produce unstable outlet purity, higher air consumption, and uneven utilization of the adsorption bed.
Mechanical strength is equally important. The adsorbent is exposed to repeated pressurization, depressurization, gas velocity changes, vibration, and particle-to-particle contact. Excessive abrasion can generate dust, increase pressure drop, damage valves, contaminate downstream equipment, and reduce the effective adsorption capacity of the bed. A suitable CMS must therefore combine adsorption performance with adequate crushing strength and resistance to pulverization.
Thermal and moisture stability also influence performance. Adsorption is generally exothermic, meaning that the temperature of the bed can rise during operation. Higher temperature tends to reduce adsorption capacity. If water or oil enters the tower, it may occupy micropores or block access to the active carbon surface. Proper air pretreatment and an adsorbent with stable operating characteristics are therefore essential.
Key Advantages of the CMS Product Range
Efficient Oxygen-Nitrogen Separation
The primary advantage of CMS-240, CMS-260, CMS-280, and CMS-330 is their selective adsorption behavior in oxygen-nitrogen separation. The controlled micropore structure enables oxygen to diffuse into the carbon pores faster than nitrogen. This creates the adsorption selectivity needed for PSA nitrogen production.
Efficient separation can help a nitrogen generator reach its target purity with an appropriate amount of adsorbent and compressed air. It also allows users to balance nitrogen purity against gas production. In many industrial applications, extremely high purity is not necessary. A system may operate more economically at 99.5%, 99.9%, or 99.99% nitrogen purity than at 99.999%. CMS allows this operating point to be adjusted according to the process requirement.
Strong Adsorption Capacity
Carbon molecular sieve maintains useful adsorption capacity even when the concentration of a target gas component is relatively low. This is valuable because nitrogen generators must repeatedly remove oxygen from air under dynamic operating conditions. Strong adsorption supports a stable product stream and helps the adsorbent perform effectively across repeated PSA cycles.
The material also retains meaningful adsorption performance over a practical range of operating temperatures. Nevertheless, adsorption capacity normally declines as temperature rises. This is why cool, dry compressed air and effective aftercooling are important for achieving the best result. The CMS itself provides the separation function, while the supporting air-treatment system protects and enables that function.
Flexible Purity and Capacity
One of the most important practical benefits of CMS is flexibility. The nitrogen purity and product flow can be adjusted through changes in cycle time, feed-air quantity, adsorption pressure, product withdrawal, and the operating strategy of the generator. Higher purity generally requires more adsorbent utilization, a longer or more carefully controlled cycle, and a greater amount of compressed air per unit of nitrogen.
At a lower purity target, the same adsorbent bed may produce a greater nitrogen flow. This creates an opportunity to reduce the cost of nitrogen when the application only requires oxygen displacement, fire prevention, packaging protection, or general inerting. The user can select a suitable balance between purity, flow, and energy consumption rather than operating every system at the highest possible purity.
Cost-Effective PSA Operation
PSA nitrogen production has several advantages compared with the purchase and delivery of bottled or liquid nitrogen. Nitrogen is generated at the point of use, reducing dependence on deliveries, storage tanks, cylinder handling, and emergency replenishment. The process does not require cryogenic temperatures and can be started or stopped according to production demand.
The cost of nitrogen depends on electricity consumption, compressor efficiency, air pretreatment, maintenance, utilization of the adsorbent, and the required purity. A high-performing CMS can contribute to lower nitrogen cost by supporting efficient gas separation and stable operation. The final economic result, however, must always be evaluated together with the complete generator design and the actual operating conditions.
Broad Industrial Applicability
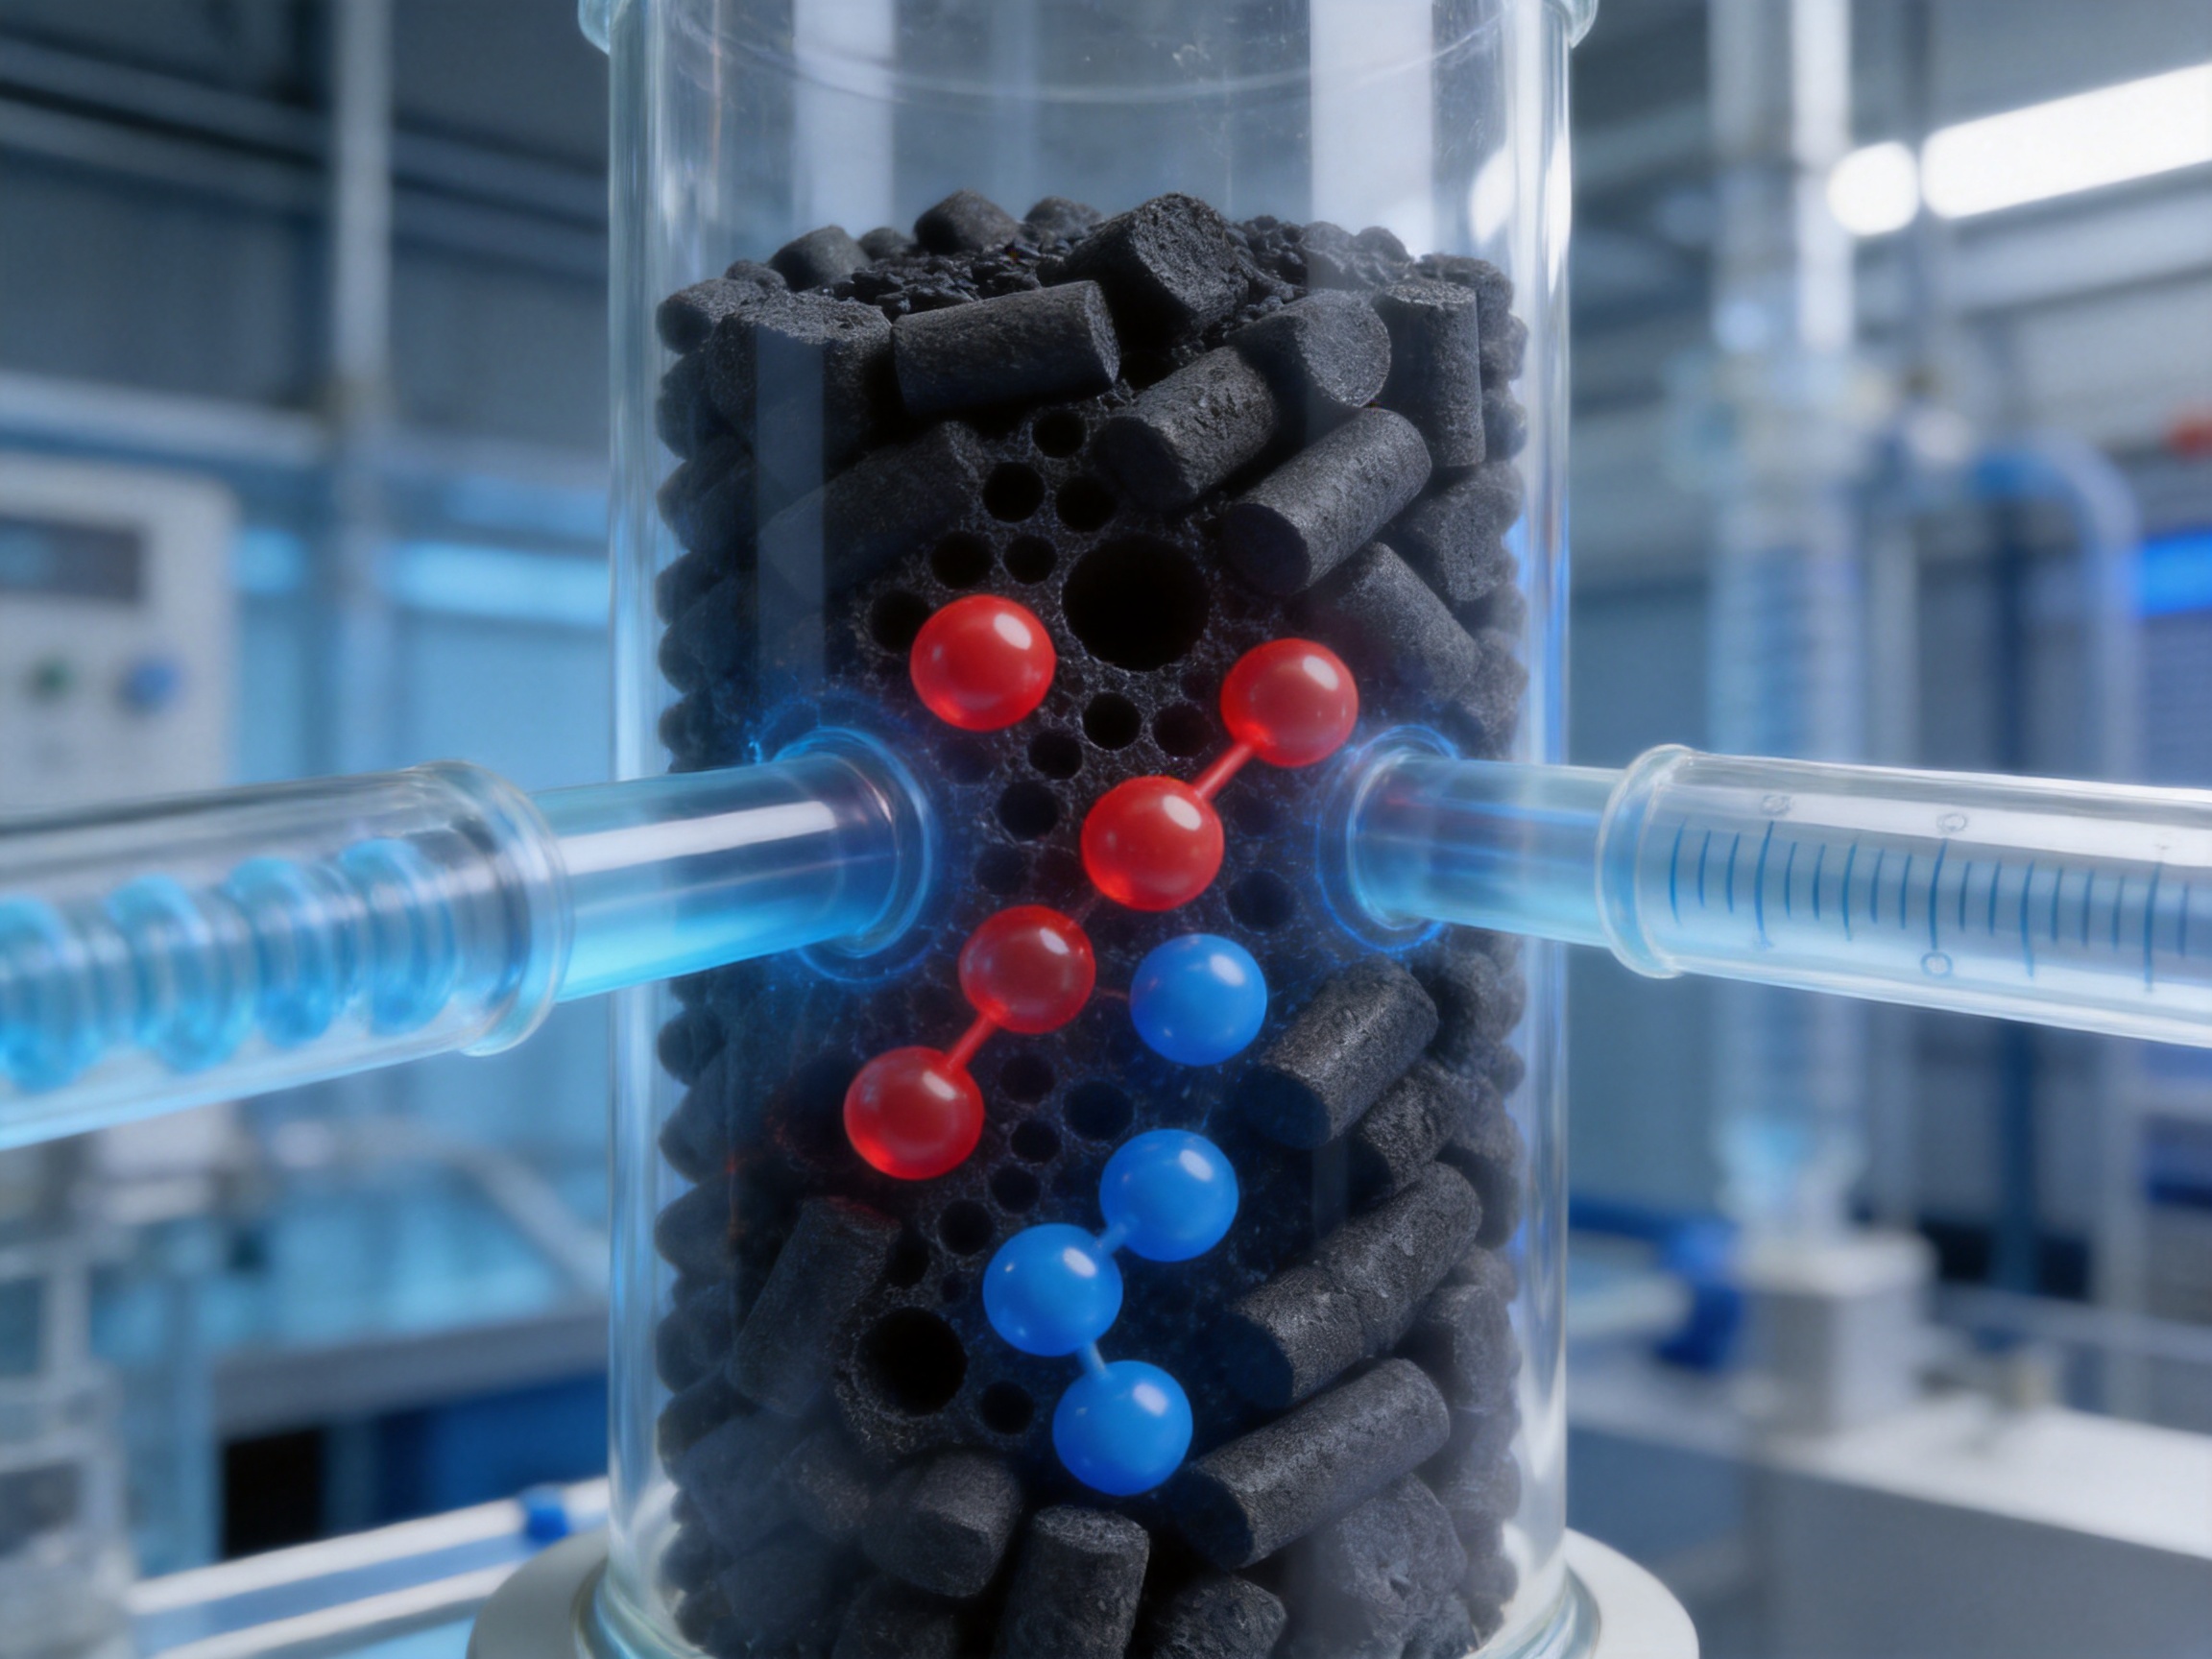
CMS nitrogen generators are used in chemical processing, oil and gas operations, electronics manufacturing, food packaging, coal handling, pharmaceuticals, cable production, metal heat treatment, transportation, storage, and many other industries.
In food packaging, nitrogen can displace oxygen and slow oxidation. In electronics manufacturing, high-purity nitrogen can protect sensitive materials and processes from oxygen and moisture. In metal heat treatment, nitrogen can provide an inert atmosphere. In oil and gas applications, nitrogen can be used for tank blanketing, pipeline purging, pressure maintenance, and equipment protection. In pharmaceutical production, nitrogen can help maintain controlled atmospheres when supported by appropriate purification and validation systems.
Product Models and Typical Performance
The product range includes CMS-240, CMS-260, CMS-280, and CMS-330. The model designation represents a product grade within the range and is associated with different nitrogen-generation performance levels. The data below summarizes the supplied typical performance information at an adsorption pressure of approximately 0.75 to 0.80 MPa.
Model |
Adsorption Pressure |
Nitrogen Purity |
Typical Nitrogen Production Rate |
Air-to-Nitrogen Ratio |
CMS-240 |
0.75–0.80 MPa |
99.999% |
70 |
6.5 |
CMS-240 |
0.75–0.80 MPa |
99.99% |
110 |
4.6 |
CMS-240 |
0.75–0.80 MPa |
99.9% |
165 |
3.6 |
CMS-240 |
0.75–0.80 MPa |
99.5% |
240 |
2.6 |
CMS-240 |
0.75–0.80 MPa |
99.0% |
290 |
2.3 |
CMS-260 |
0.75–0.80 MPa |
99.999% |
80 |
6.4 |
CMS-260 |
0.75–0.80 MPa |
99.99% |
120 |
4.5 |
CMS-260 |
0.75–0.80 MPa |
99.9% |
175 |
3.5 |
CMS-260 |
0.75–0.80 MPa |
99.5% |
260 |
2.5 |
CMS-260 |
0.75–0.80 MPa |
99.0% |
305 |
2.2 |
CMS-280 |
0.75–0.80 MPa |
99.999% |
90 |
6.2 |
CMS-280 |
0.75–0.80 MPa |
99.99% |
135 |
4.2 |
CMS-280 |
0.75–0.80 MPa |
99.9% |
195 |
3.3 |
CMS-280 |
0.75–0.80 MPa |
99.5% |
280 |
2.3 |
CMS-280 |
0.75–0.80 MPa |
99.0% |
335 |
1.9 |
CMS-330 |
0.75–0.80 MPa |
99.999% |
100 |
6.2 |
CMS-330 |
0.75–0.80 MPa |
99.99% |
170 |
4.0 |
CMS-330 |
0.75–0.80 MPa |
99.9% |
250 |
3.3 |
CMS-330 |
0.75–0.80 MPa |
99.5% |
330 |
2.3 |
CMS-330 |
0.75–0.80 MPa |
99.0% |
360 |
1.9 |
The production-rate figures should be treated as typical reference values rather than universal guarantees. Actual performance depends on tower dimensions, filling density, particle size, feed-air quality, pressure cycle, temperature, valve timing, nitrogen purity measurement, and generator design. Before selecting a grade, users should provide the required nitrogen flow, purity, pressure, operating hours, ambient conditions, and expected service life.
CMS-240
CMS-240 is suitable for nitrogen generators requiring a balance between standard PSA performance and controlled operating cost. It can support a wide range of nitrogen purities from approximately 99.0% to 99.999%, with the corresponding product flow changing according to the purity target. It may be considered for general industrial nitrogen, packaging, storage protection, and applications where the required flow is moderate.
CMS-260
CMS-260 provides a higher typical production rate than CMS-240 at corresponding purity levels in the supplied data. It can be used when a nitrogen generator requires additional capacity while maintaining a broad operating range. The grade may be appropriate for medium-scale industrial systems and applications where the balance between purity, flow, and air consumption is important.
CMS-280
CMS-280 is positioned as a higher-performance grade and is particularly relevant to systems requiring stronger nitrogen-generation output. At 99.999% purity, the typical production rate is listed as 90, while at lower purity levels the rate increases substantially. The manufacturer reports that approximately 90% of its CMS production reaches CMS-280 and above, indicating a focus on higher-grade product consistency.
CMS-330
CMS-330 is the highest grade listed in this product range. It is intended for applications that require high output and efficient nitrogen production across purity levels. The supplied data lists a typical production rate of 100 at 99.999% purity and up to 360 at 99.0% purity. It may be selected for demanding PSA systems, provided that the generator design and operating conditions are matched to the material.
Manufacturing Strengths and Quality Advantages
Integrated Raw-Material Supply
A major strength of the manufacturing system is the relationship between the porous-carbon material supply and the final CMS product. The company works with related raw-material suppliers and uses dedicated raw materials intended for carbon molecular sieve production. Greater control over the precursor can improve consistency in carbonization, pore development, activation, and final product performance.
Vertical or closely coordinated supply arrangements can also reduce unnecessary price differences caused by multiple intermediaries. Lower production costs can be passed to customers while maintaining attention to process control. For industrial buyers, this may support more predictable procurement and reduce the risk of quality variation between batches.
Specialized Carbon Material and Base Technology
The production process uses a specialized carbon-material base developed for carbon molecular sieve applications. The company states that its patented carbon molecular sieve base material can produce a greater quantity of finished CMS from the same amount of new carbon material compared with less efficient approaches. Improved material utilization can reduce waste, support competitive pricing, and contribute to more stable manufacturing economics.
The company’s broader porous-carbon technology includes Resin-Based Porous Carbon, or RHC, in which polymer resin is used as a precursor to create a stable hard-carbon structure through high-temperature carbonization. Although different applications may use different formulations and process parameters, this background in resin-derived porous carbon provides a technical foundation for controlling carbon structure and pore development.
Continuous Production Equipment
Continuous production equipment is used to reduce the number of manual interventions in the manufacturing process. Automation and continuous processing can minimize direct labor costs and reduce the influence of human variation on product quality. They may also improve process repeatability, throughput, and the ability to monitor key production parameters.
In CMS manufacturing, repeatability is especially important because small differences in carbonization temperature, activation conditions, binder distribution, shaping, drying, or post-treatment can influence adsorption kinetics and mechanical properties. A controlled continuous process can help maintain a narrower performance range from batch to batch.
Climate and Production-Environment Considerations
The company operates in northern China for production conditions where relatively low humidity and lower moisture content in the air are considered favorable for CMS manufacturing. Moisture control is important because water can interfere with pore development and complicate drying. A production environment with lower ambient humidity can reduce the burden on moisture-control systems and contribute to more consistent processing.
Environmental conditions must still be controlled through appropriate industrial equipment, monitoring, and storage practices. The choice of production location is one supporting factor, not a substitute for process management.
Research and Development Cooperation
Research cooperation with Jinan Shengquan Group and China University of Mining and Technology supports the study of carbon materials and CMS performance. Cooperation between an industrial manufacturer and research institutions can help connect laboratory-scale characterization with commercial process development.
Research may address pore-size distribution, adsorption kinetics, particle strength, carbon precursor selection, regeneration behavior, thermal stability, and performance in actual nitrogen generators. Continuous testing and product iteration are important because the best adsorbent for one generator design may not be the best choice for another.
Testing in an Actual Nitrogen Generator
The manufacturer states that CMS performance is tested in a nitrogen generator before the product leaves the factory. This is a valuable quality-control approach because laboratory adsorption data alone cannot describe every aspect of PSA operation. Actual generator testing can reveal whether the material provides stable purity, suitable production capacity, acceptable pressure drop, and resistance to pulverization under cyclic conditions.
Testing the product in equipment also helps connect material quality with customer expectations. The final result depends on the complete PSA cycle, not only on a single static adsorption measurement. Production-rate and purity data should therefore be interpreted together with the test conditions used by the manufacturer.
ISO 9001 Quality Management
An ISO 9001-certified quality-management system provides a framework for documented processes, traceability, corrective action, inspection, and continual improvement. Certification does not replace technical testing, but it supports a structured approach to managing raw materials, manufacturing operations, finished-product inspection, and customer requirements.
For industrial customers, quality documentation may include batch information, product specifications, packaging records, inspection results, and recommended operating conditions. Buyers should confirm the exact documentation available for their order and application.
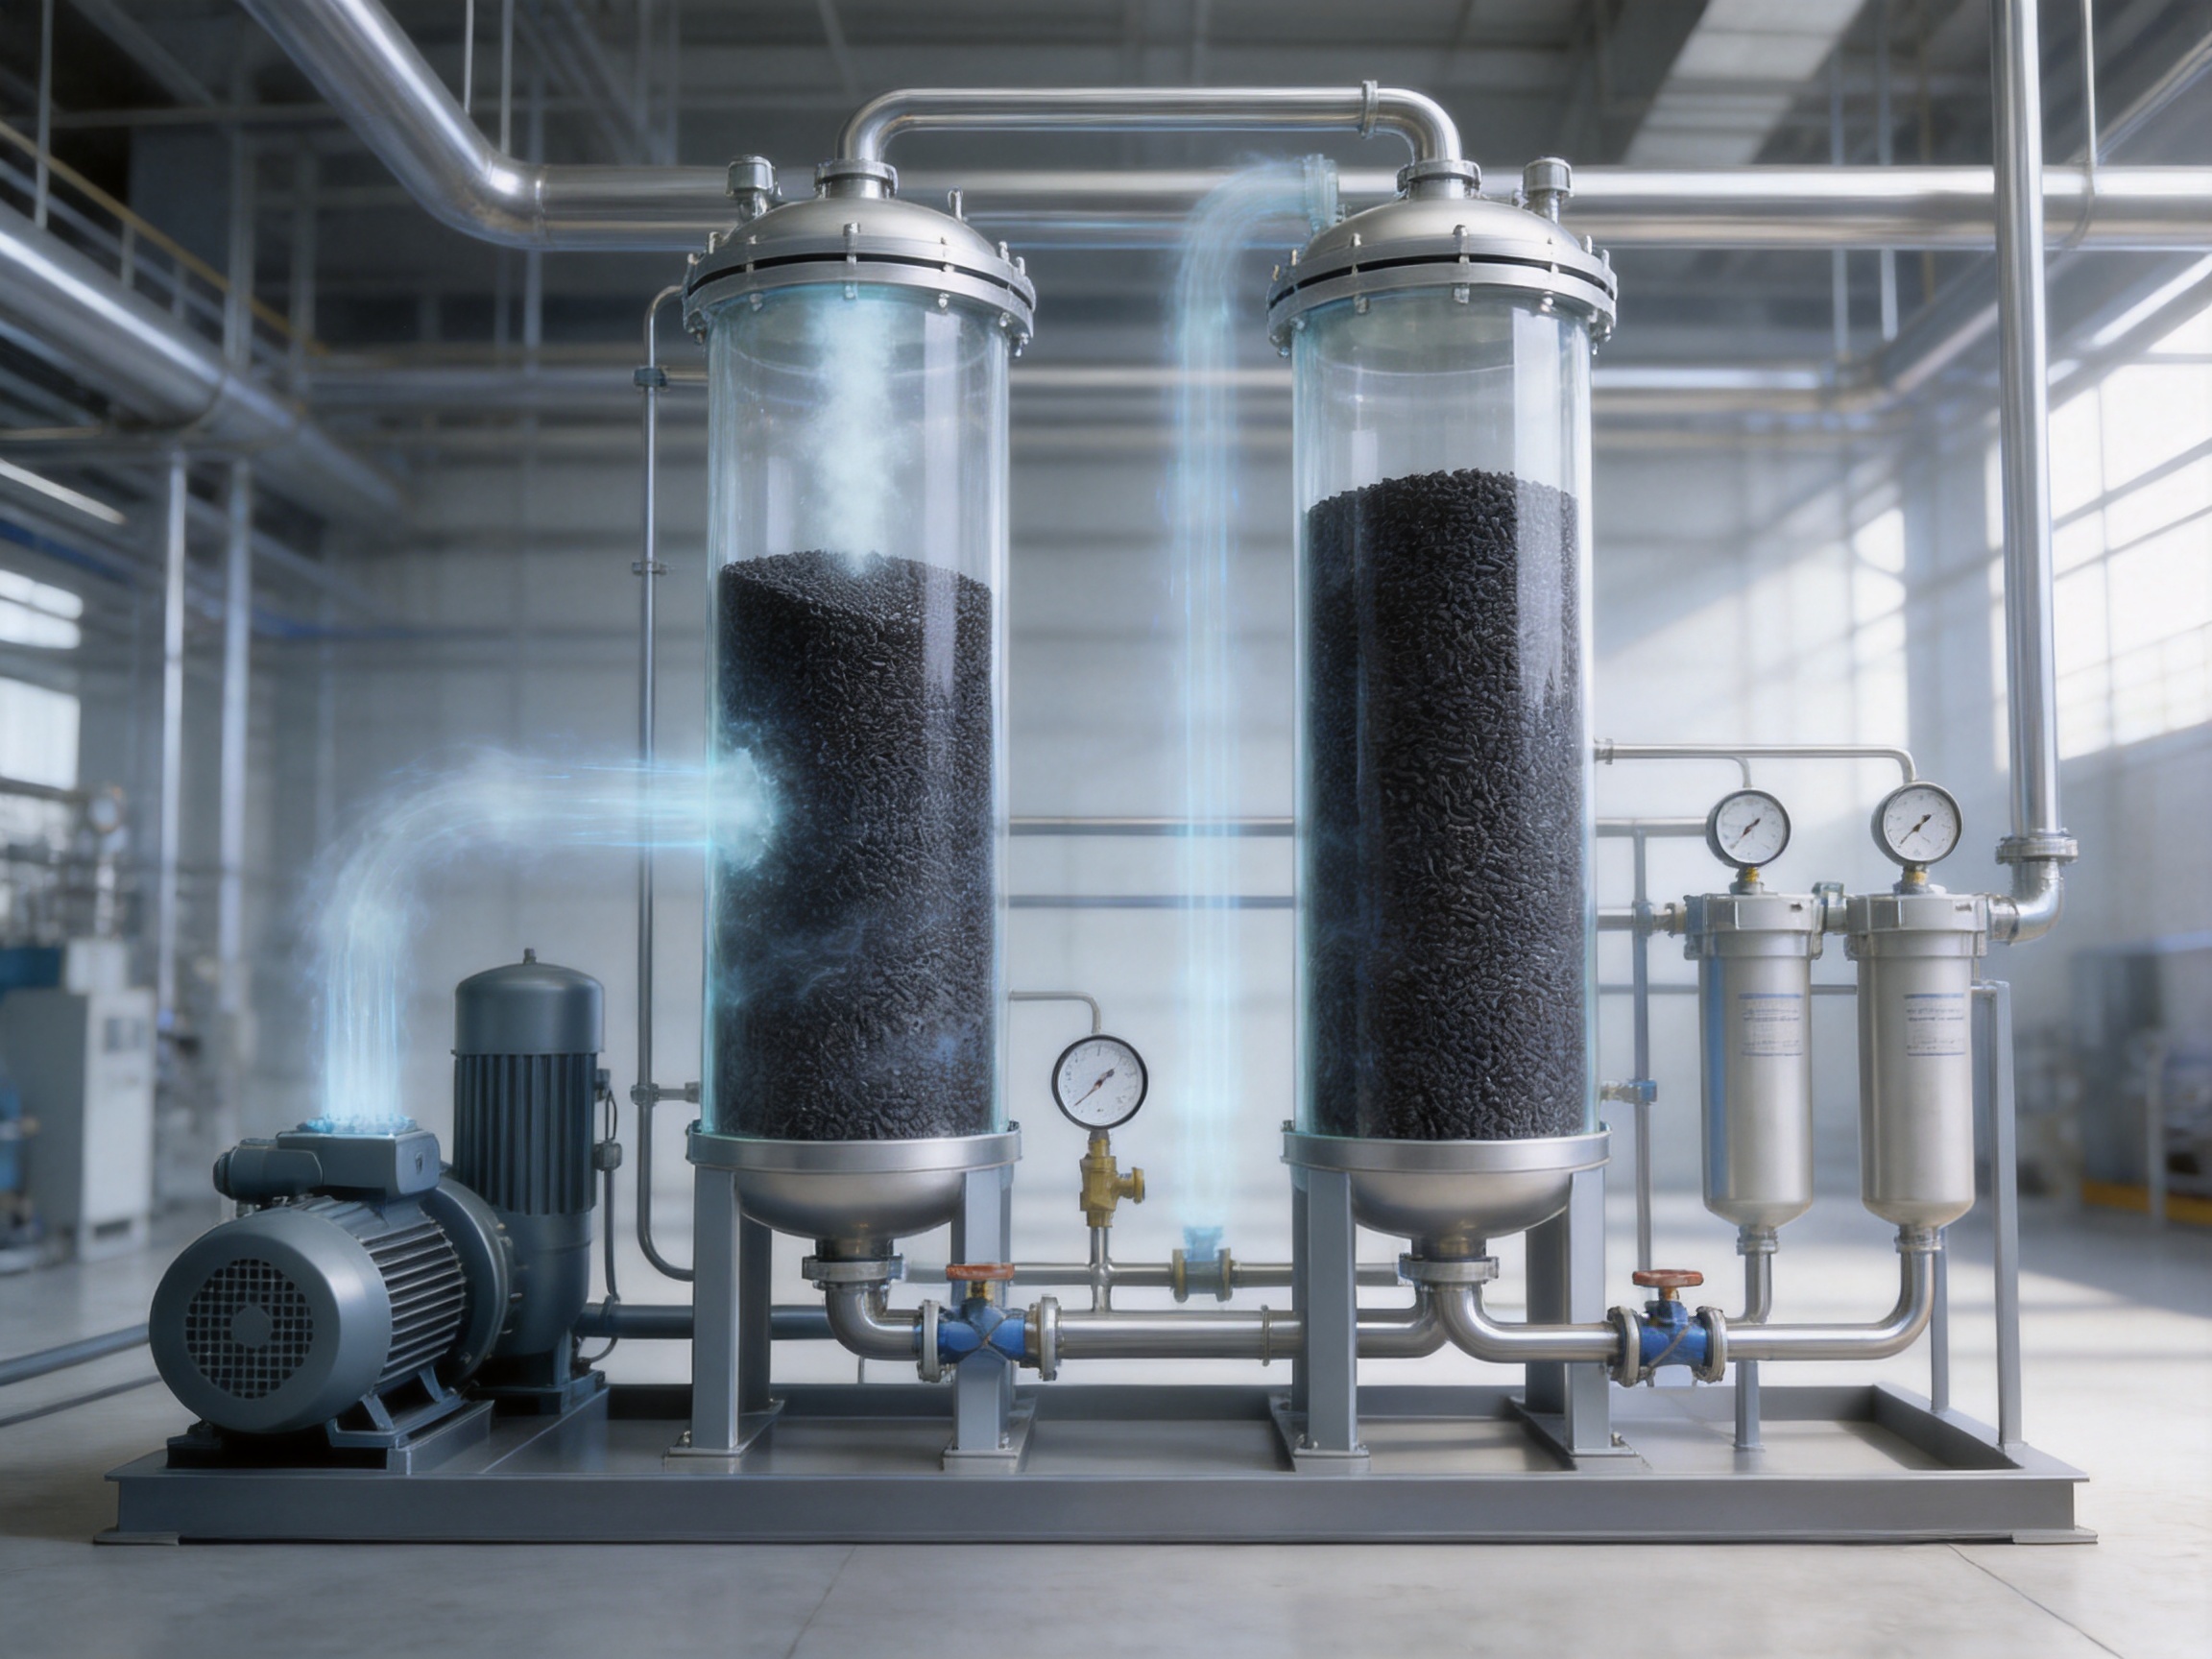
How CMS Works in a PSA Nitrogen Generator
Step 1: Compression and Cooling
Ambient air is drawn into an air compressor and compressed to the required feed pressure. Compression increases the temperature of the air and may introduce oil vapor, especially when an oil-lubricated compressor is used. The compressed air must therefore pass through an aftercooler or heat exchanger before entering the purification section.
Step 2: Air Purification
Air purification removes liquid water, oil aerosols, oil vapor, dust, and other contaminants. A typical system may include a water separator, coalescing filters, an oil-removal stage, a refrigerated or desiccant dryer, and additional filtration. The supplied operating guidance specifies a feed-air dew point below approximately minus 40°C and oil content below approximately 0.3 ppm, together with control of organic contaminants.
These limits should be confirmed against the final generator design and CMS supplier documentation. The more demanding the nitrogen purity and the longer the desired adsorbent life, the more important it is to maintain reliable pretreatment. CMS should not be expected to compensate for an undersized or poorly maintained air-treatment system.
Step 3: Pressurized Adsorption
Purified compressed air enters one adsorption tower filled with CMS. Under pressure, oxygen diffuses into the micropores more rapidly than nitrogen. The adsorbent retains oxygen and other preferentially adsorbed components while nitrogen passes through the tower and is collected as product gas.
As the adsorption front moves through the bed, the tower gradually approaches saturation. The generator controller must switch the tower at an appropriate point to prevent oxygen breakthrough. Cycle timing is selected according to the CMS grade, bed dimensions, pressure, temperature, feed-air quality, and required nitrogen purity.
Step 4: Pressure Equalization
When one adsorption tower completes its production cycle, some of the gas remaining in the tower can be transferred to another tower. This pressure-equalization step reduces the pressure difference between towers and can recover part of the gas energy within the system.
The supplied operating guidance recommends a general pressure-equalization time of approximately one to three seconds, although the correct setting depends on the equipment. Proper equalization can improve energy efficiency, reduce abrupt pressure changes, and reduce mechanical stress on the CMS. Poorly controlled equalization may contribute to particle movement, attrition, or unstable switching behavior.
Step 5: Depressurization and Regeneration
After adsorption, the saturated tower is depressurized. Reducing the pressure lowers the loading of oxygen and other adsorbed gases, allowing them to leave the CMS pores. In a pressure-swing process using atmospheric regeneration, the tower is usually regenerated toward atmospheric pressure. A small amount of product nitrogen may be used as purge gas, depending on the generator configuration.
The regenerated tower is then repressurized and prepared to receive compressed air again. By alternating the towers, the PSA system maintains a continuous product stream while each individual bed operates cyclically.
Recommended Operating Conditions
Feed-Air Dew Point and Oil Control
Water and oil are among the most serious threats to CMS performance. Moisture can occupy active micropores, lower oxygen adsorption, increase the risk of bed degradation, and cause corrosion or malfunction in associated equipment. Oil vapor can coat the carbon surface and permanently reduce access to the pore network.
The compressed-air system should include appropriately sized filtration and drying equipment. Filters must be replaced according to pressure drop, service hours, and contamination loading. Dryers should be monitored for dew point, and compressor maintenance should be performed to prevent abnormal oil carryover.
Adsorption Pressure
Higher adsorption pressure generally increases the amount of gas that can be adsorbed. However, excessive pressure also increases compressor energy consumption, equipment cost, and mechanical requirements. The supplied guidance recommends an adsorption pressure of approximately 0.6 to 0.8 MPa for a general atmospheric-regeneration process, while the product performance table is based on approximately 0.75 to 0.80 MPa.
The optimum pressure should be established through a complete energy and performance evaluation. A pressure that appears favorable from an adsorption perspective may not be economical when compressor efficiency, valve losses, and system pressure drop are included.
Operating Temperature
Because adsorption releases heat, the temperature inside the CMS bed can rise during the adsorption stage. As temperature increases, adsorption capacity generally decreases. Lower and more stable feed-air temperature is therefore beneficial for nitrogen production.
The supplied material recommends an ambient temperature at or below approximately 15°C for optimal nitrogen-generator performance. In practice, the acceptable temperature range depends on the generator design and local conditions. Aftercoolers, ventilation, insulation, and adequate equipment-room design can help manage thermal effects.
Pressure-Equalization Time
Pressure equalization should be optimized rather than selected arbitrarily. A short equalization period may fail to recover available gas energy, while an excessively long period may reduce production time or disturb the cycle balance. The recommended general range of one to three seconds is a starting point for engineering adjustment.
Purity and Product-Flow Balance
Users should define nitrogen quality according to the actual process requirement. Higher purity normally means lower product flow and higher air consumption. If the application only requires an oxygen-reduced atmosphere, operating at 99.0% or 99.5% nitrogen may offer a more favorable total cost than pursuing 99.999% purity.
The product gas should be analyzed using a properly calibrated oxygen or nitrogen analyzer. Purity should be evaluated after the generator reaches stable operation and under representative flow and pressure conditions. Temporary purity values during startup should not be used as the sole basis for product selection.
Applications Across Major Industries
Chemical Processing
Nitrogen is used to create inert atmospheres, reduce oxidation, purge vessels, and protect reactive chemicals. A PSA nitrogen generator can supply nitrogen near the point of use and adjust output according to production schedules. The required purity depends on the chemical reaction, solvent system, temperature, and safety assessment.
Oil and Gas
Oil and gas facilities use nitrogen for tank blanketing, pipeline purging, pressure testing, well-service operations, and equipment preparation. Reliable flow and stable pressure are often more important than the highest possible purity. CMS selection should be based on the required nitrogen quality, outdoor operating temperature, compressor conditions, and continuous-duty expectations.
Food Packaging
Nitrogen can displace oxygen in food packages and help reduce oxidation. It is used in modified-atmosphere packaging, snack-food packaging, beverage processing, and storage. Food-contact applications require appropriate system hygiene, gas-quality verification, and compliance with applicable regulations. The CMS is one component of the nitrogen system and does not by itself determine food-grade compliance.
Electronics and Semiconductor Manufacturing
Electronics production may require nitrogen for soldering, reflow processes, component storage, inert chambers, and moisture-sensitive manufacturing steps. These applications can require high purity and carefully controlled moisture and oxygen levels. CMS-280 or CMS-330 may be considered for high-capacity or high-purity systems, subject to testing and system qualification.
Pharmaceutical Production
Nitrogen is used for blanketing, transfer, packaging, drying, and protection from oxygen. Pharmaceutical applications require documented qualification, monitoring, validated operating procedures, and appropriate sanitation. The CMS generator must be integrated with purification and distribution equipment that meets the specific quality requirements of the process.
Metal Heat Treatment
Nitrogen is used as an inert or protective atmosphere in annealing, brazing, sintering, and other heat-treatment processes. The required gas quality depends on the metal, furnace design, temperature, and acceptable oxidation level. A stable nitrogen supply can improve process consistency and reduce reliance on delivered gas.
Cable, Transportation, and Storage
Nitrogen can protect cables, electrical components, tires, tanks, warehouses, and transport containers from oxidation or moisture. It may also be used for fire-risk reduction and inerting in enclosed spaces. Safety procedures must address oxygen-deficient atmospheres because nitrogen is colorless and odorless and can displace breathable air.
Choosing the Correct CMS Grade
The correct CMS grade should be selected through a structured assessment rather than by model number alone. The first requirement is the target nitrogen purity. The second is the required flow under normal and peak conditions. The third is the available compressed-air capacity and the acceptable air-to-nitrogen ratio.
Users should also evaluate operating pressure, feed-air temperature, dew point, oil carryover, daily operating hours, startup frequency, space limitations, maintenance capability, and expected adsorbent service life. For an existing generator, information about the original adsorbent, tower volume, particle size, cycle sequence, and historical purity will help determine compatibility.
A practical selection process may begin with CMS-240 for moderate requirements, CMS-260 for higher output, CMS-280 for a stronger performance margin, and CMS-330 for demanding high-capacity or high-purity systems. These are general positioning guidelines. A technical evaluation should confirm the choice through testing under the actual generator’s conditions.
Installation, Filling, and Maintenance
Adsorbent Filling
Before filling, the adsorption tower should be clean, dry, and free from oil, water, rust flakes, and foreign matter. Internal screens, support layers, distributors, and retaining components should be inspected. CMS particles should be handled carefully to minimize dropping distance and impact.
The bed should be filled uniformly and leveled according to the equipment manufacturer’s instructions. Uneven filling can cause channeling, localized velocity increases, poor gas distribution, and premature oxygen breakthrough. After filling, the tower should be sealed correctly and checked for leakage.
Startup
Startup should proceed gradually. The system should confirm that the air compressor, cooler, filters, dryer, valves, analyzer, and control system are operating correctly before the CMS towers are placed under full-cycle operation. Sudden pressurization can move particles and create unnecessary mechanical stress.
Routine Monitoring
Operators should monitor product nitrogen purity, product flow, feed pressure, regeneration pressure, pressure drop, temperature, dew point, oil carryover, valve timing, and compressor condition. A gradual decline in purity may indicate moisture contamination, oil contamination, adsorbent aging, valve leakage, incorrect cycle timing, or an undersized air-treatment system.
Increased pressure drop may indicate dust formation, bed compaction, blocked filters, or damaged internal screens. Unusual noise during switching may indicate excessive particle movement or valve malfunction. Early investigation can prevent a minor operating issue from developing into a complete adsorbent replacement event.
Storage and Transportation
Unused CMS should be kept sealed in moisture-resistant packaging. The material should be protected from rain, condensation, high humidity, oil vapor, and chemical contamination. Opened packages should not be left exposed for long periods. Storage areas should be clean, dry, and separated from materials that may release organic vapors.
Competitive Advantages of the Product and Manufacturer
The competitive position of this CMS product range is based on the combination of material performance, manufacturing integration, product testing, and technical development. Many suppliers can provide carbon adsorbents, but consistent PSA performance requires control of the complete material chain.
First, the product range offers several grades rather than a single general-purpose material. CMS-240, CMS-260, CMS-280, and CMS-330 provide choices for different purity and capacity targets. This helps users avoid over-specifying a high-cost grade when a lower grade is sufficient, while also providing higher-performance options for demanding systems.
Second, the manufacturer emphasizes dedicated carbon raw materials and cooperation with related supply companies. This can improve control over precursor quality and reduce dependence on inconsistent external sources. A stable raw material is important because carbon structure and micropore development begin with the precursor.
Third, continuous production equipment reduces manual variation and supports repeatable manufacturing. Consistency is particularly important for PSA adsorbents because the customer’s generator must perform through thousands of pressure cycles.
Fourth, the manufacturer tests CMS in an actual nitrogen generator before shipment. This provides a stronger connection between product quality and real PSA operation than relying only on general material specifications.
Fifth, research cooperation, patented carbon-material technology, an annual porous-carbon production capacity of approximately 4,000 tons, and planned expansion of a 3,000-ton porous-carbon project support long-term development. The company also reports 21 core patents and ISO 9001 certification, demonstrating an emphasis on technology ownership and structured quality management.
Finally, the company provides an integrated industrial chain that includes porous-carbon materials and nitrogen-equipment services. This can be useful for customers seeking not only an adsorbent but also technical communication concerning generator performance, operating parameters, and application matching.
Frequently Asked Questions
What is the main function of CMS in a nitrogen generator?
CMS selectively adsorbs oxygen from compressed air more rapidly than nitrogen. Nitrogen passes through the adsorption bed as product gas, while oxygen and other preferentially adsorbed components are removed during regeneration.
What is the difference between CMS-240, CMS-260, CMS-280, and CMS-330?
They are different CMS performance grades intended for different nitrogen-generation requirements. In the supplied typical data, higher-numbered grades generally provide higher nitrogen production rates at comparable purity levels. The final choice should be verified according to the generator design and operating conditions.
Can CMS produce 99.999% nitrogen?
Yes. The supplied performance data lists 99.999% nitrogen purity for all four grades. Actual purity depends on the generator design, air pretreatment, adsorption pressure, cycle timing, temperature, gas flow, and analyzer accuracy.
Does higher nitrogen purity reduce product flow?
Generally, yes. Producing higher-purity nitrogen requires more complete oxygen removal and usually increases compressed-air consumption per unit of nitrogen. Product flow commonly decreases as the purity target increases.
Why must compressed air be dried before entering the CMS tower?
Moisture can occupy micropores, reduce oxygen adsorption, promote contamination, and shorten adsorbent service life. Dry compressed air helps preserve separation performance and protects the CMS bed.
Why is oil removal important?
Oil vapor and aerosols can coat the carbon surface and block micropores. Oil contamination may cause a permanent loss of adsorption capacity and may also damage downstream valves, analyzers, and equipment.
What adsorption pressure is recommended?
The general guidance is approximately 0.6 to 0.8 MPa for atmospheric-regeneration operation, while the supplied performance data is based on approximately 0.75 to 0.80 MPa. The correct pressure must be confirmed through the complete generator design and energy evaluation.
How long can CMS last?
Service life depends on air quality, pressure cycling, temperature, bed design, particle handling, valve operation, and maintenance. Properly dried and oil-free air, stable cycling, and careful filling can help extend service life. No fixed lifetime should be assumed without reviewing the operating conditions.
Can CMS be used in an existing nitrogen generator?
It may be possible, but compatibility should be checked. Important factors include tower size, bed volume, particle size, distributor design, operating pressure, cycle timing, regeneration method, and the performance of the existing air-treatment equipment. A technical review is recommended before replacement.
How should CMS be stored?
CMS should remain sealed in moisture-resistant packaging and be kept in a dry, clean environment away from oil vapor, water, condensation, and organic contamination. Opened material should be used promptly or resealed properly.
What information should a buyer provide when requesting a quotation?
The buyer should provide the required nitrogen flow, purity, outlet pressure, operating hours, feed-air pressure, ambient temperature, compressor type, dew point, oil content, generator model, tower dimensions, and intended application. This information helps the supplier recommend the appropriate CMS grade and quantity.
Are the listed production rates guaranteed for every generator?
No. The listed values are typical reference data. Actual results vary according to equipment design, test conditions, air pretreatment, pressure cycle, temperature, and measurement methods. Performance should be confirmed through application-specific testing.
Conclusion
Carbon molecular sieve is the core separation material in PSA nitrogen generators, and its quality has a direct influence on purity, capacity, air consumption, stability, and service life. CMS-240, CMS-260, CMS-280, and CMS-330 provide a graded product range for applications requiring different balances of nitrogen purity, flow, and operating cost.
The key technical advantages include controlled micropore structure, selective oxygen adsorption, strong adsorption capacity, flexible purity adjustment, and suitability for continuous PSA operation. The product range is further supported by dedicated raw materials, specialized porous-carbon technology, continuous production equipment, research cooperation, ISO 9001 quality management, and testing in nitrogen-generating equipment before shipment.
For the best result, CMS selection should be integrated with correct air pretreatment, suitable adsorption pressure, controlled temperature, optimized pressure equalization, careful filling, and routine performance monitoring. When the material and the generator are properly matched, carbon molecular sieve can provide an economical and dependable source of nitrogen for a wide variety of industrial processes.
References
1. Manufacturer-provided technical information for CMS-240, CMS-260, CMS-280, and CMS-330 carbon molecular sieve.
2. Manufacturer-provided guidance on PSA nitrogen-generator operating conditions, compressed-air pretreatment, pressure equalization, and temperature control.
3. ISO 9001 quality-management principles for manufacturing and process control.
4. General technical literature on adsorption kinetics and pressure swing adsorption air separation.
5. General engineering references on compressed-air drying, oil removal, filtration, and gas-generation system maintenance.
6. General industrial guidance for nitrogen use in chemical processing, food packaging, electronics, pharmaceuticals, metal treatment, oil and gas, and storage applications.
Product: Carbon Molecular Sieve (CMS)
 E-mail
anhuilisa@126.com
 Phone
+86 18603224420
 Address
No. 26 Kunshan Road, Xuanzhou Economic Development Zone, Liqiao Town, Xuanzhou District, Xuancheng City, Anhui Province, P.R.China
Copyright Anhui Zhuoxu New Material Technology Co., Ltd. All rights reserved.
 Carbon Molecular Sieve Manufacturer Carbon Molecular Sieve Supplier